DIN EN 1090-2 EXC3
Certified welding contractor for load-bearing steel structures – qualified up to Execution Class EXC3.
DVS ZERT · Zertifizierungsstelle des DVS download as PDFLoad-bearing and technically demanding welded assemblies up to 50 t – manufactured as a certified welding contractor to DIN EN 1090-2 EXC3 in Lorch.
Certified welding contractor to EXC3, EN ISO 3834-2 and DIN EN ISO 9001:2015.
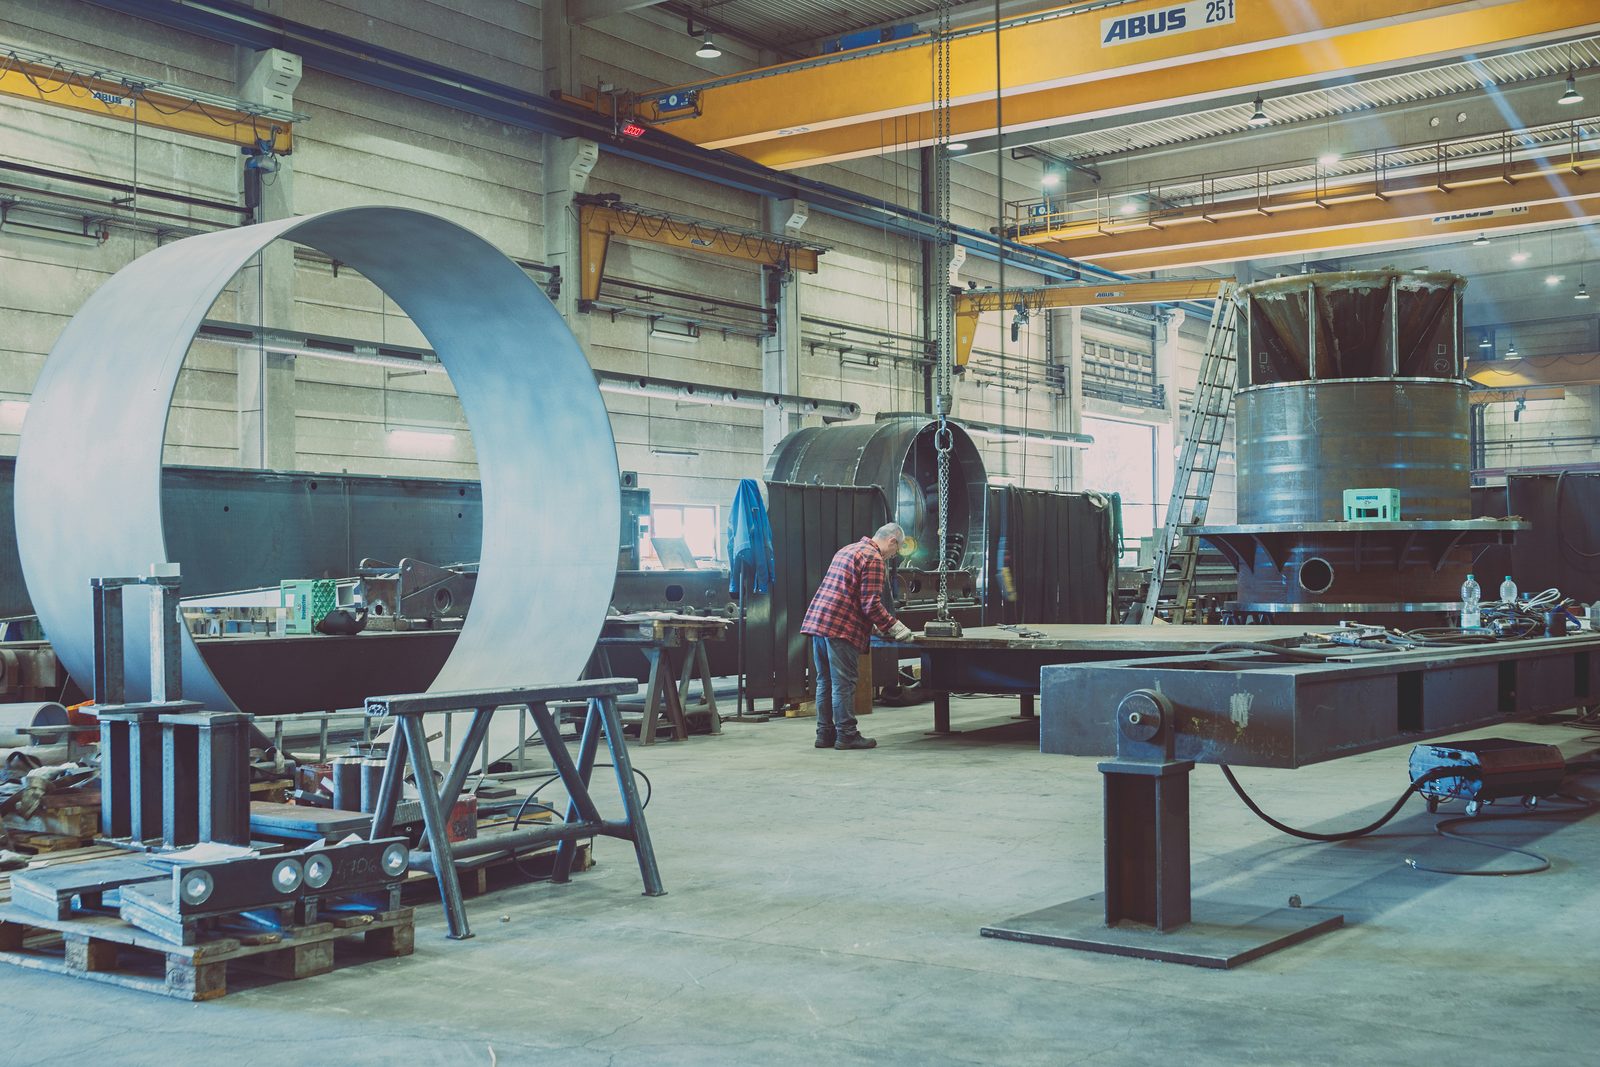
2×25 t crane system for safe handling of heavy welded assemblies.
Three welding processes selected by component requirement and required seam quality.
Steel, fine-grain structural steel, Hardox and stainless – exclusively certified materials.
VT, PT and MT to DIN EN ISO 9712 in-house, UT on a project basis via our cooperation partner.
CNC machining, shot blasting, painting and assembly within the same facility.
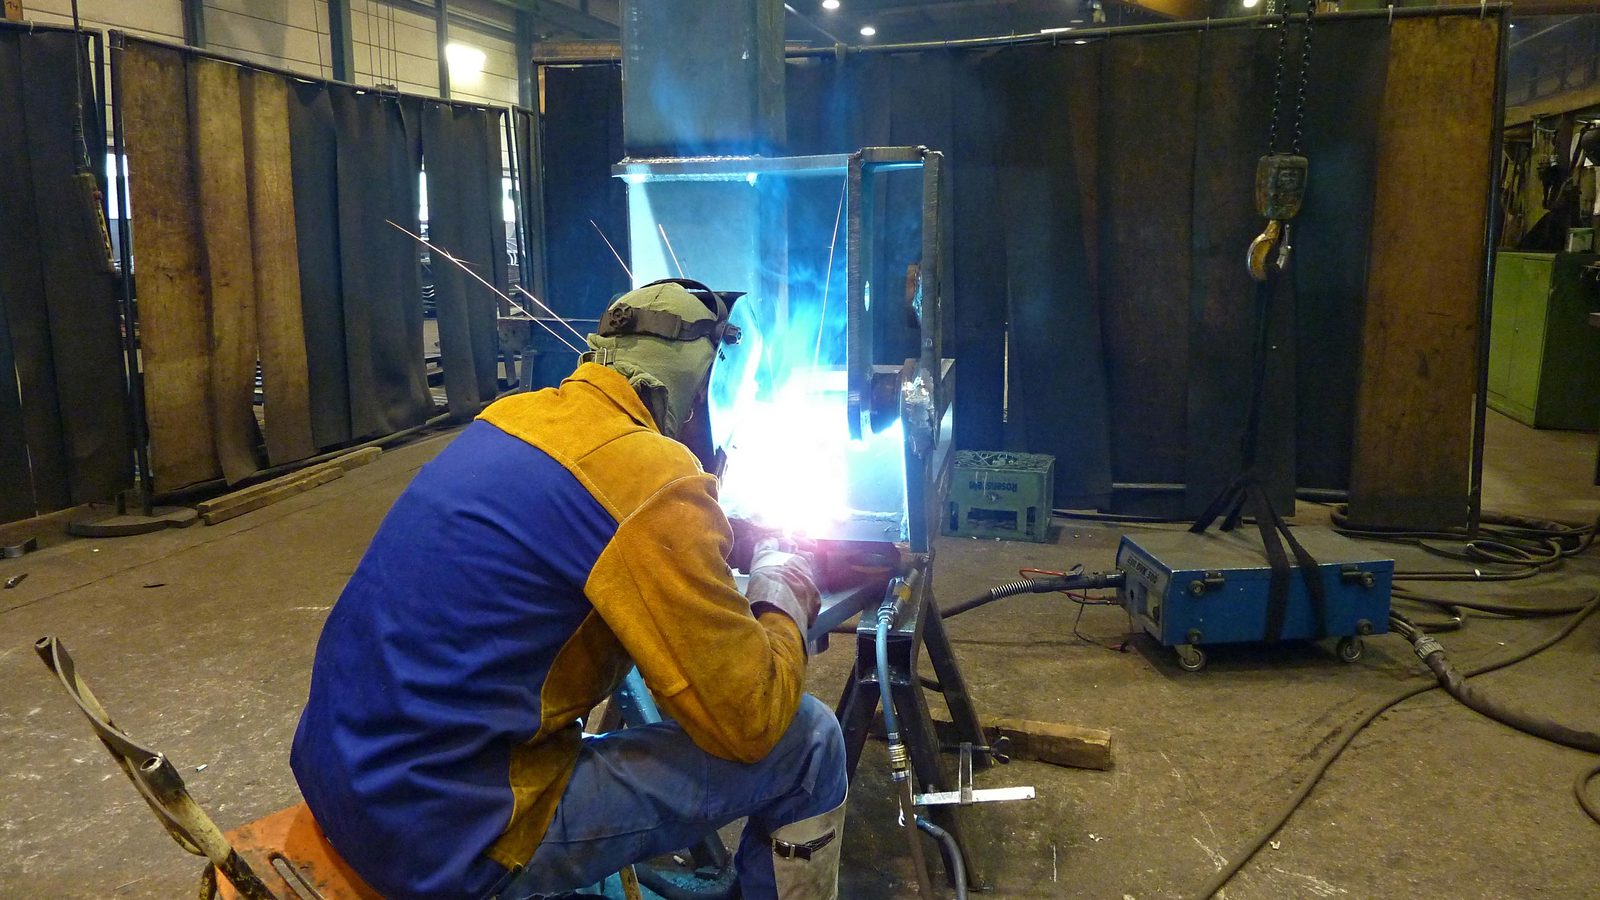
MAG for the structure, TIG for quality-critical seams, SAW for deep weld volume – combinable within a single component.
VT, PT and MT to DIN EN ISO 9712 in-house, Level 2 – testing happens where the welding happens.
Welding procedure specifications (WPS) and procedure qualification records (WPQR) to DIN EN 1090-2 are in place; project-specific records such as 3.1 inspection certificates, dimensional reports and NDT test reports are documented with the assembly.
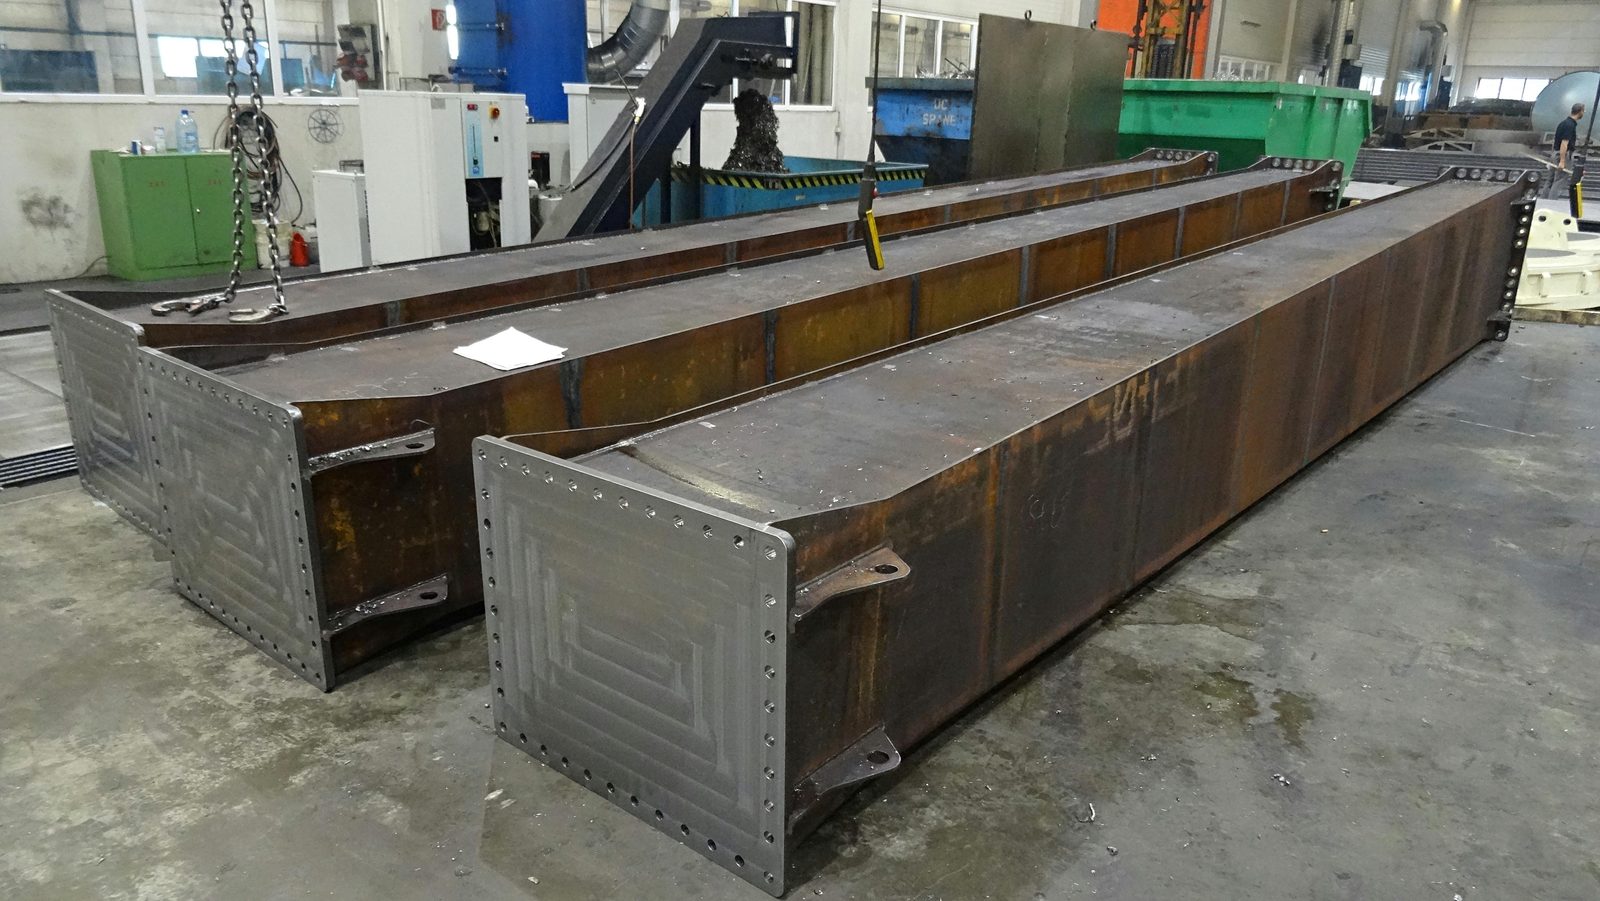
Welded assemblies at Bock are fabricated steel structures produced to customer drawings or specifications – from straightforward components to heavy, multi-part assemblies with close tolerances, high strength requirements or demanding material properties.
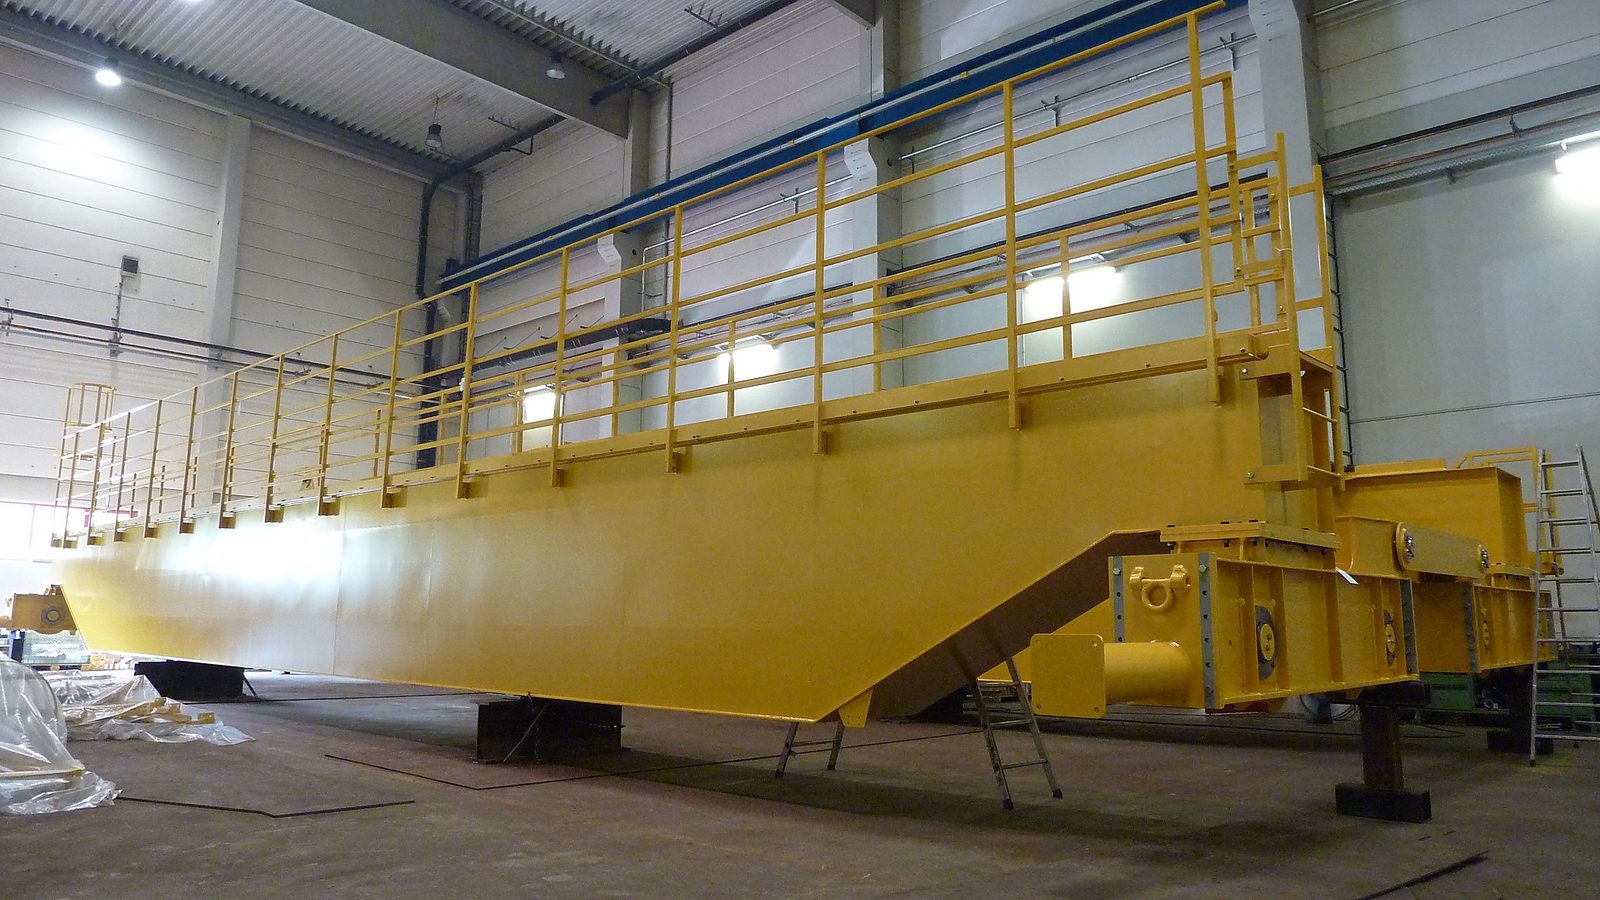
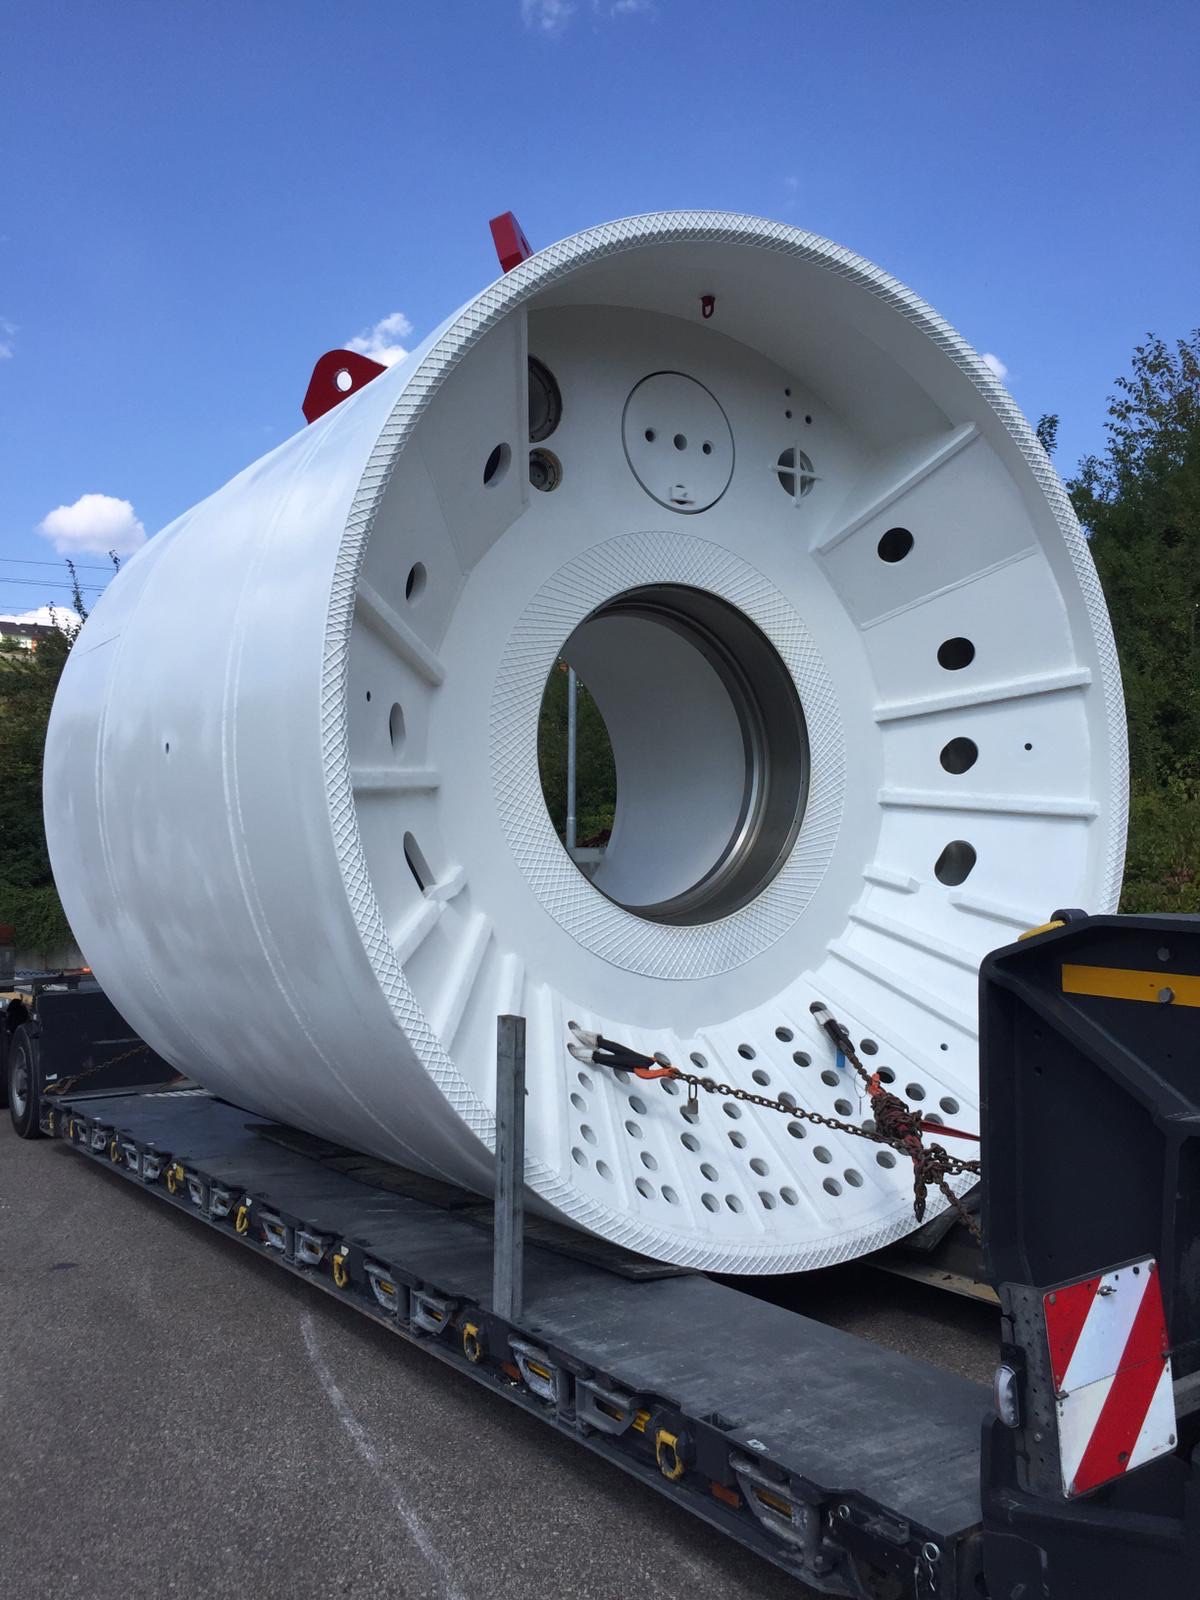
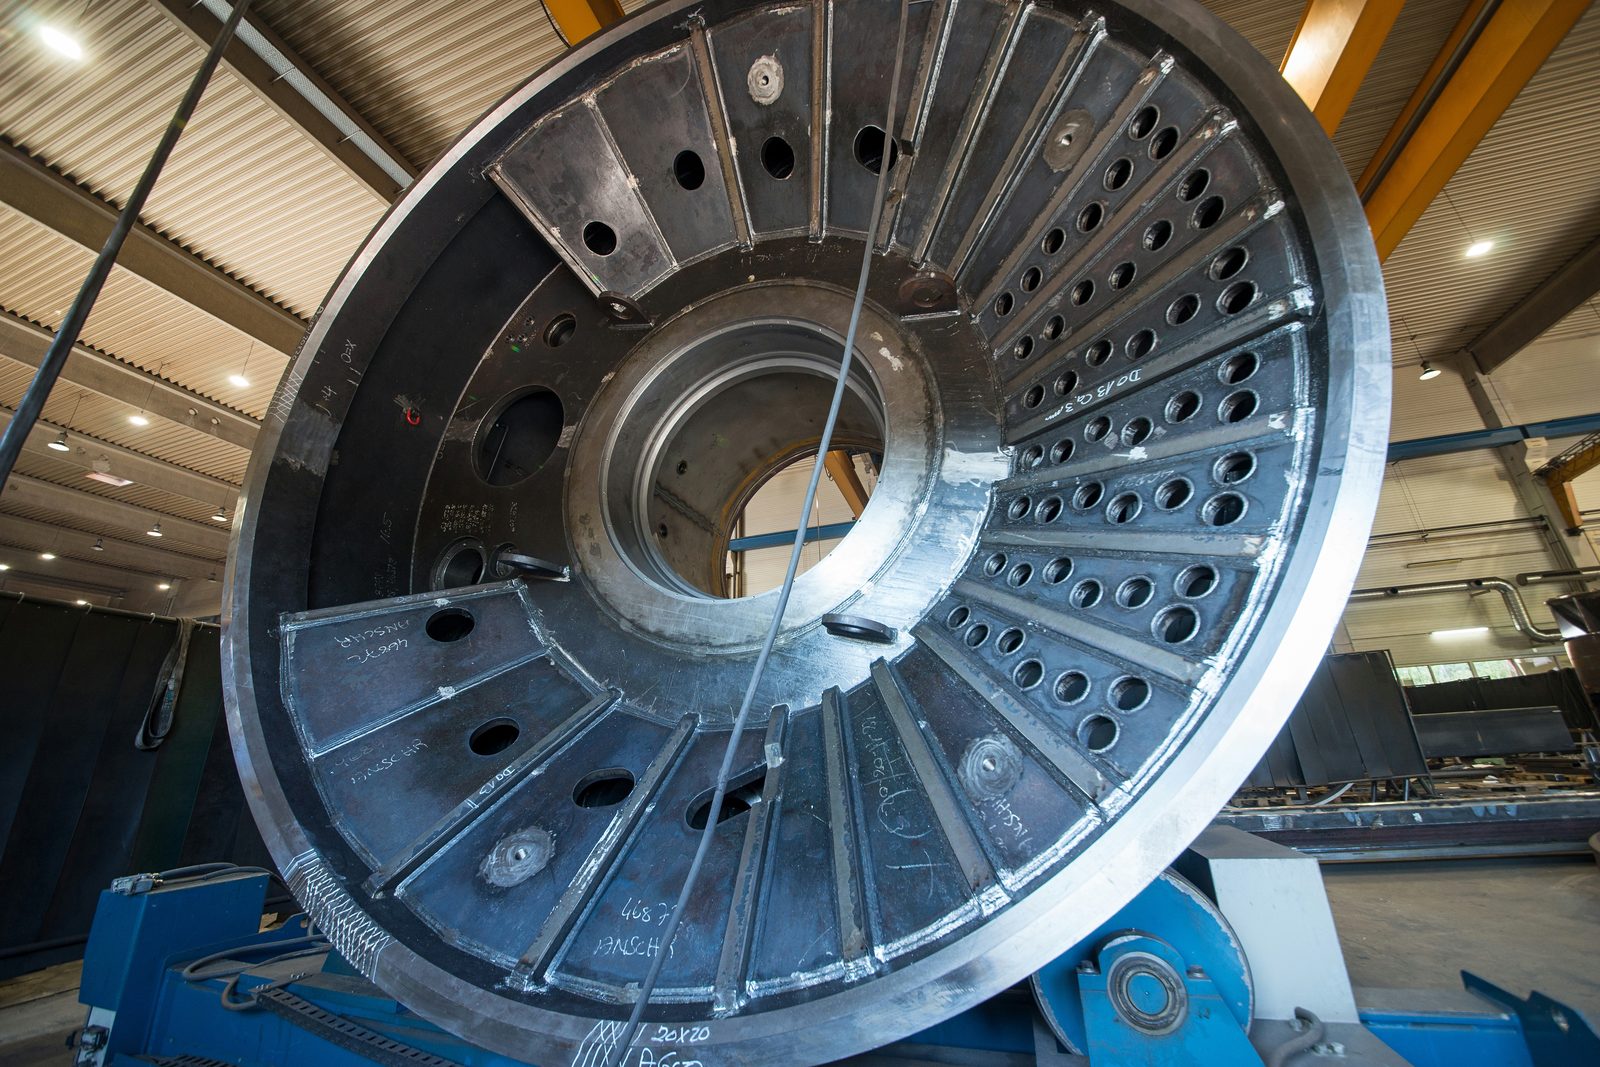
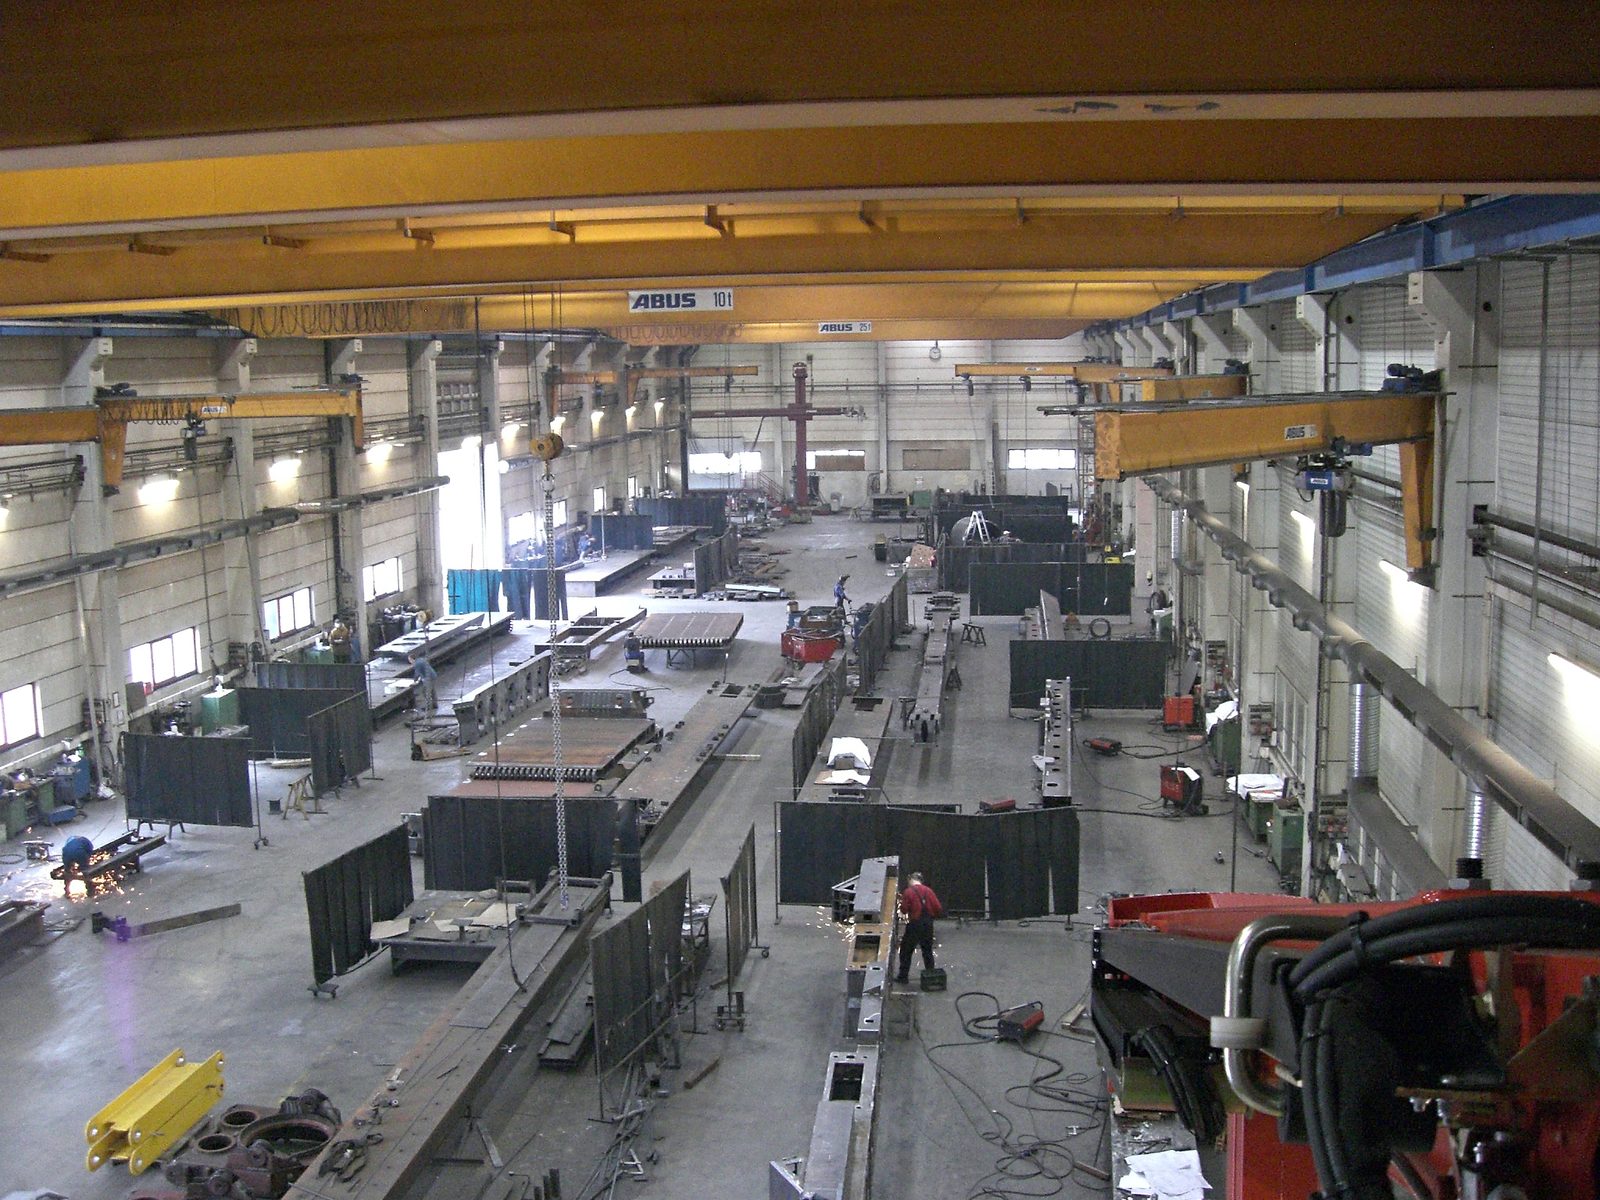
The production facility is equipped for heavy parts up to 50 t. The combination of multiple welding processes and broad material expertise allows structurally complex assemblies to be manufactured reliably to your specifications.
Where required, CNC machining, shot blasting, painting and assembly operations can be integrated into the project workflow.
As a certified welding company in the Ostalbkreis, we take on contract welding and load-bearing welded assemblies to EN 1090 for customers in the Stuttgart region, the Remstal and throughout southern Germany.

Depending on component geometry, material and seam requirements, Bock applies different welding processes:
Process selection is based on the requirements of your component. Where necessary, multiple welding processes may be combined within a single assembly.

The welding operation at Bock is extensively equipped for heavy and large-format assemblies:
This way, welds are made in the optimum position — economically, repeatably and in the inspected quality of a certified specialist welding company.

Bock uses predominantly European quality steels with traceable origin for all welded assemblies. Materials are selected according to drawing and requirements:
Material quality and origin are documented through material certificates where required by project or customer specifications. Components can extend up to 50 t unit weight; specific limits for special materials or unusual dimensions are agreed on a project basis.

Bock Maschinenbau is a certified welding contractor to DIN EN 1090-2 EXC3 and EN ISO 3834-2. Complemented by a certified quality management system to DIN EN ISO 9001:2015, these standards form a binding quality framework for the fabrication of welded assemblies: welding process qualifications, inspection requirements and documentation obligations are an integral part of production. Current certificates are available as PDF for clients with verification requirements.
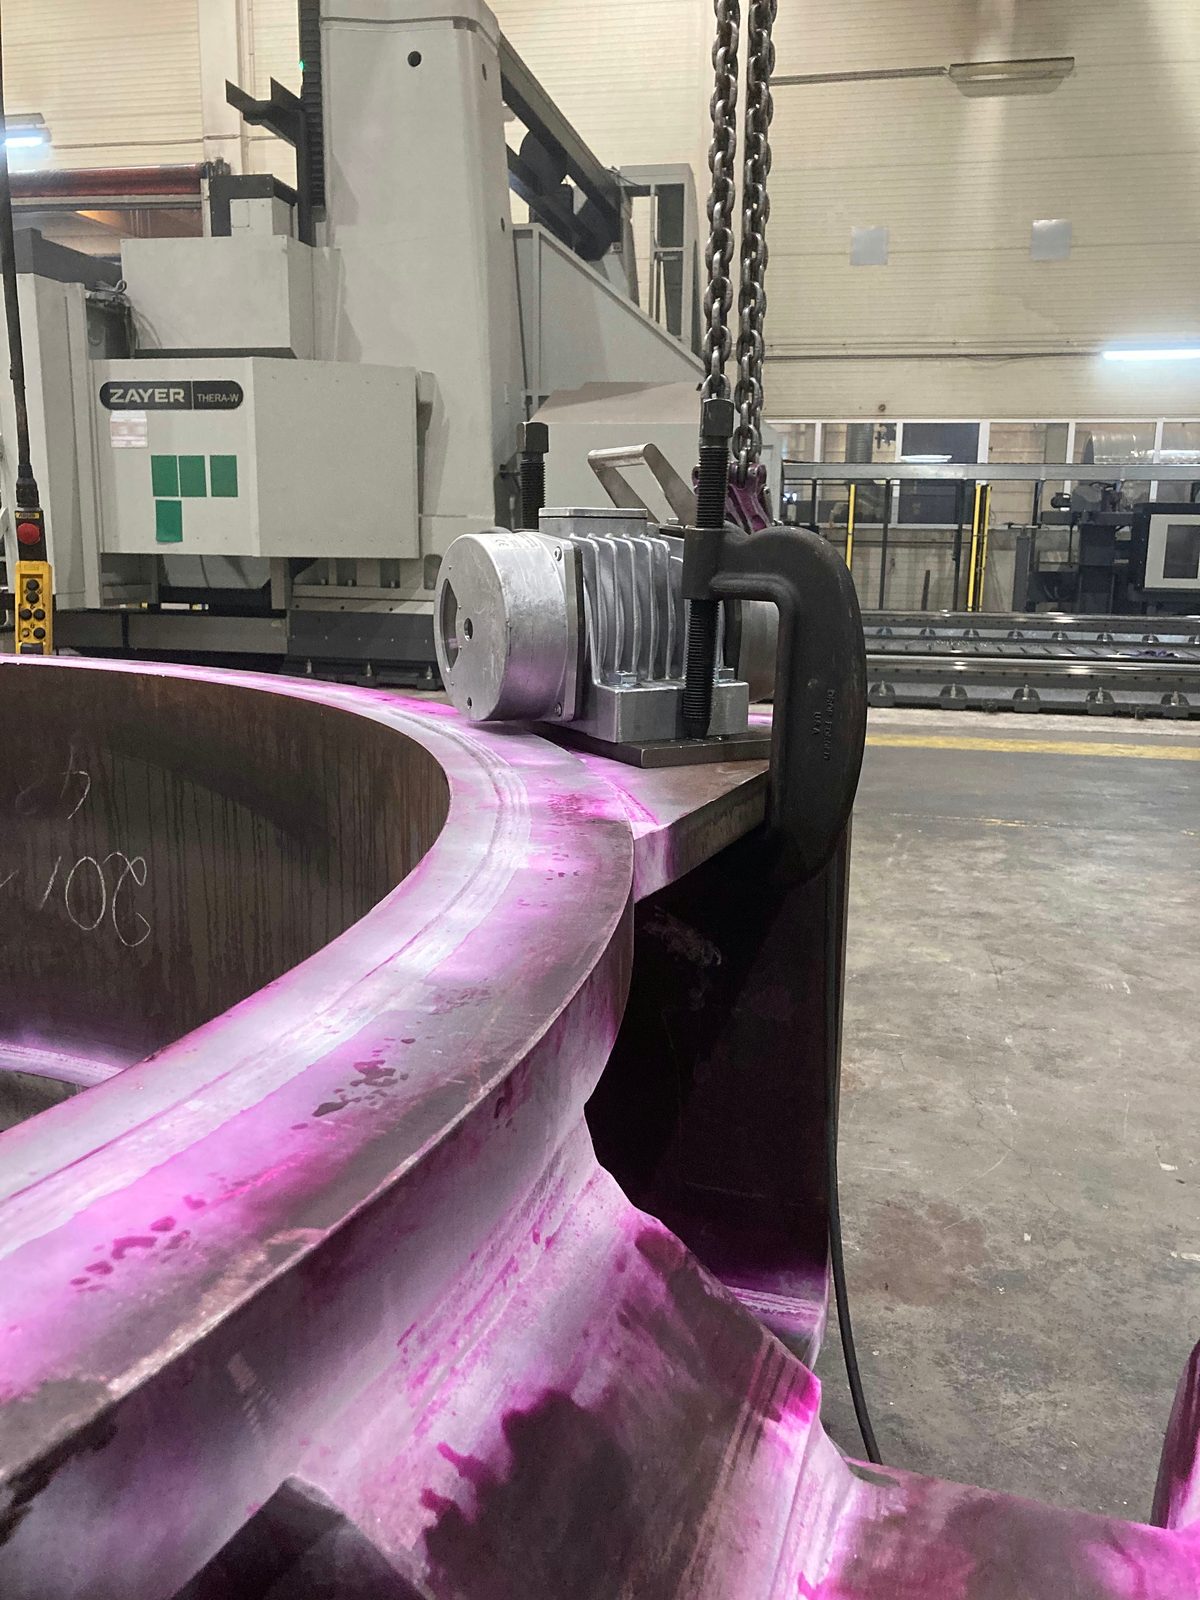
For welded assemblies, quality depends not only on the finished weld but also on traceable verification of the required standard. Welding operations are therefore accompanied by appropriate quality assurance measures. Depending on component, material, weld requirements and customer specifications, visual inspection and non-destructive testing (NDT) methods may be applied.
This covers surface indications, cracks, near-surface irregularities and internal irregularities in suitable components and weld joints.
Inspection and documentation requirements are agreed on a project basis according to drawing, normative requirements and customer specifications – ensuring that quality assurance is tailored to the individual assembly rather than applied as a blanket measure.

Welded assemblies frequently require further production steps. The following operations can be integrated into the project workflow as required:
Welded assemblies can therefore be not only welded but also machined, surface-prepared, coated or pre-assembled within the same production facility – subject to agreement and project requirements.

Welded assemblies from Bock are produced for technically demanding applications where material quality, certification, joining sequence and weld geometry are critical:
If, on the other hand, the number of joints is not the focus, but rather the size of the individual component and its handling, the production of heavy welded structures provides the appropriate framework.

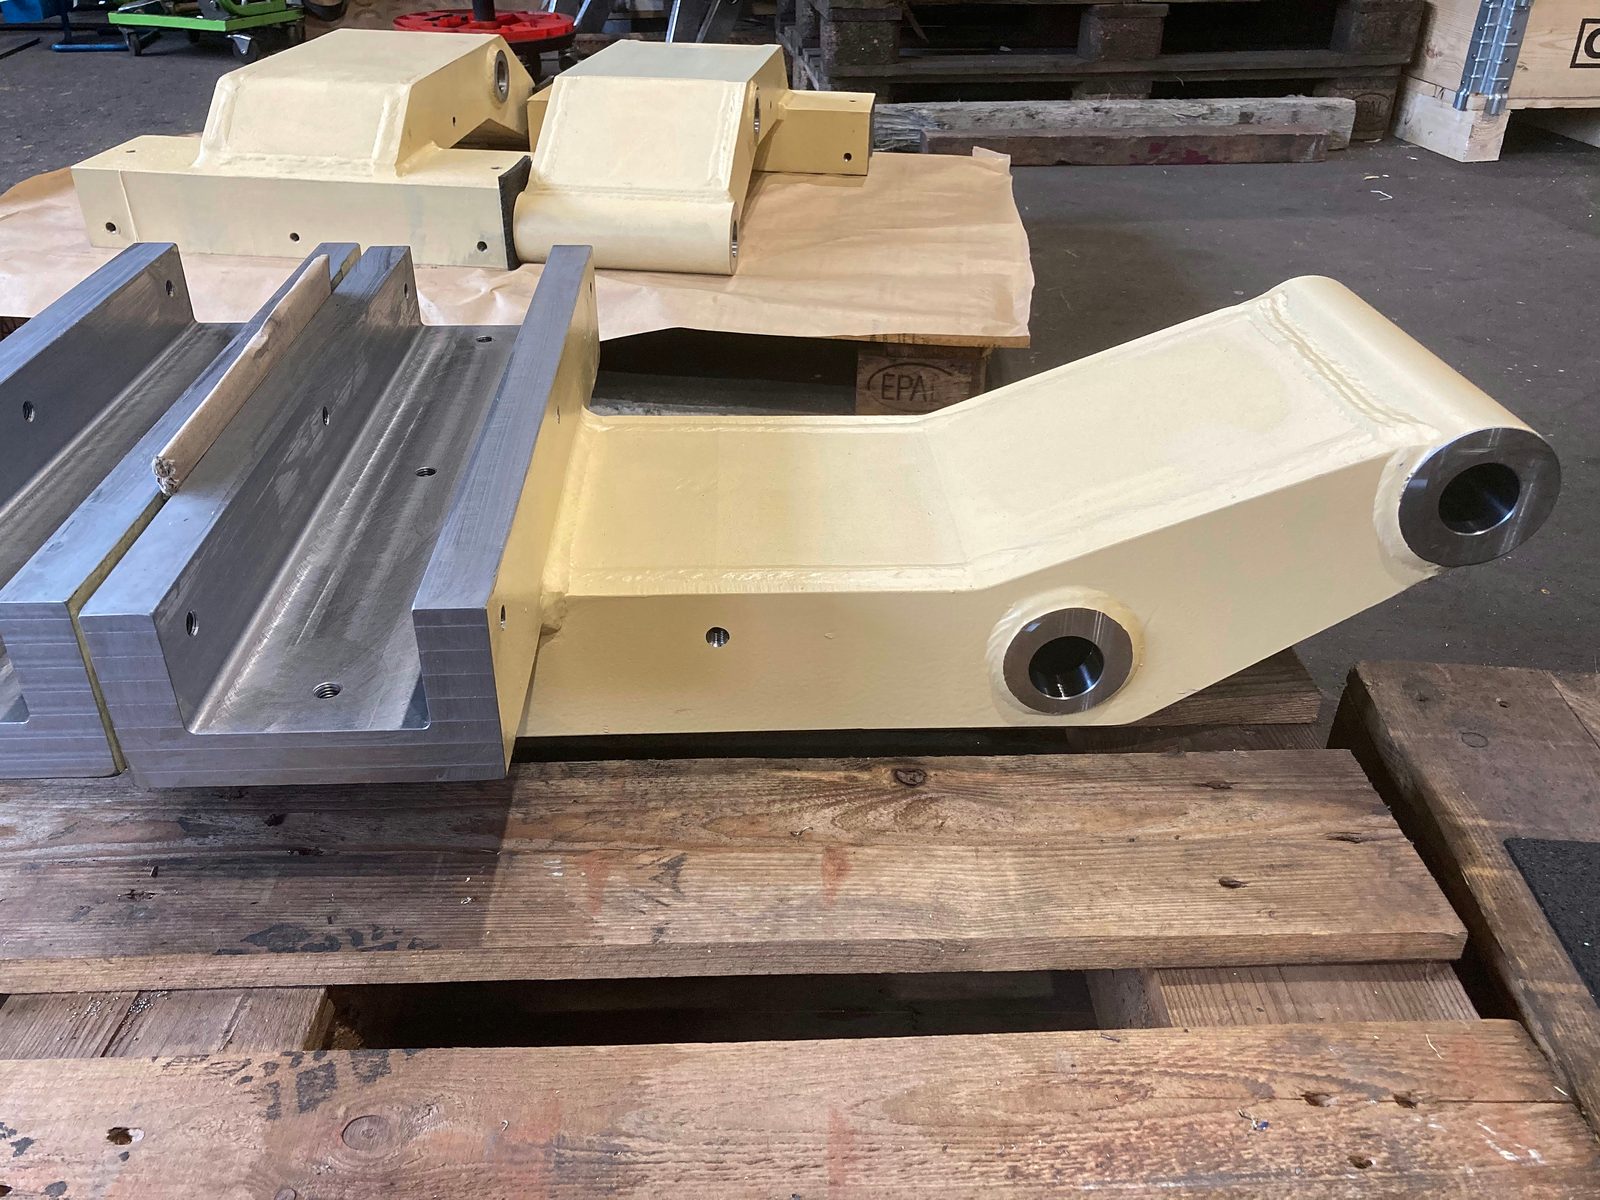
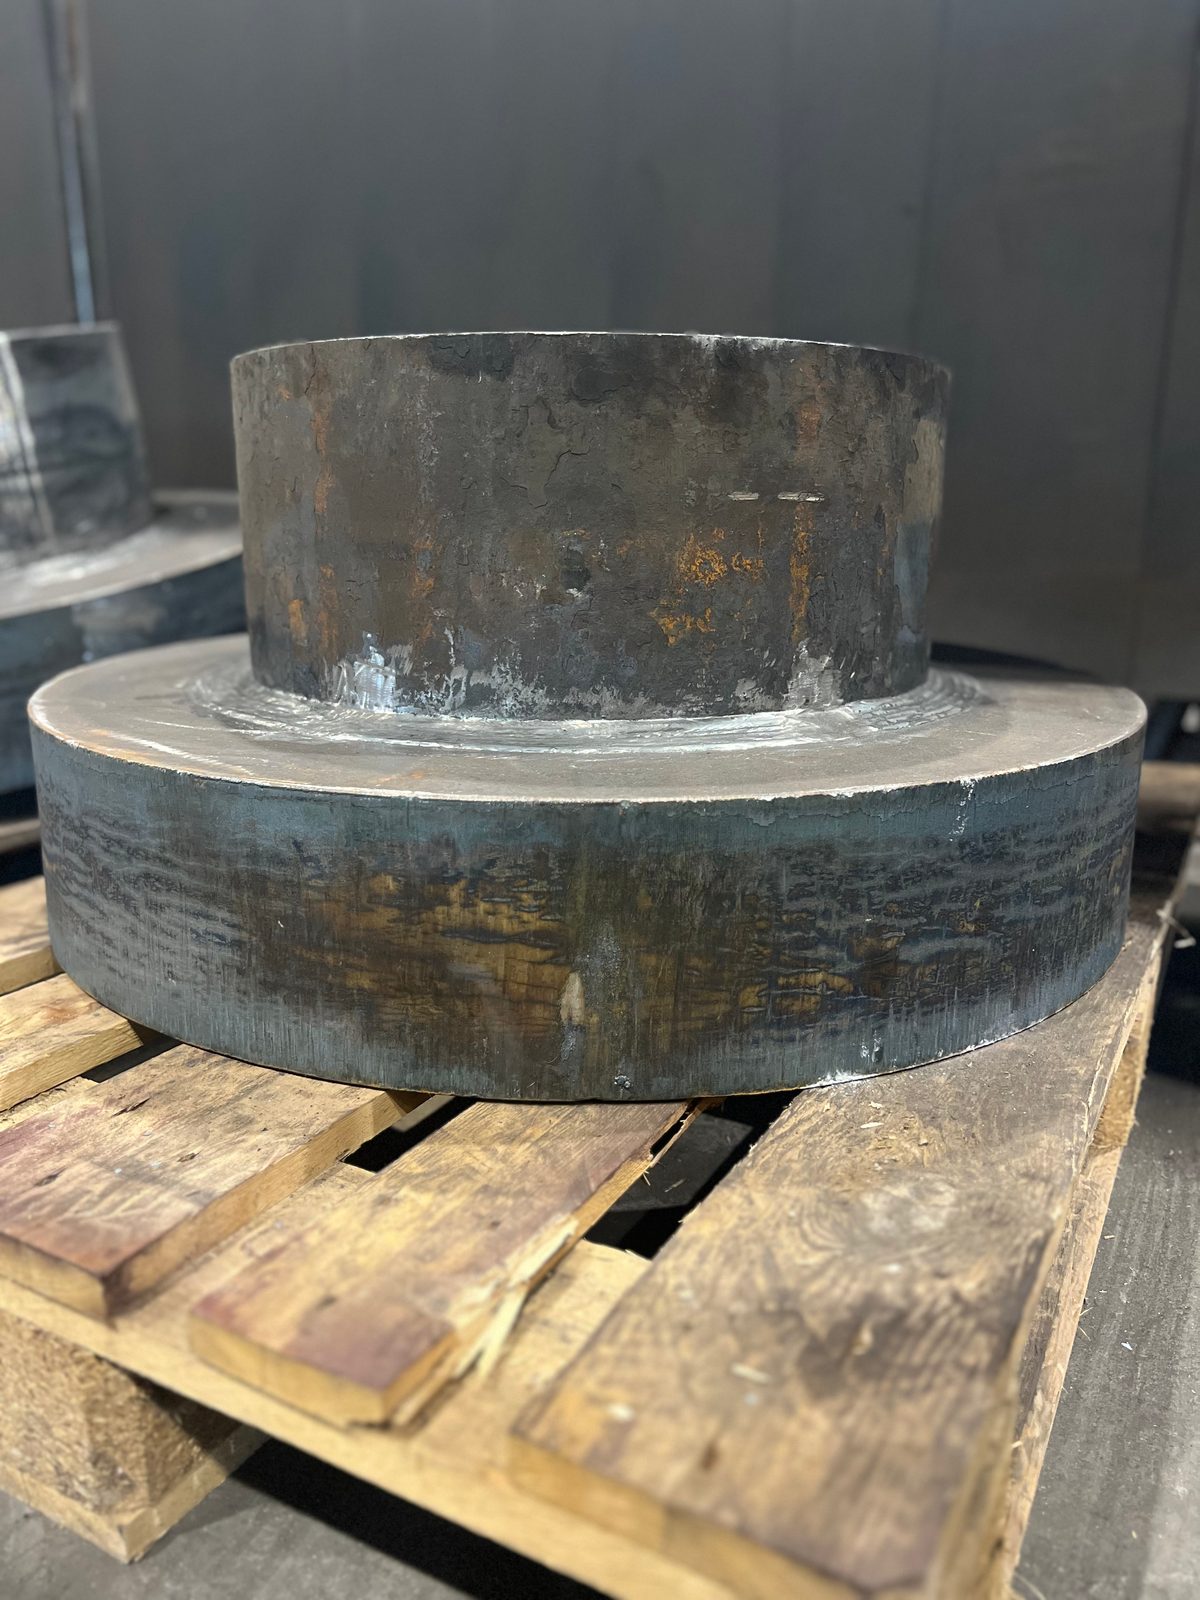
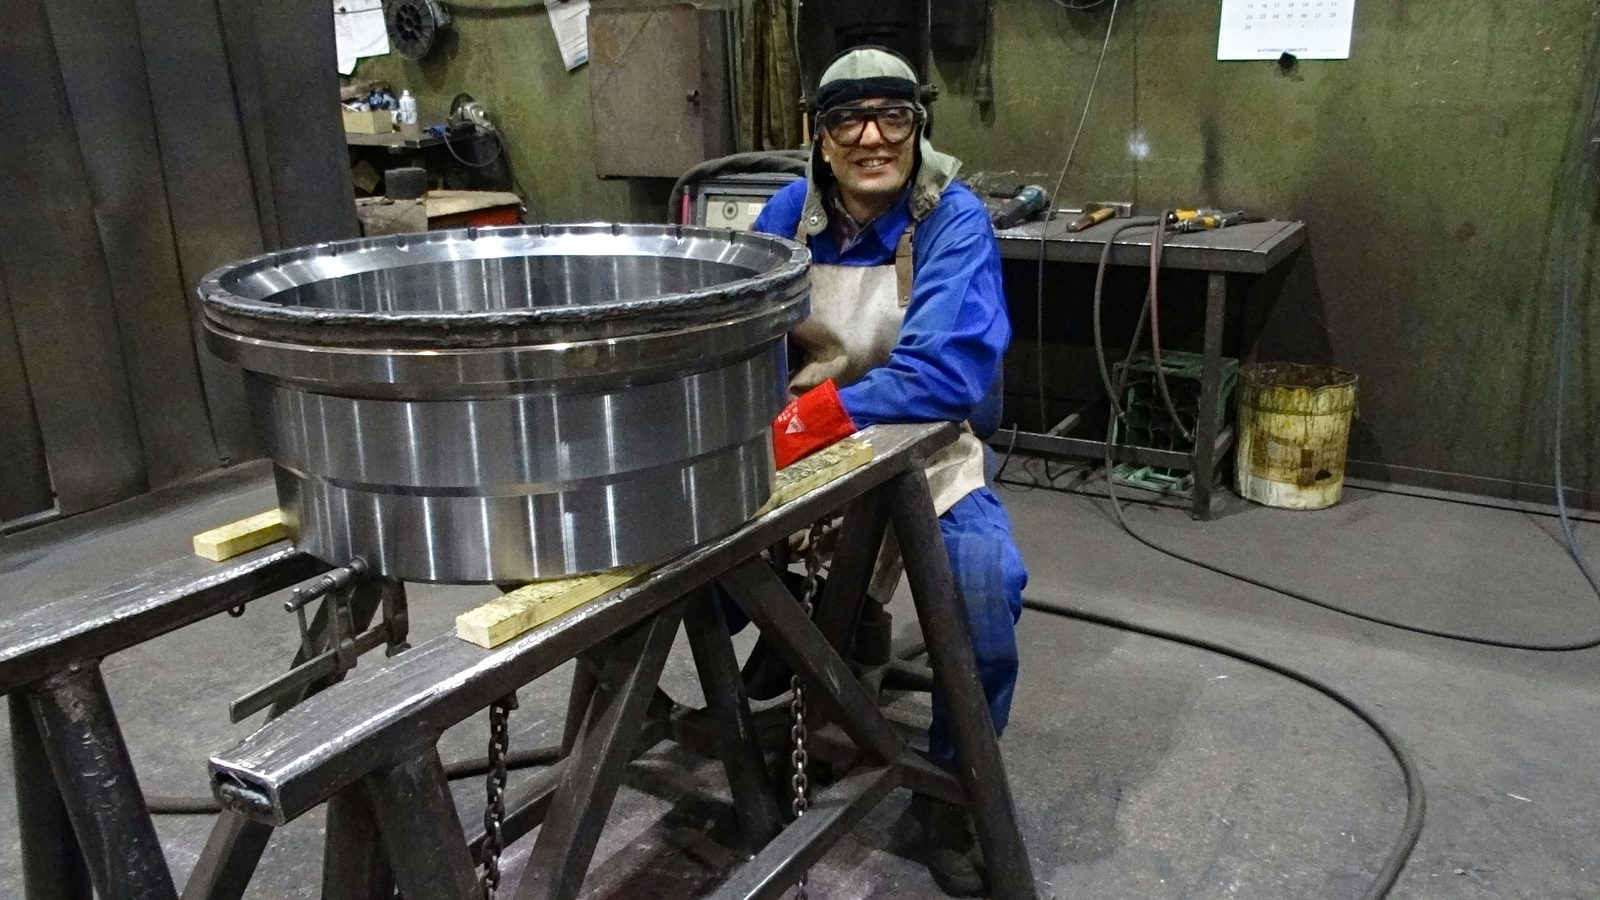
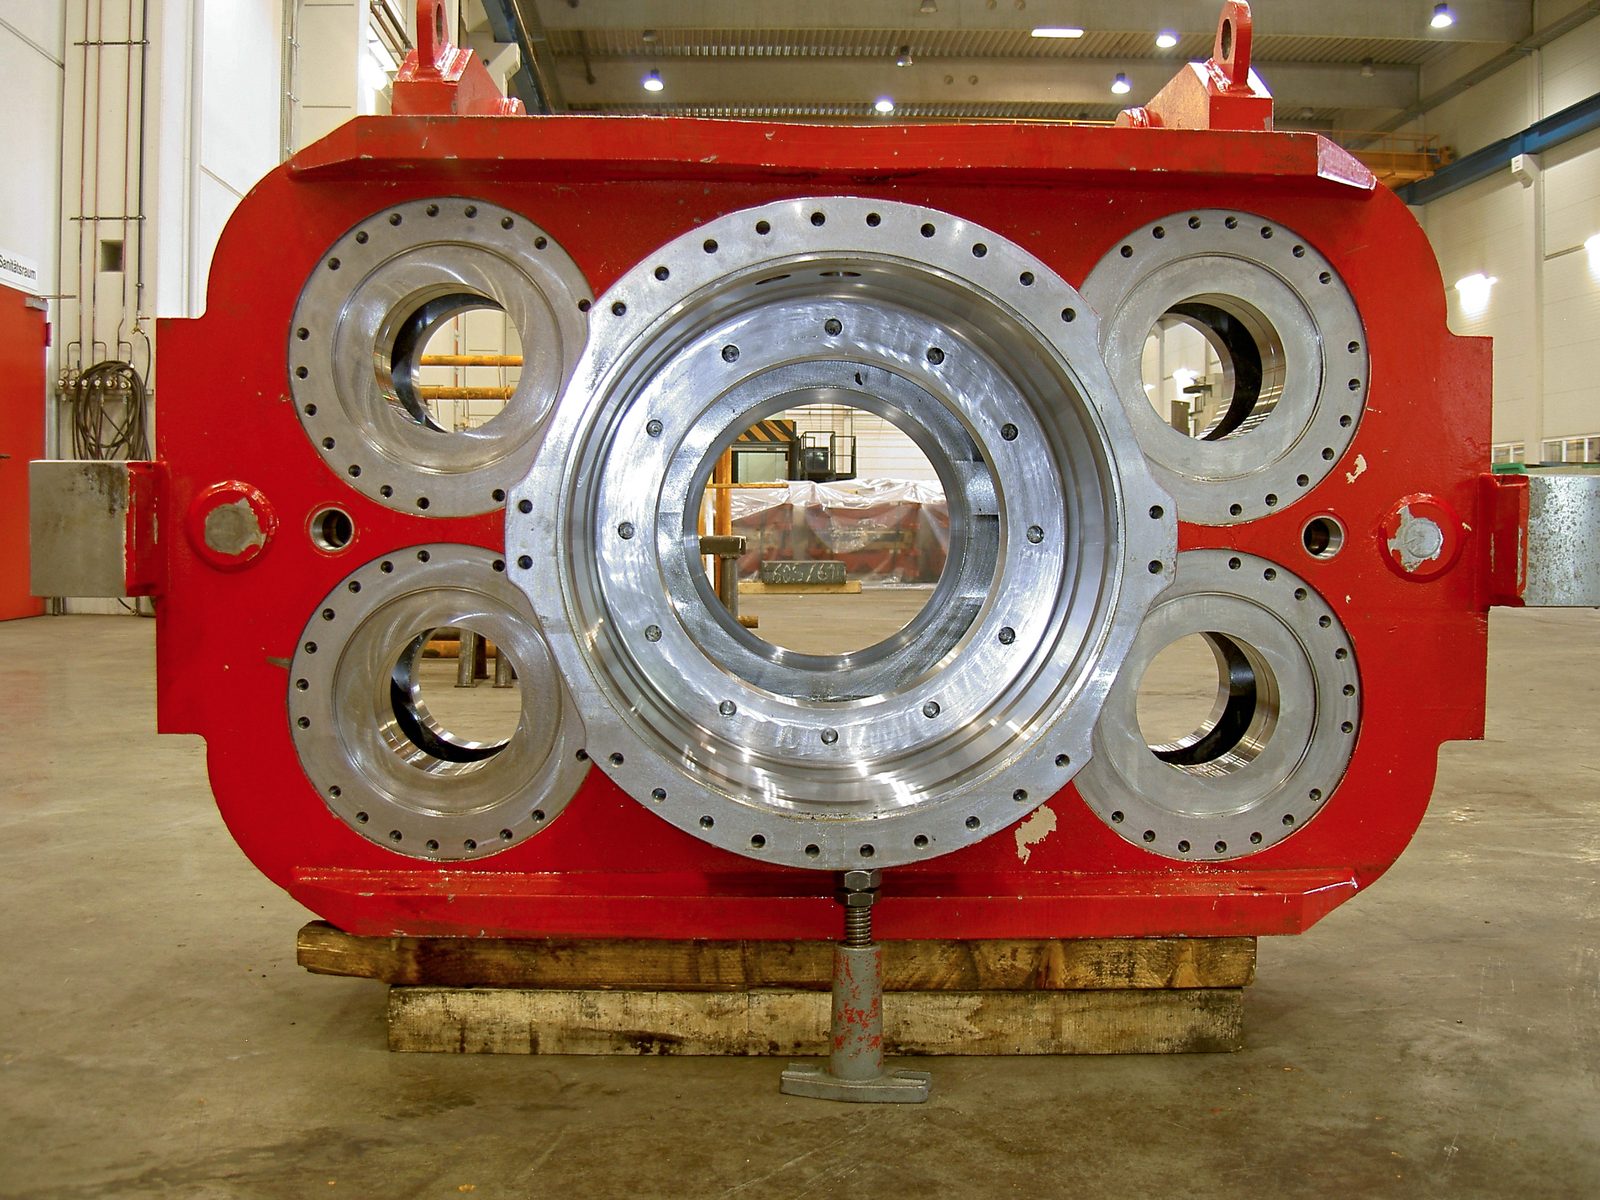
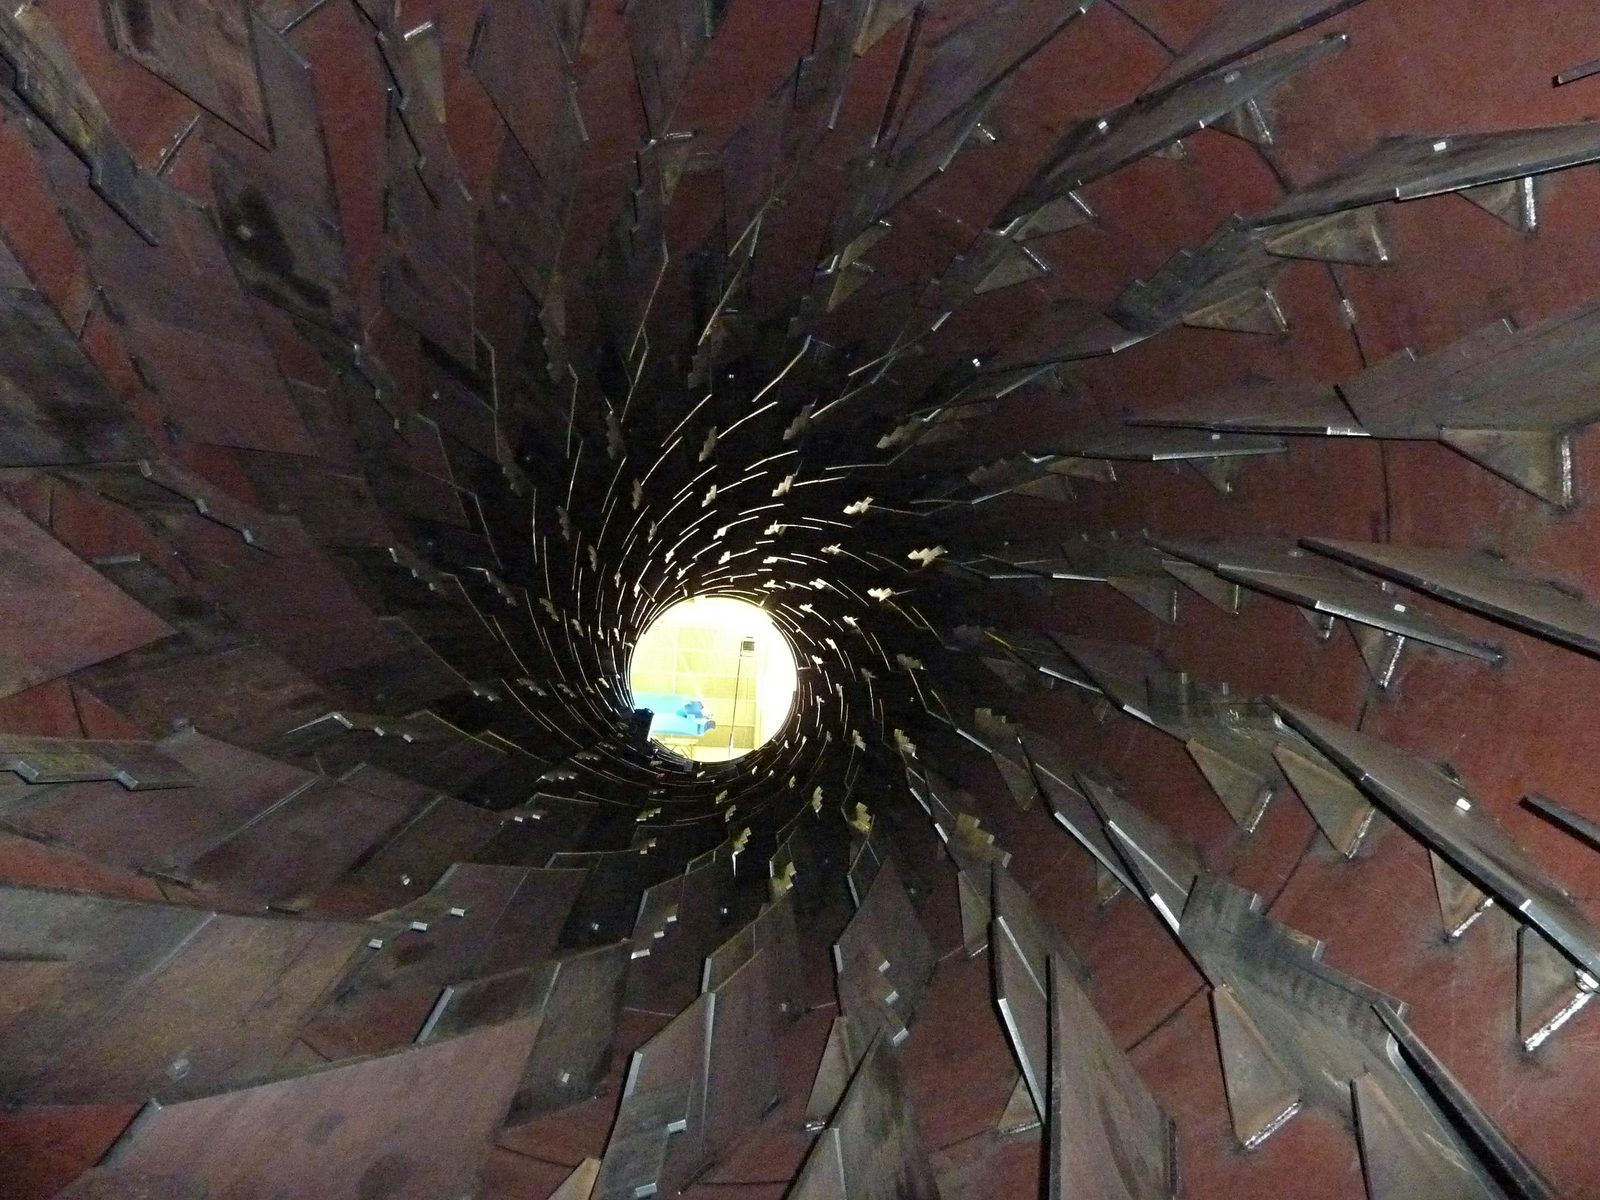
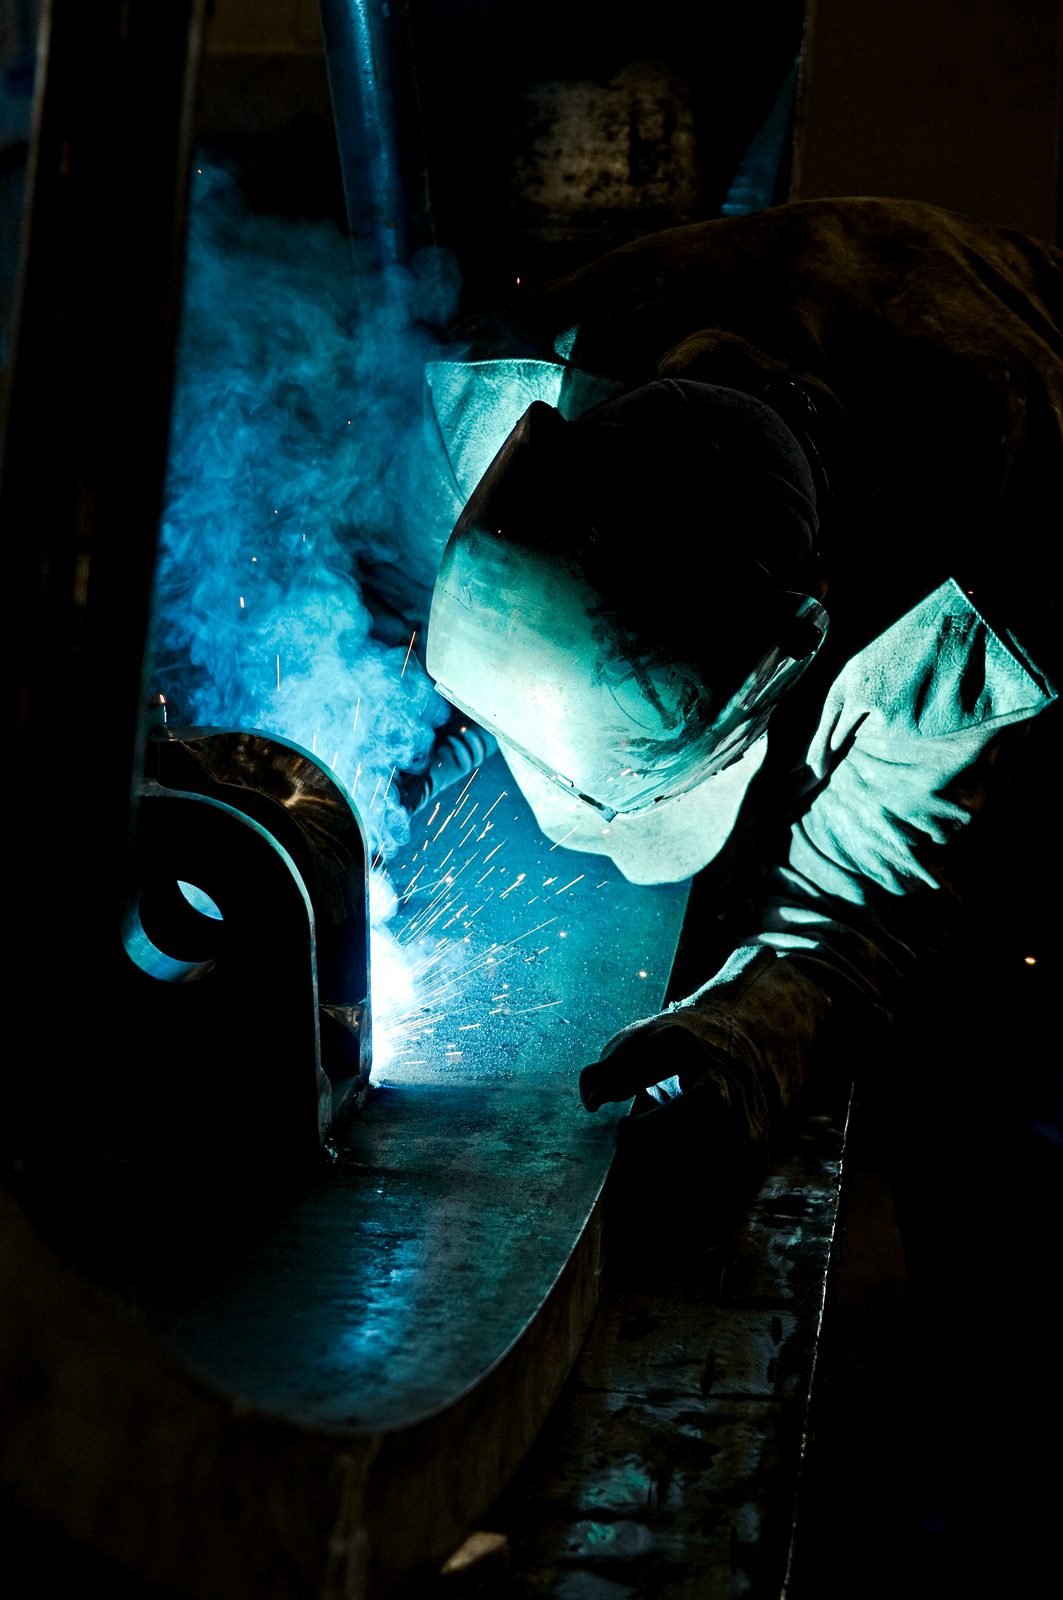
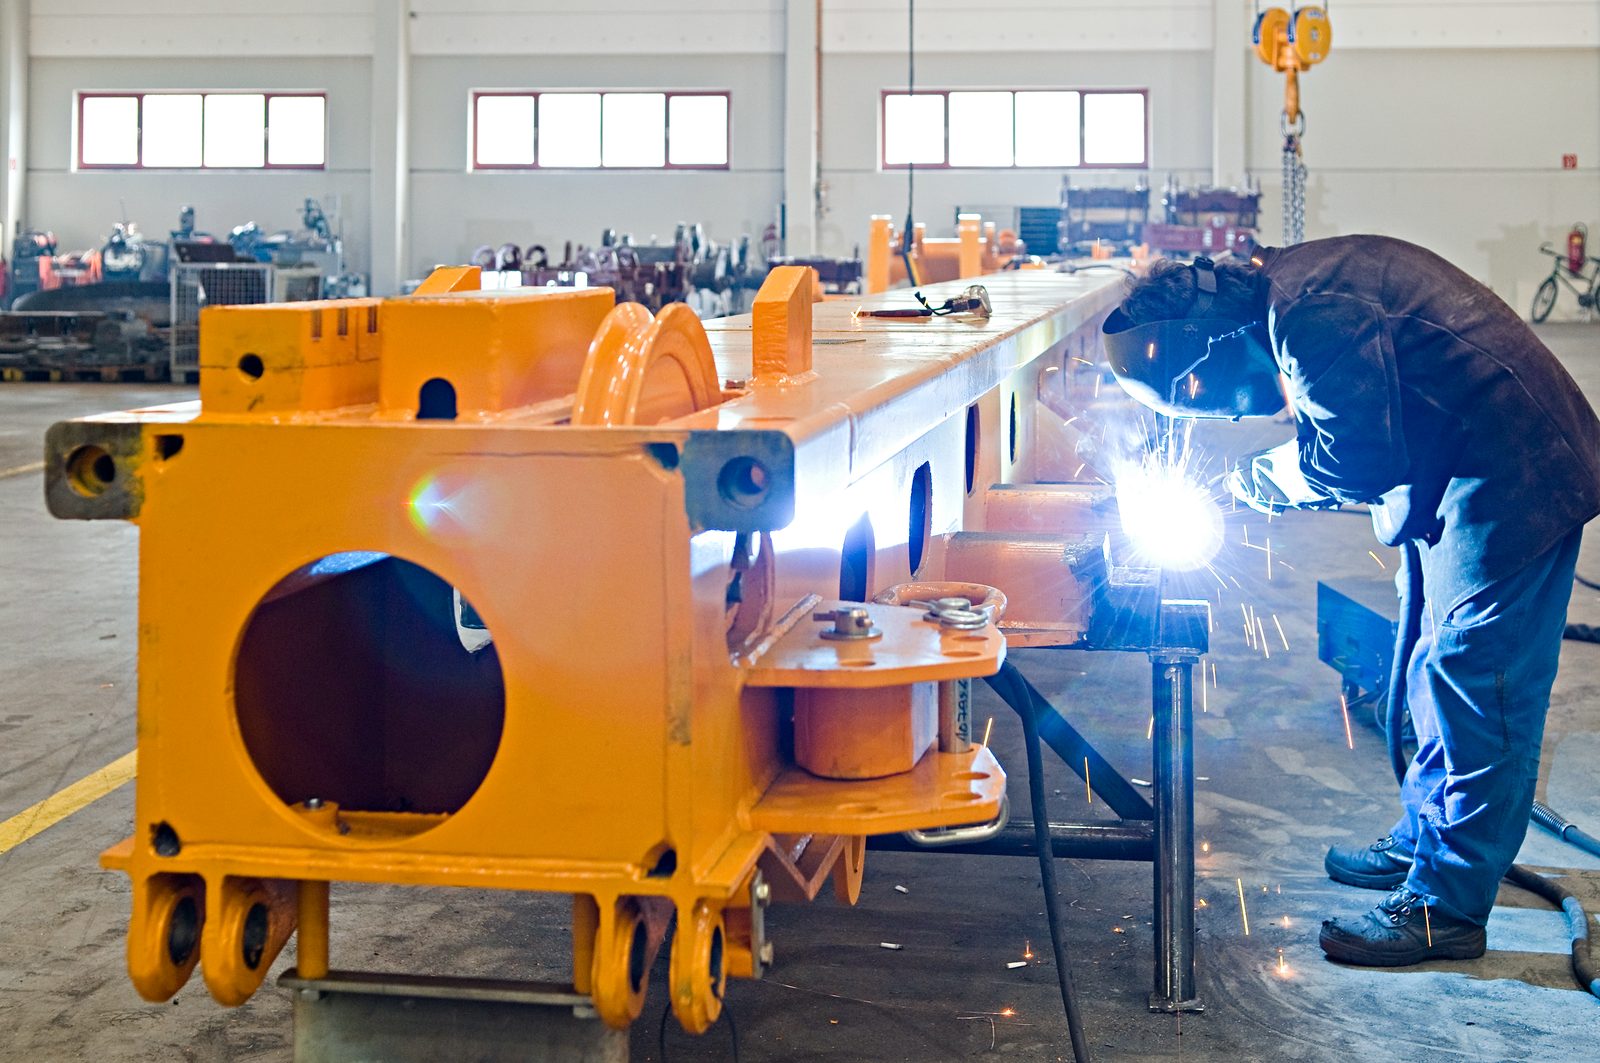
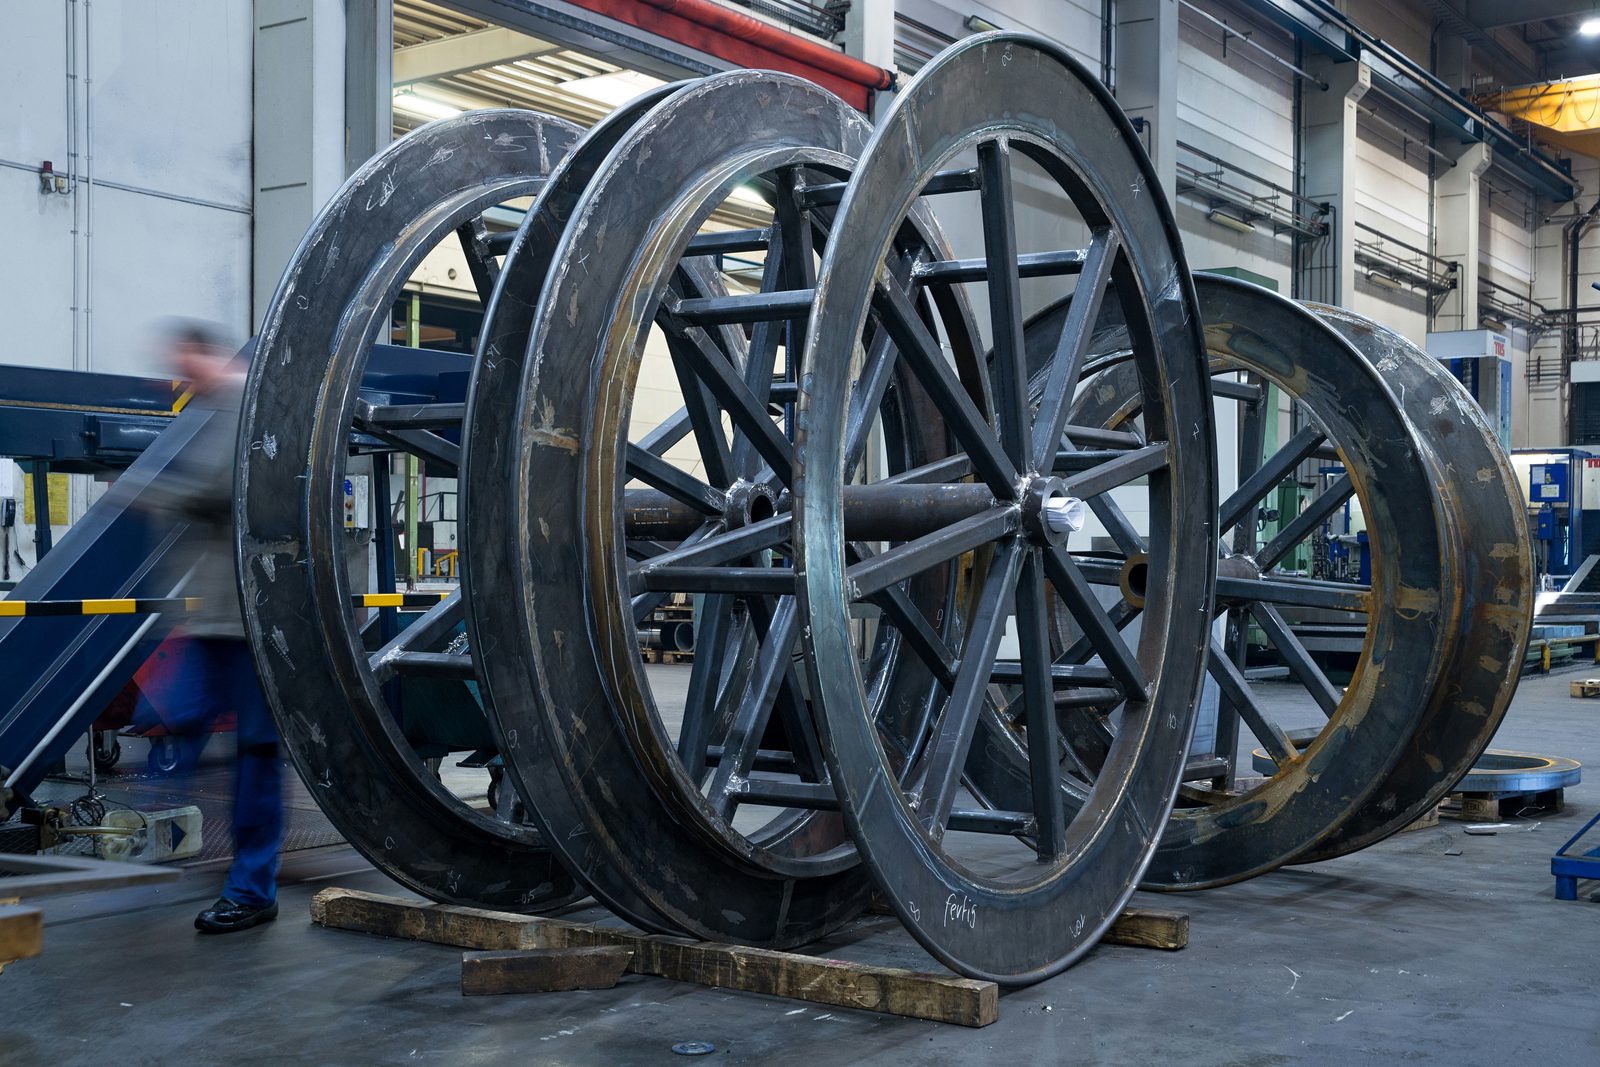
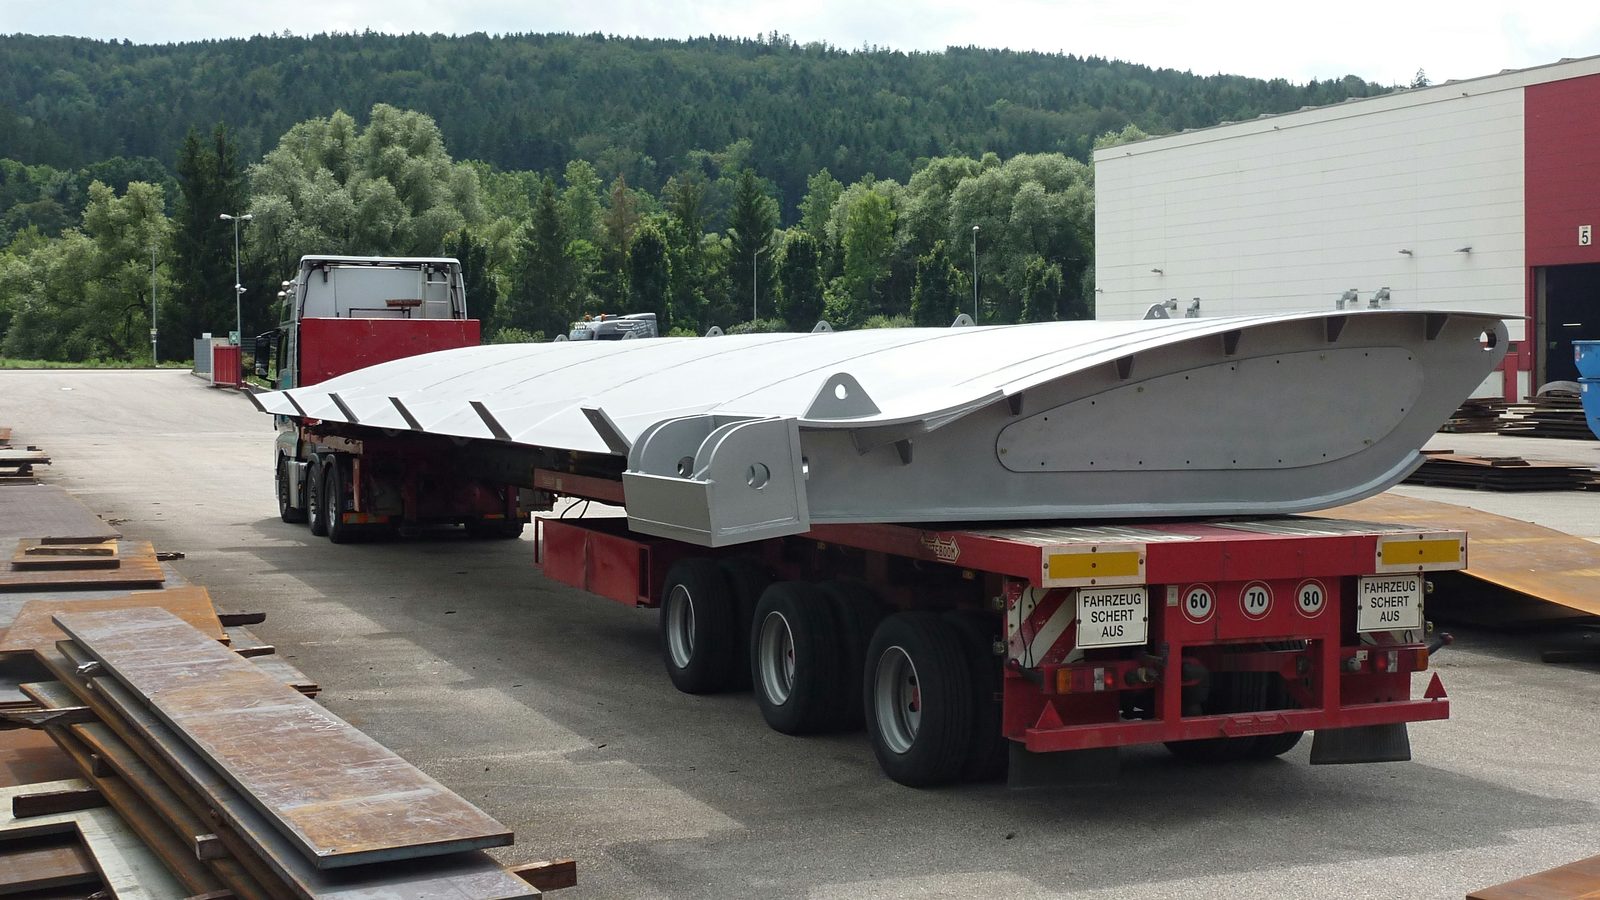
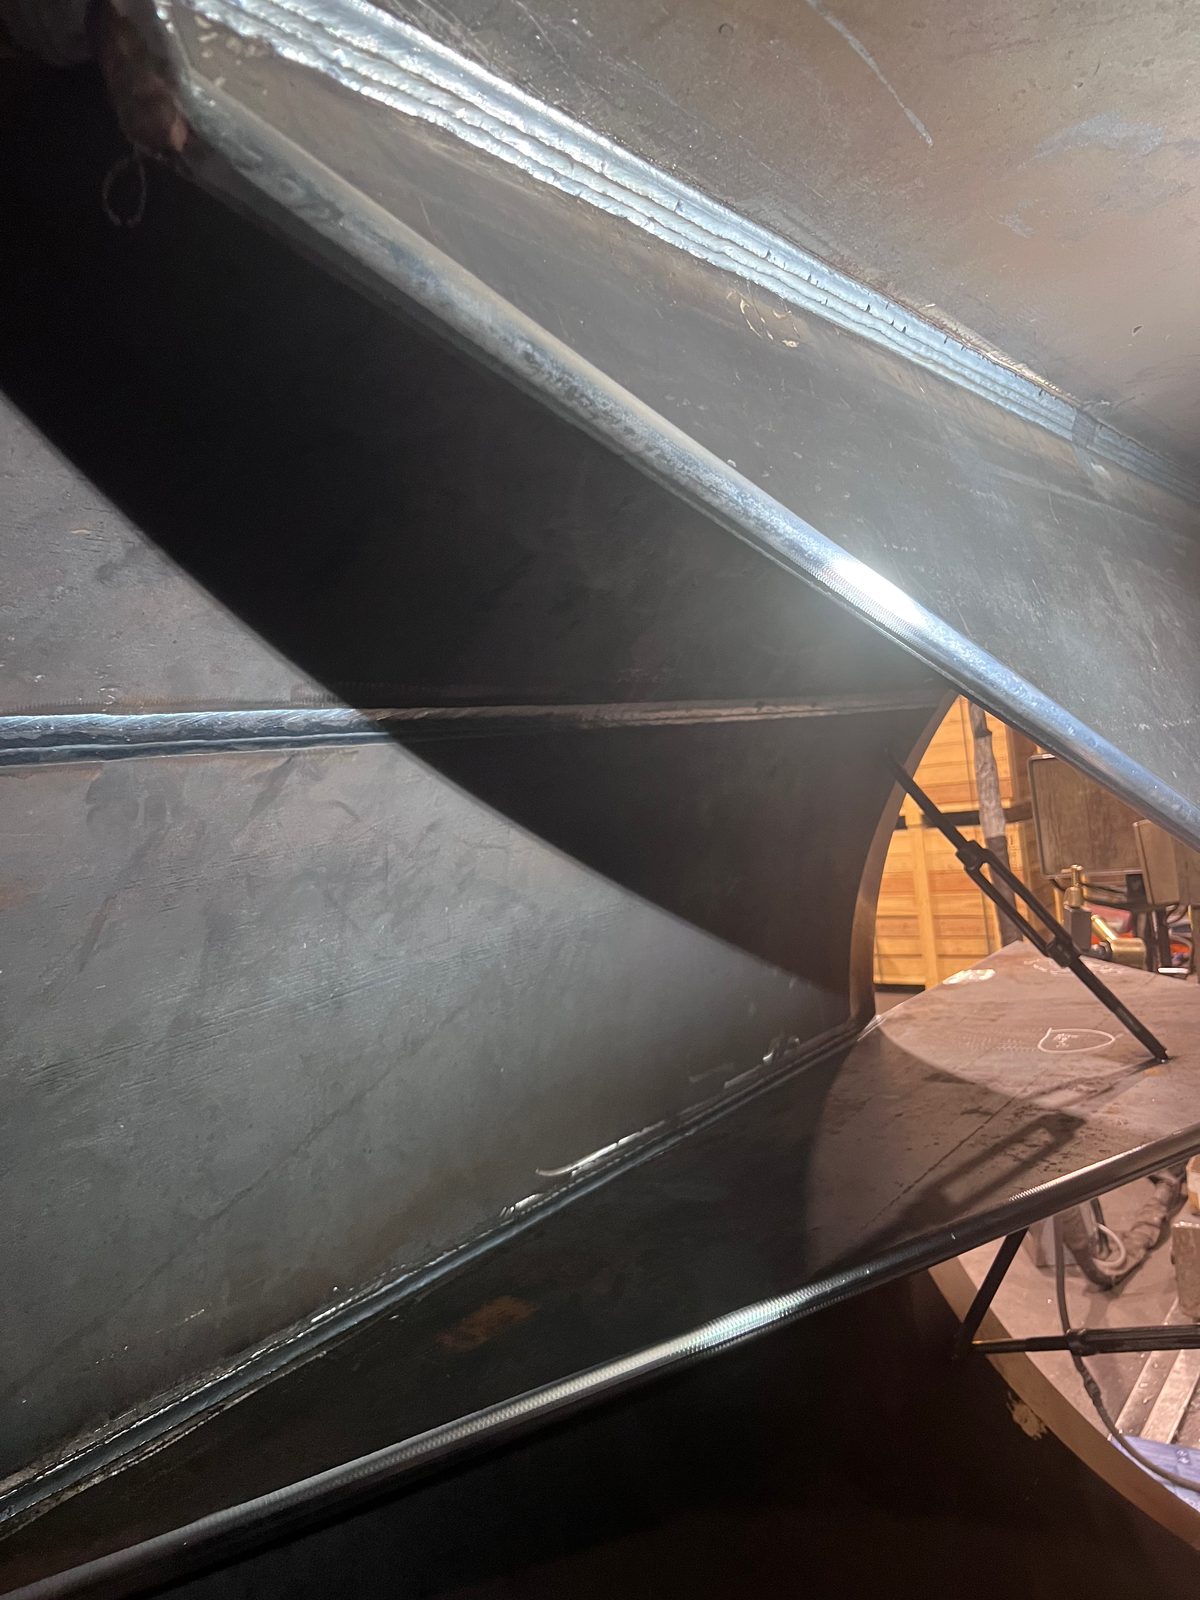
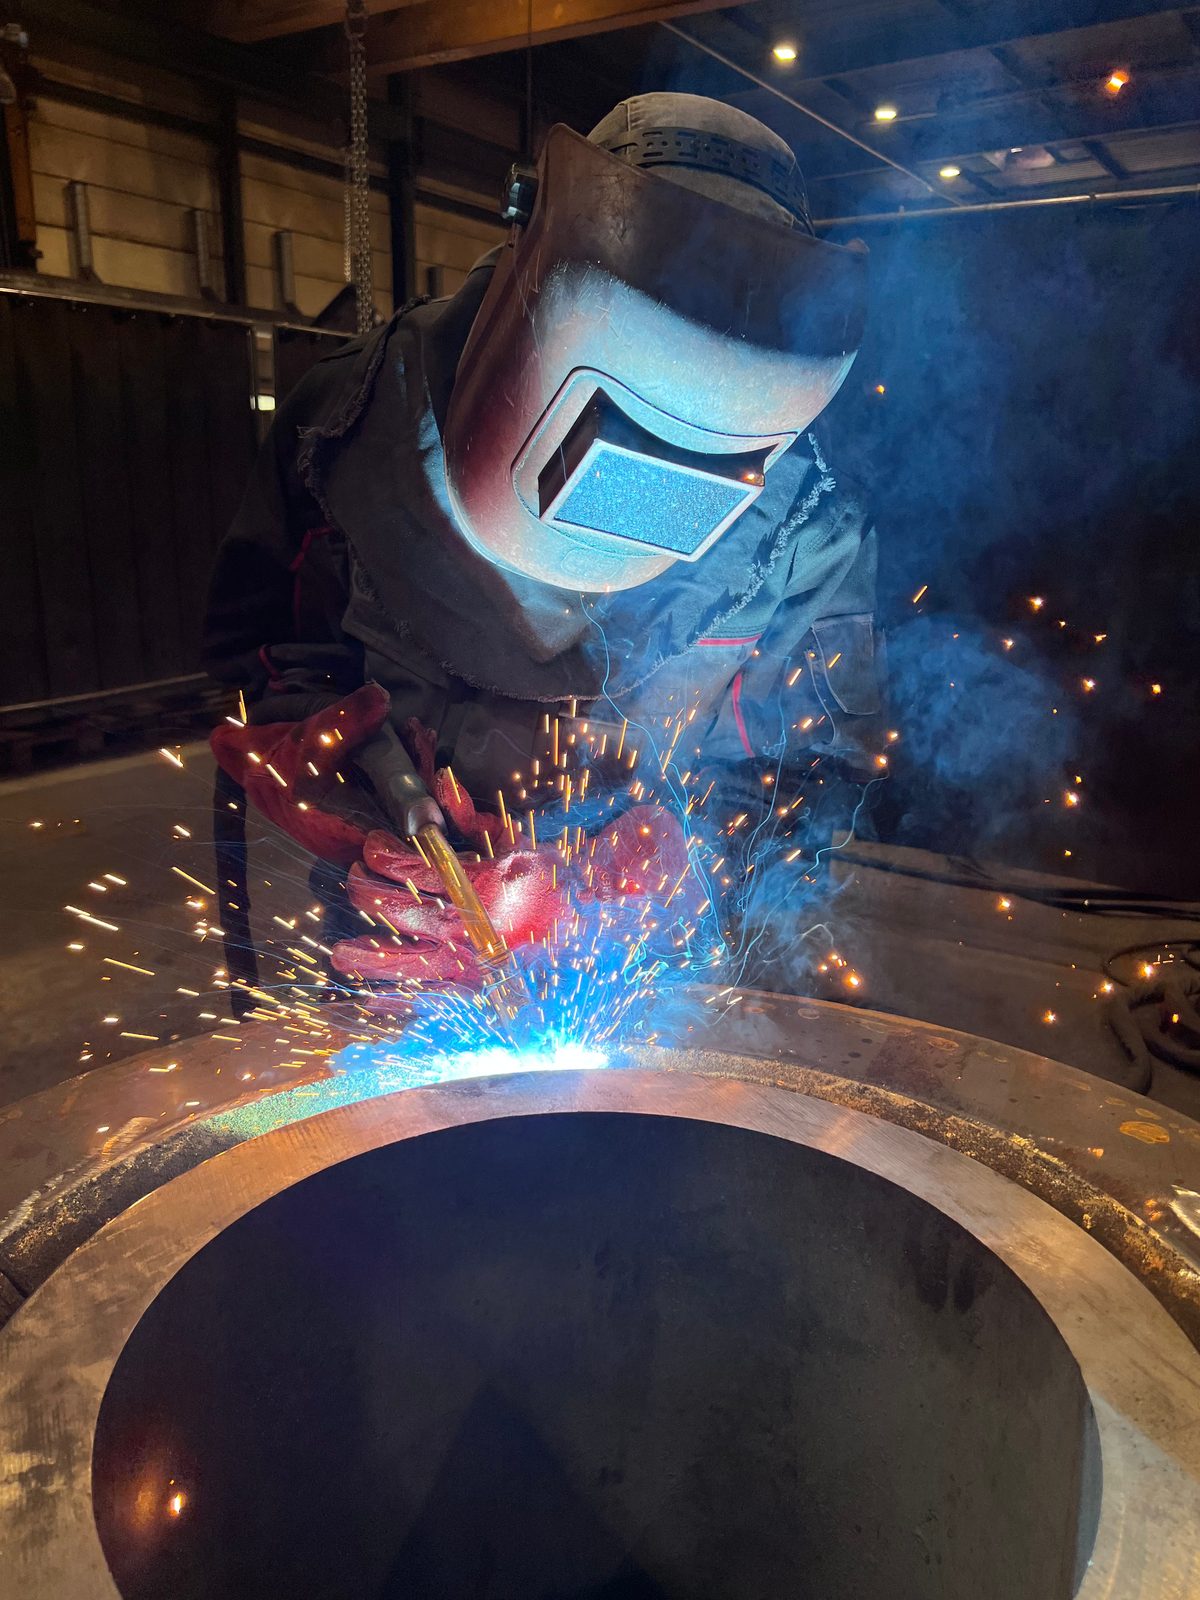
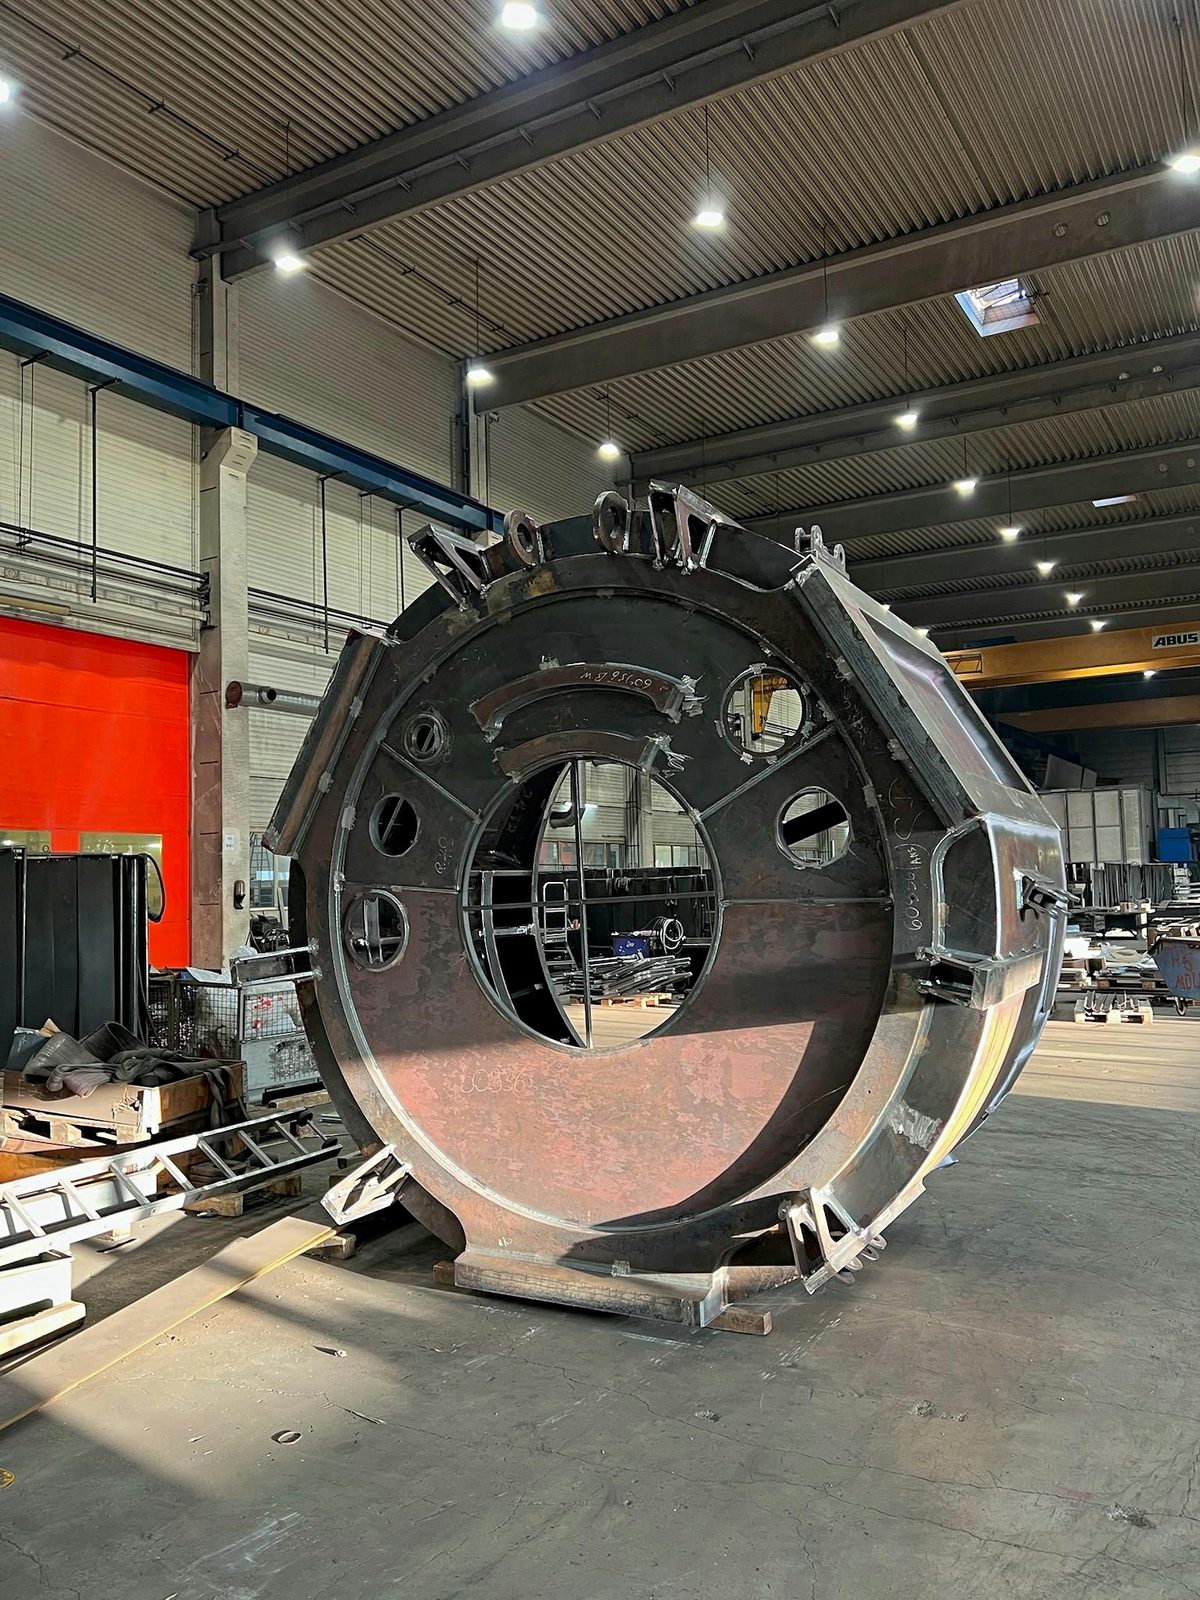
Real shots from our shop floor in Lorch – from the flame-cut bevel that prepares the joint, through welding on the part and the hand-welded MAG fillet weld beside the machined mating face, to a large welded assembly taking shape.
Bock Maschinenbau has been producing welded structures and heavy assemblies at its Lorch site for over six decades:

EXC3 contract welding of load-bearing assemblies for steel and plant builders from the Stuttgart area, the DACH region and across Europe – certified, from our facility in Lorch.
Which records are supplied is agreed on a project basis, for example material certificates with inspection certificate 3.1 to EN 10204, dimensional reports and non-destructive testing reports. The basis is certification to DIN EN 1090-2 EXC3 and EN ISO 3834-2 with quality management to DIN EN ISO 9001:2015; the current certificates are available as PDF.
Bock determines the process and joining sequence from the component and the weld cross-section; what is specified is the result – seam quality, tolerance and execution class. MAG welding is the standard process for structural steel components, TIG welding is used for stainless steel assemblies and SAW welding for deep weld volume – the processes can be combined within a single component.
Yes. In stud welding, headed and threaded studs up to Ø 22 mm are joined directly to the component – for fastening points, anchors and brackets without a through-hole.
Yes. The bevels for weld seam preparation are produced in production in Lorch, either on the edge milling machine (Alme) up to 12 × 45° or as a flame-cut bevel.
Around 100 shielding-gas welding stations, mainly MAG, plus TIG (Oerlikon, ESAB, Lorch, ESS), as well as three ESAB submerged-arc systems with column and boom masts. Welded assemblies are produced up to 50 t unit weight.

Send us your drawing, material, quantity and your inspection and documentation requirements. We weld the assembly to EXC3 – on request including machining, blasting, painting and assembly in the same plant.