Durably coat large components and heavy parts up to 50 t – industrial painting to EN ISO 12944 in a 25 × 7 × 6 m booth, blasting and painting from a single source in Lorch.
For large components and long welded structures in a single setup.
Handled via the 2×25 t crane system straight from welding and CNC machining.
Coating system and corrosivity category to specification – up to C5 with high durability (H).
Surface preparation without intermediate transport – short turnaround times.
Welding, press brake bending, CNC machining, blasting and painting within the same facility.
Quality management to DIN EN ISO 9001:2015, certified welding contractor to DIN EN 1090-2 EXC3.
Industrial painting provides durable corrosion protection for steel components and welded structures. Painting is carried out to EN ISO 12944 – an international standard that defines corrosion protection categories, coating systems and requirements for surface preparation and coating materials.
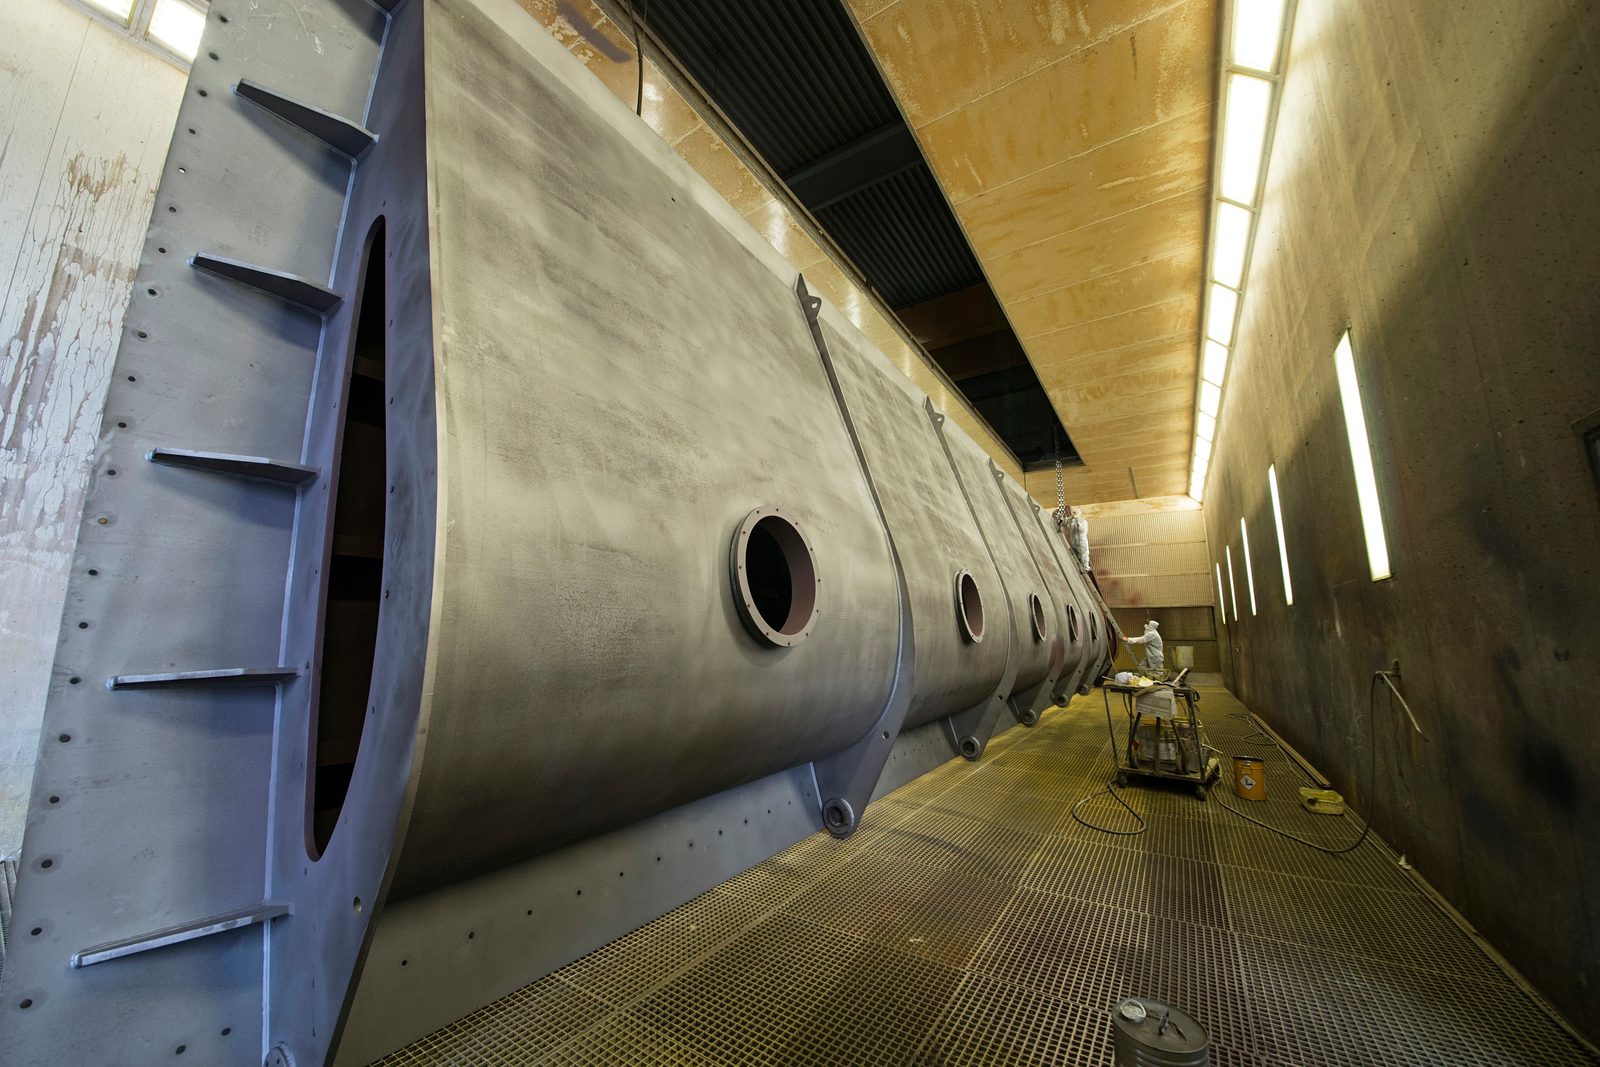
At Bock, painting is carried out in a large-format spray booth that can accommodate large welded structures, machine parts, vessels and special-purpose components. Shot blasting as surface preparation is available in-house within the same facility – transfer and handling are carried out via the in-house crane system.
Painting is embedded within the certified quality management system to DIN EN ISO 9001:2015. Coating build-up, surface preparation grade and coating requirements are defined and documented on a project basis in accordance with drawings, normative requirements and customer specifications.
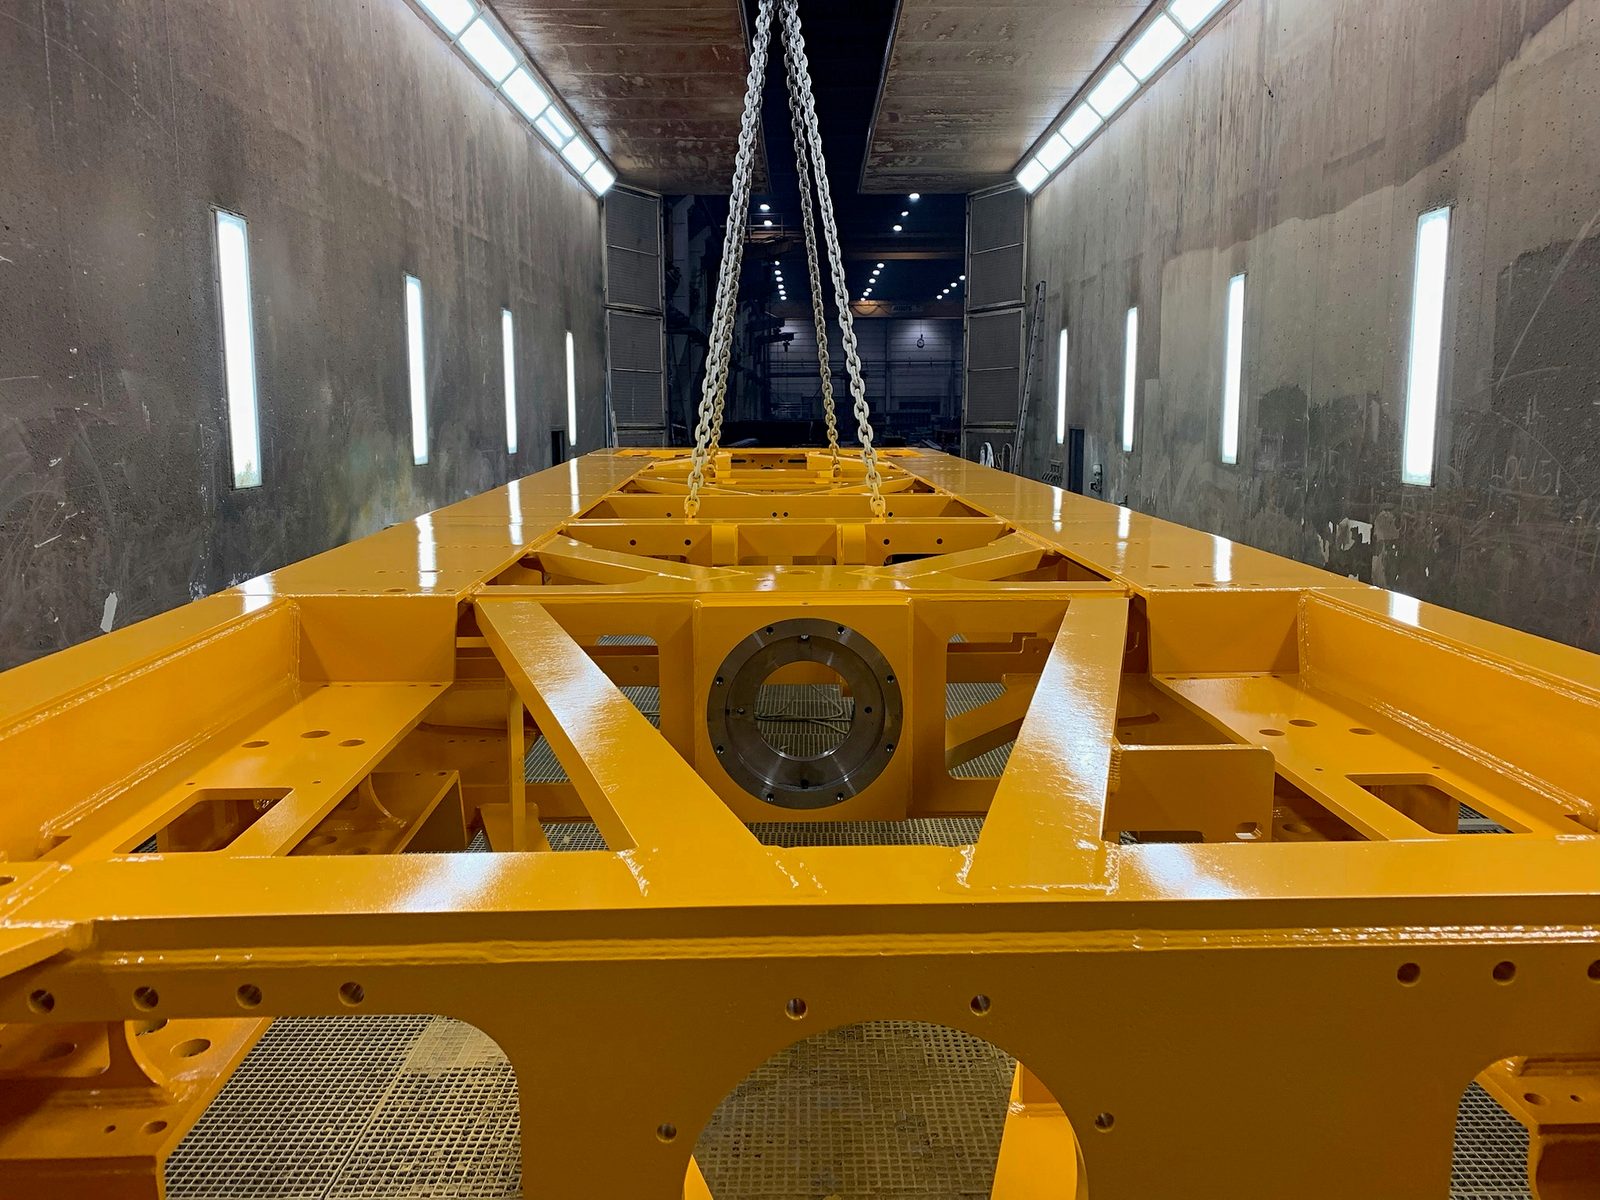
Industrial painting at Bock is carried out in six steps: receiving and masking, blasting to Sa 2.5, cleaning and priming, intermediate coat and topcoat, measuring the film thickness and loading.
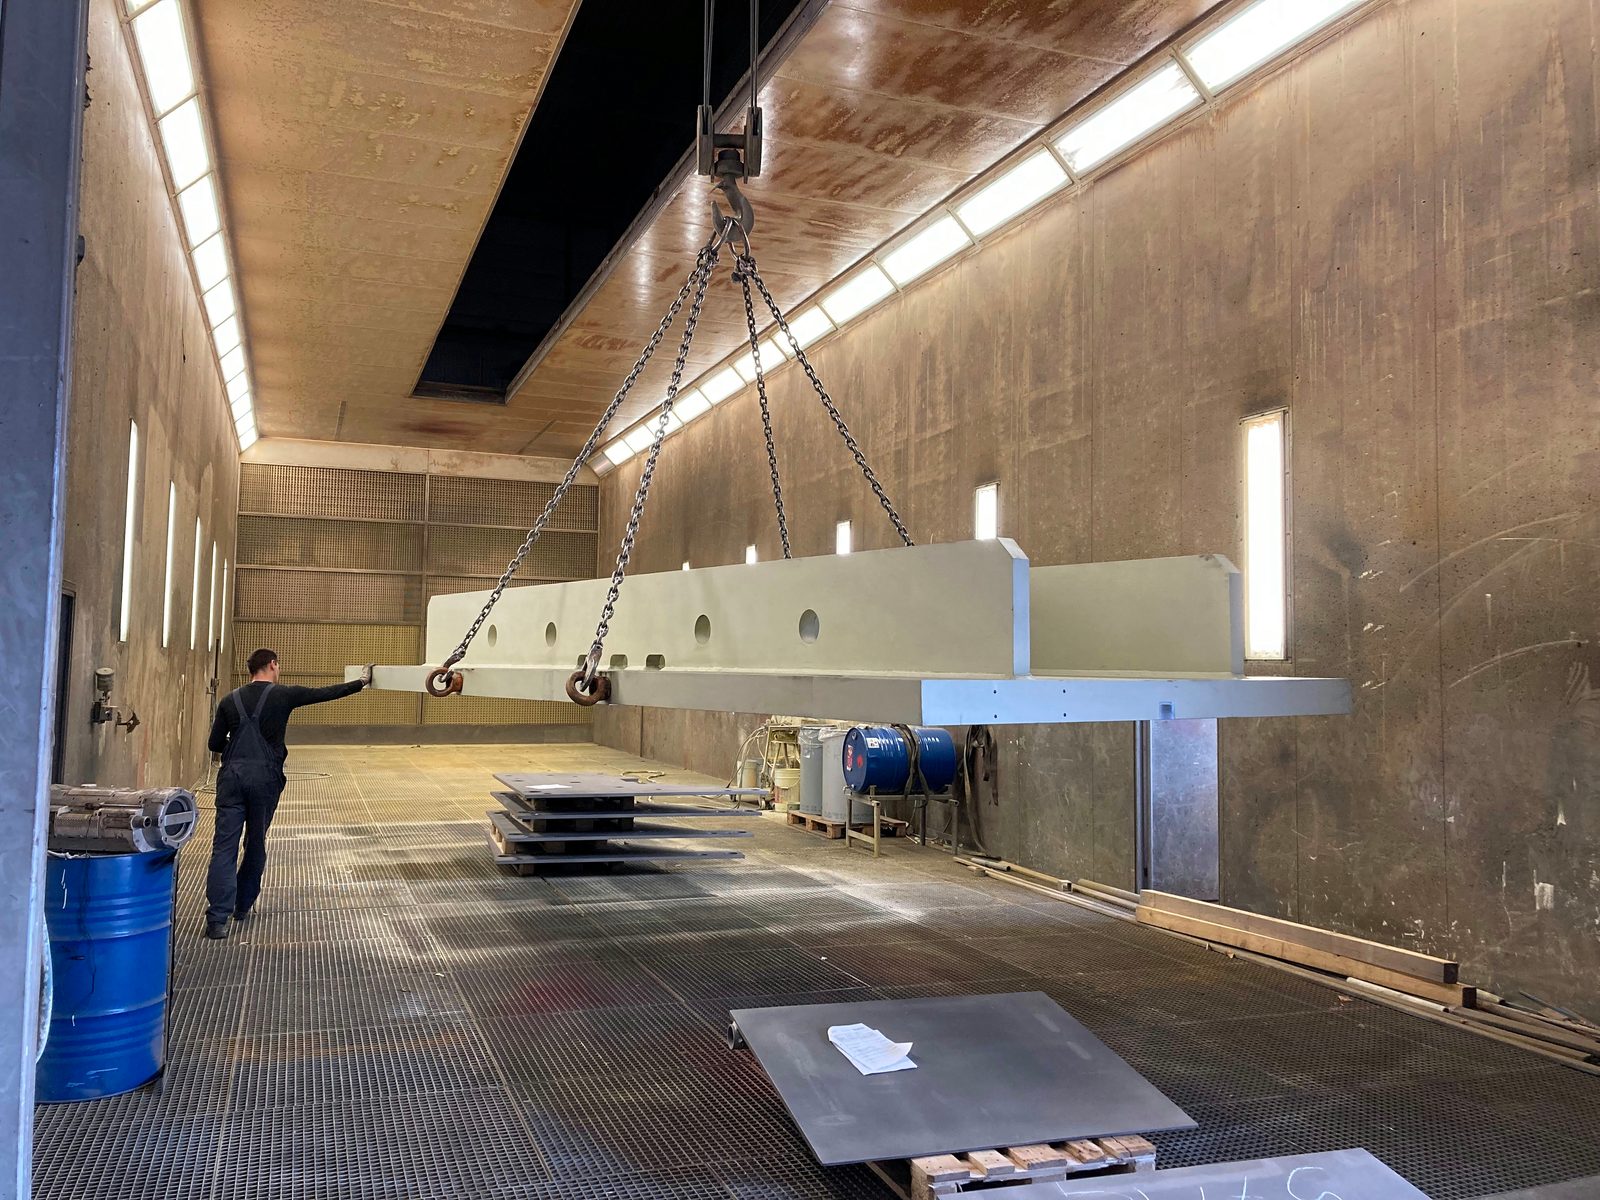
The component arrives via the overhead crane system directly from welding or CNC machining. Mating surfaces, bores and threads that are to remain bare are masked.
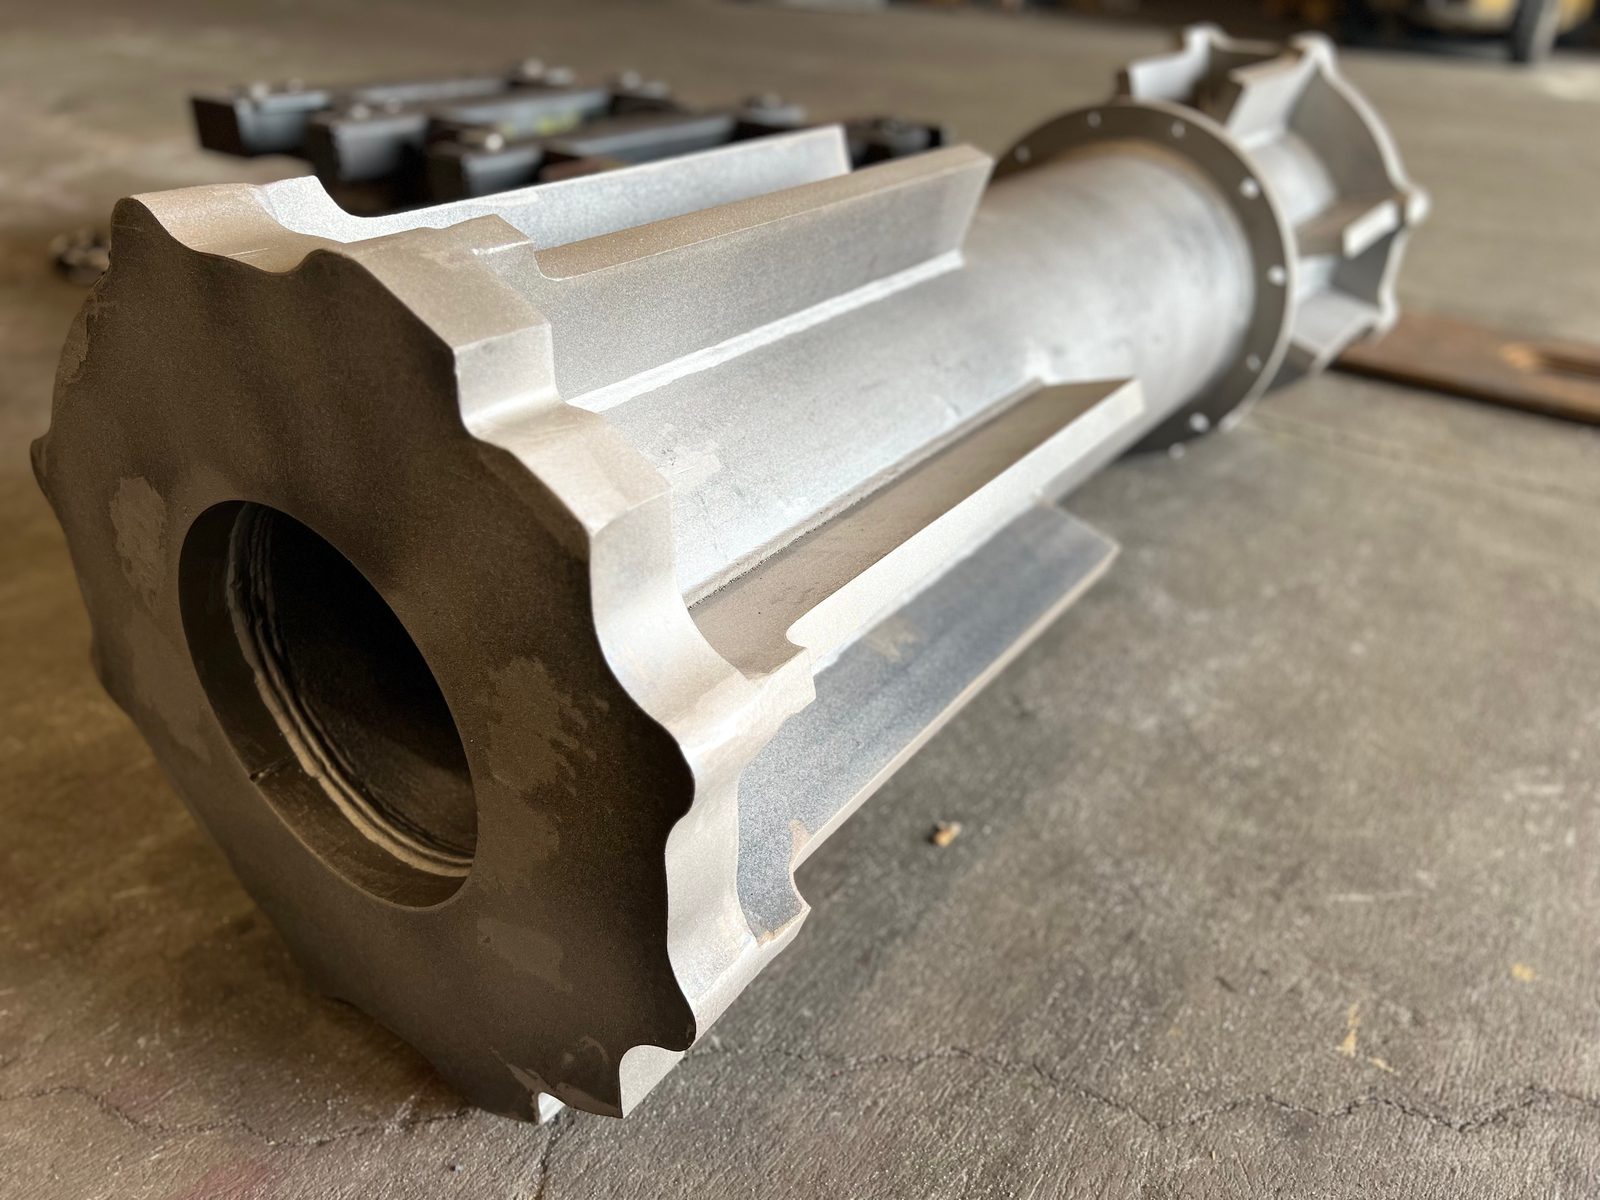
In the large-format blast chamber, the surface is blasted with steel grit or corundum to cleanliness grade Sa 2.5 to ISO 8501-1. Mill scale, rust and old coatings are then removed.
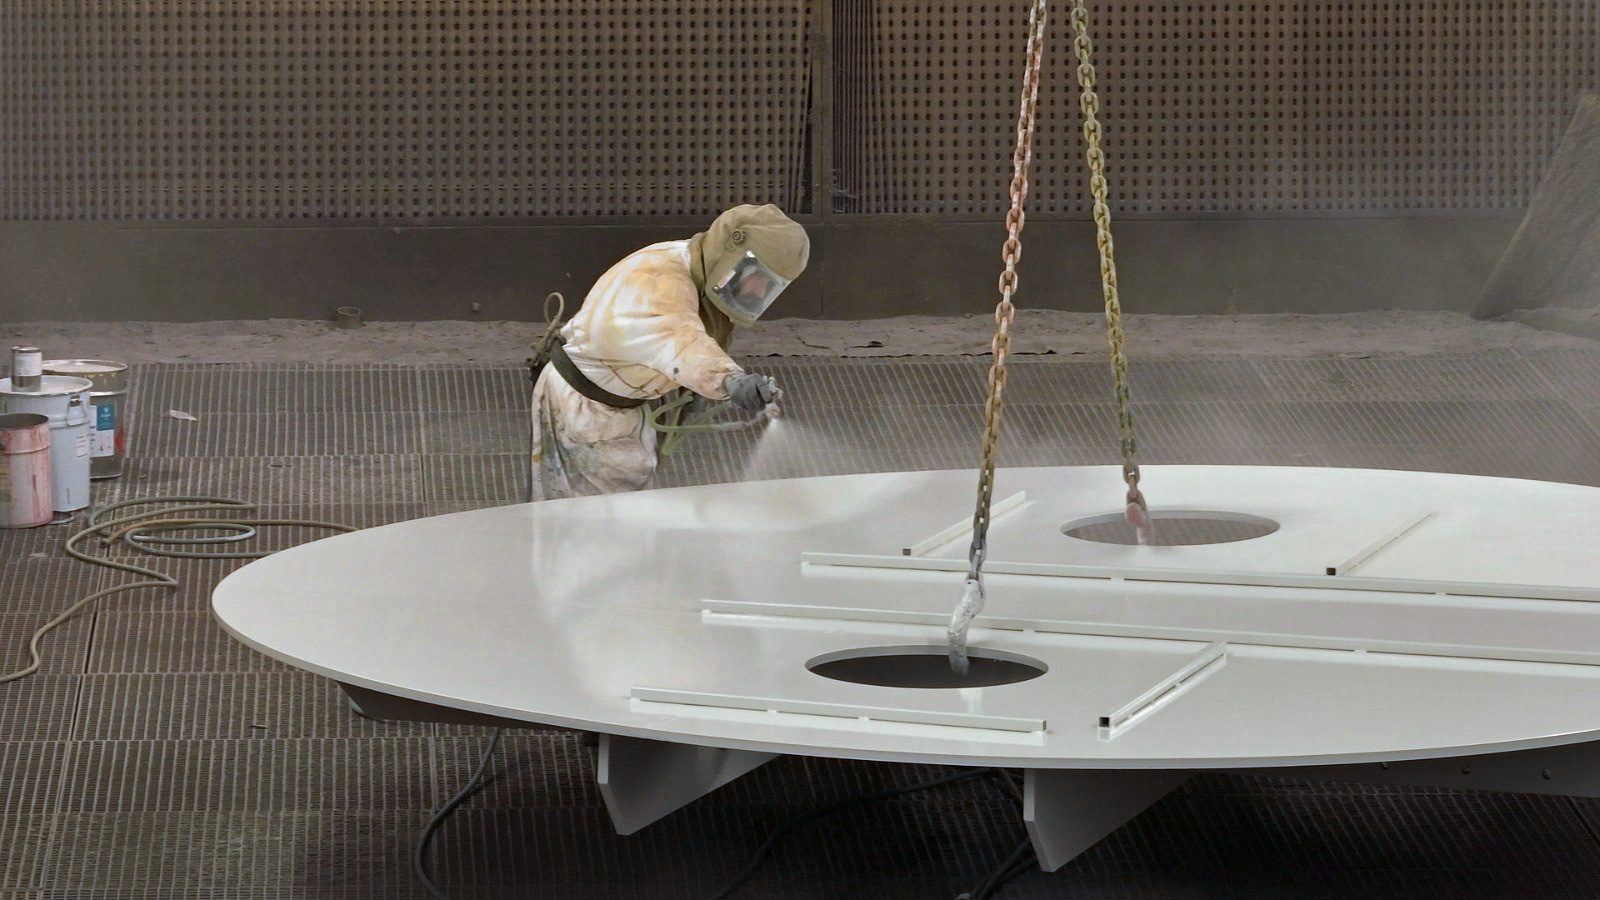
Immediately before painting, the surface is cleaned with thinner. The primer follows as the first coat of the coating system.
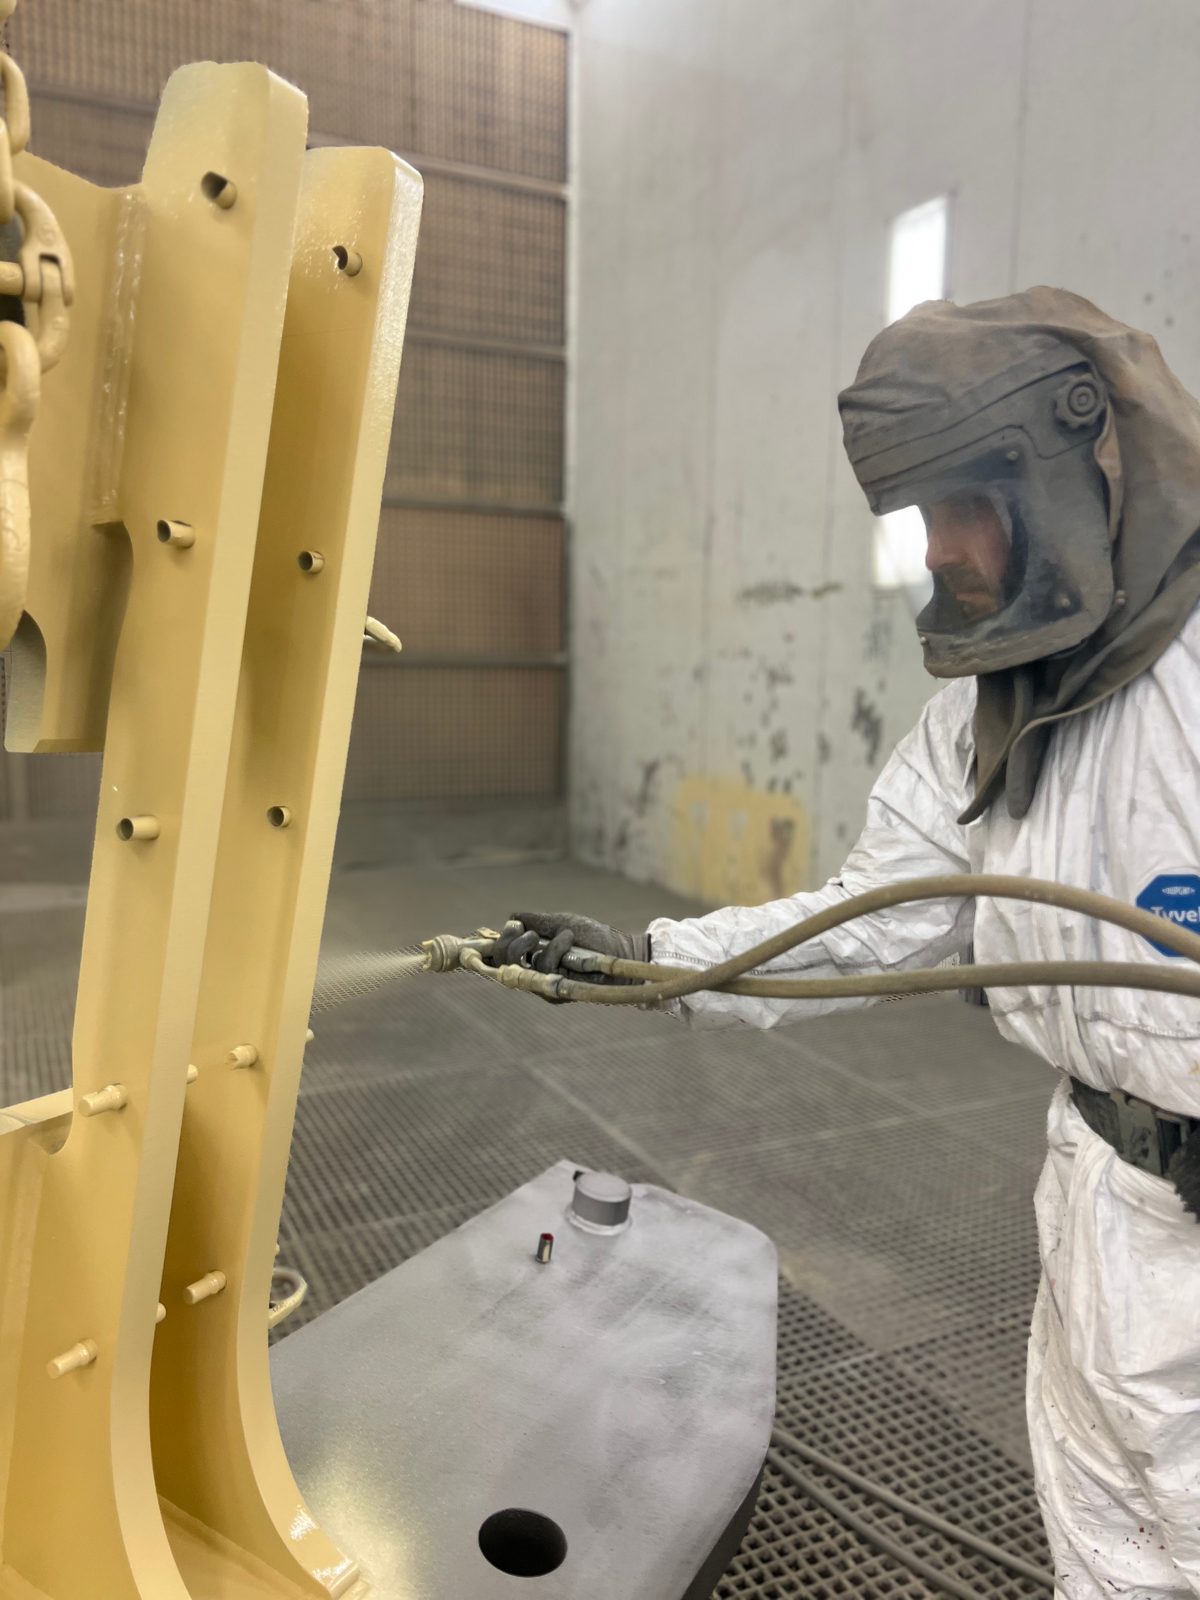
Intermediate coat and topcoat build up the coating system to EN ISO 12944 – in a colour shade to RAL or customer specification and in the required gloss level. Each coat dries before the next one follows.
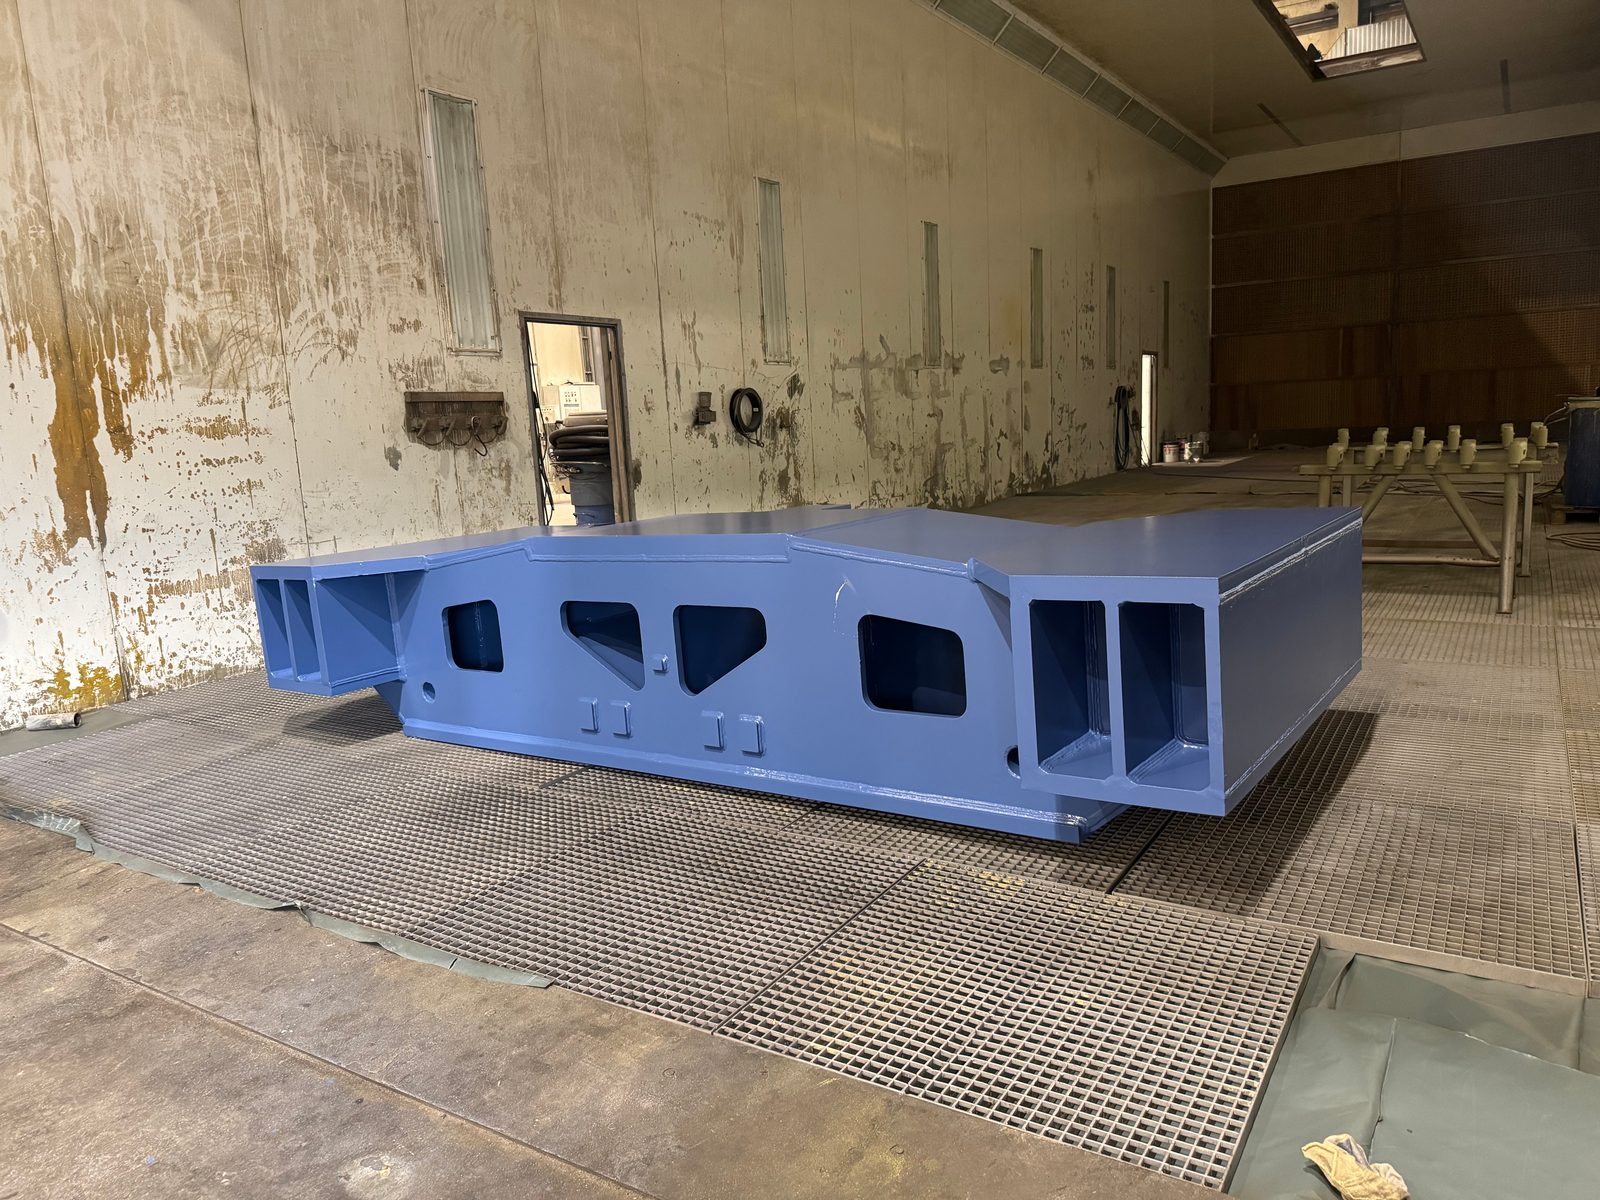
The dry film thickness is measured. On request, we record it together with the preparation grade and coating build-up for the delivery documentation.
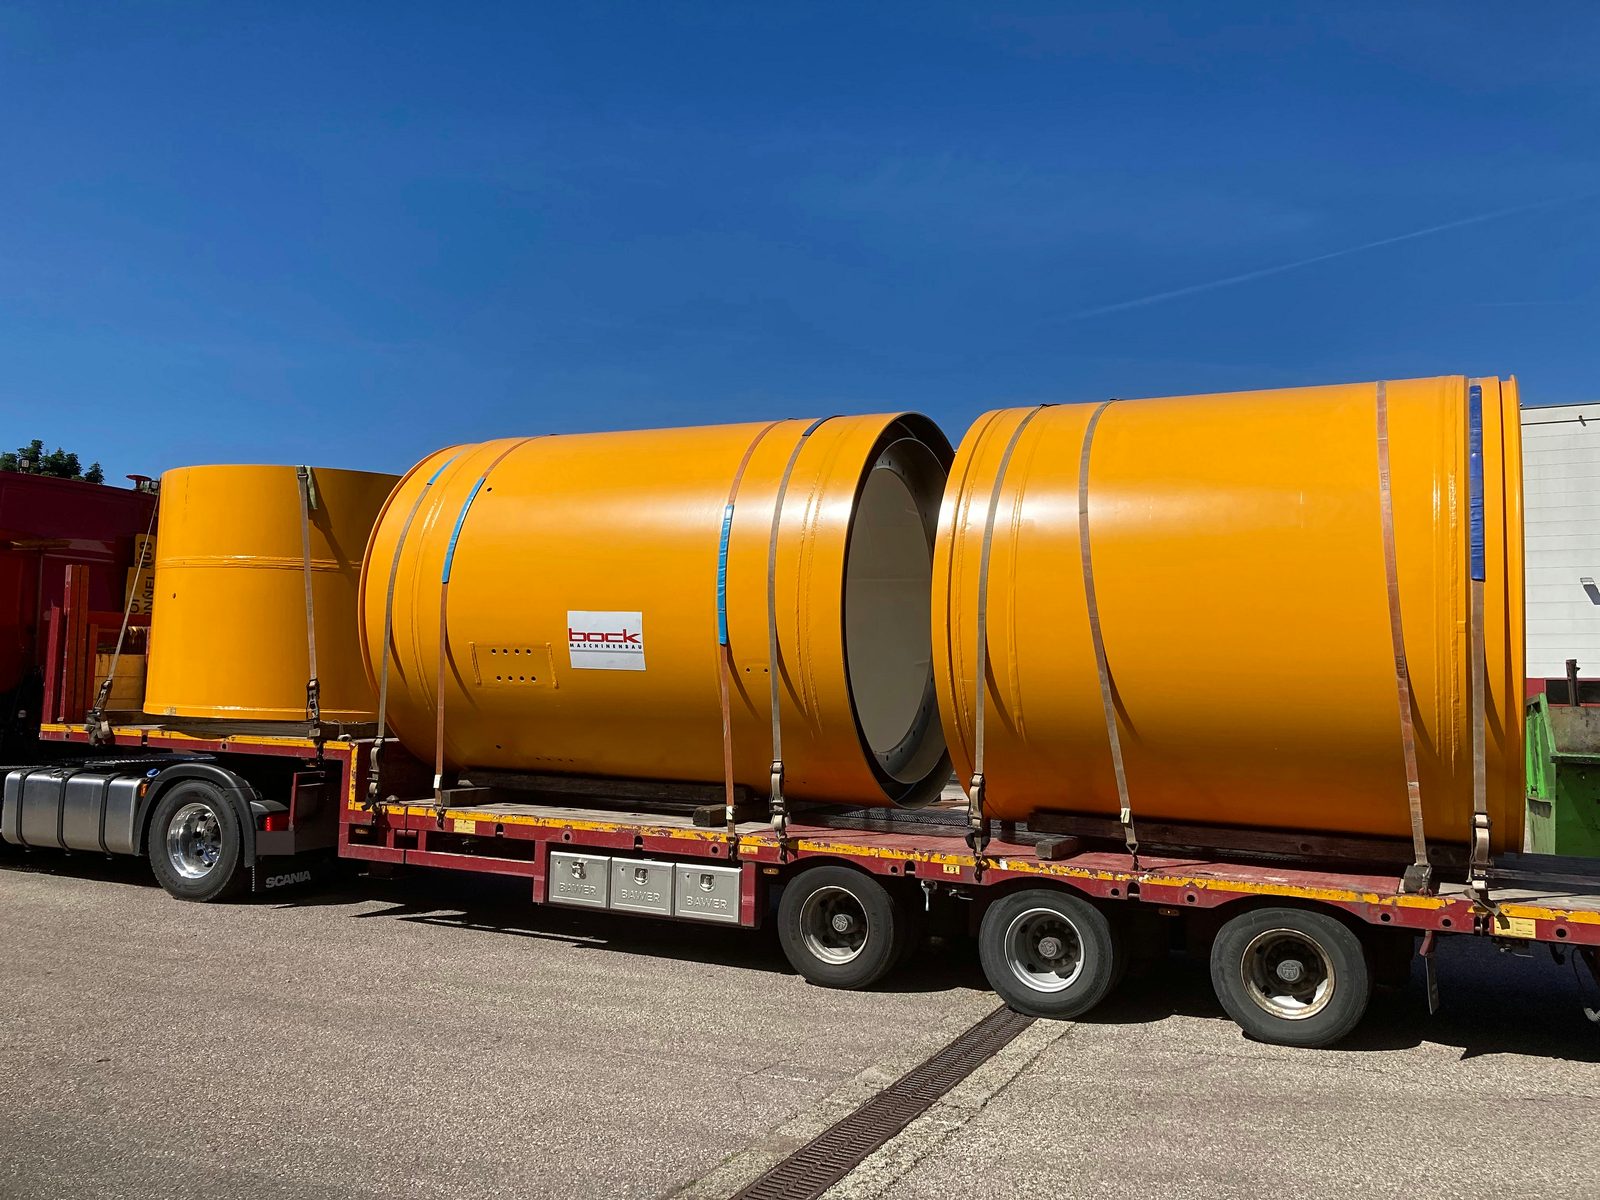
The masking is removed, and the painted component is loaded and secured for transport.
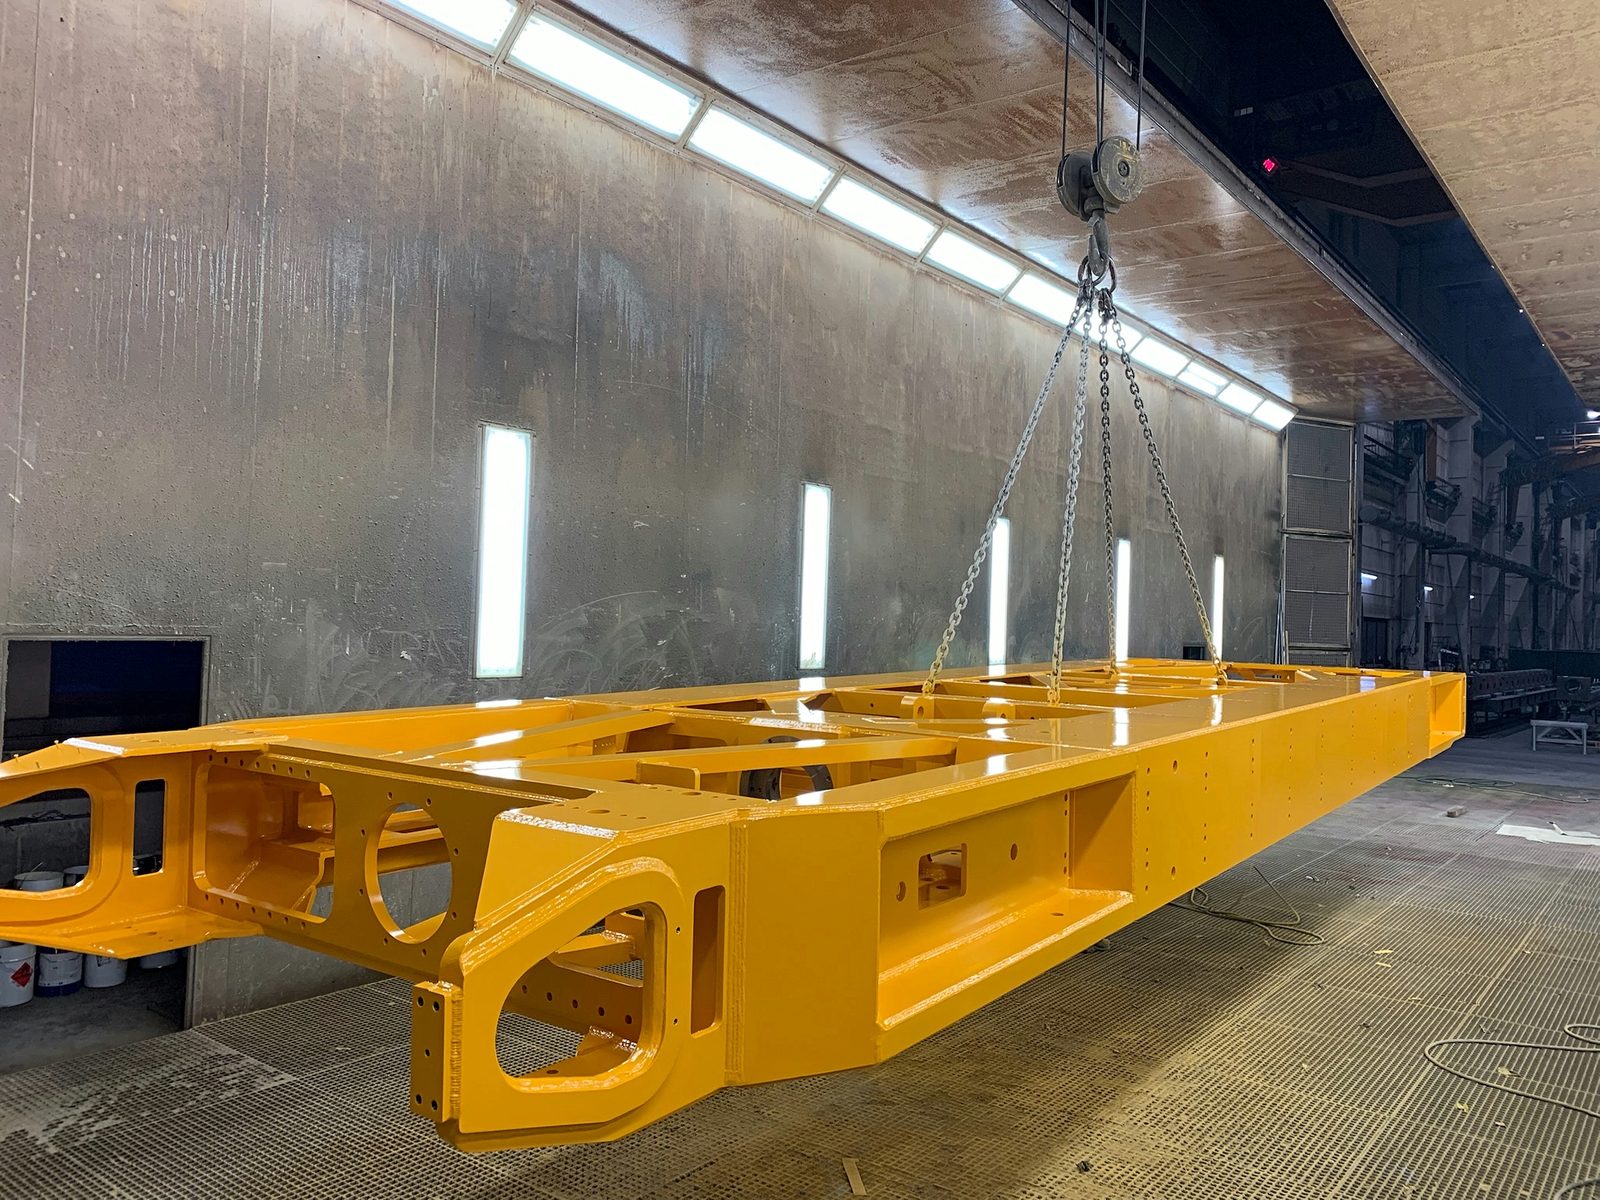
The 2×25 t crane system brings heavy parts up to 50 t directly from welding and CNC machining into the spray booth.
Coating build-up and corrosivity category are defined according to drawing and customer specification – up to C5 with high durability (H).
Shot blasting to Sa 2.5 immediately precedes painting – without intermediate transport to third parties.
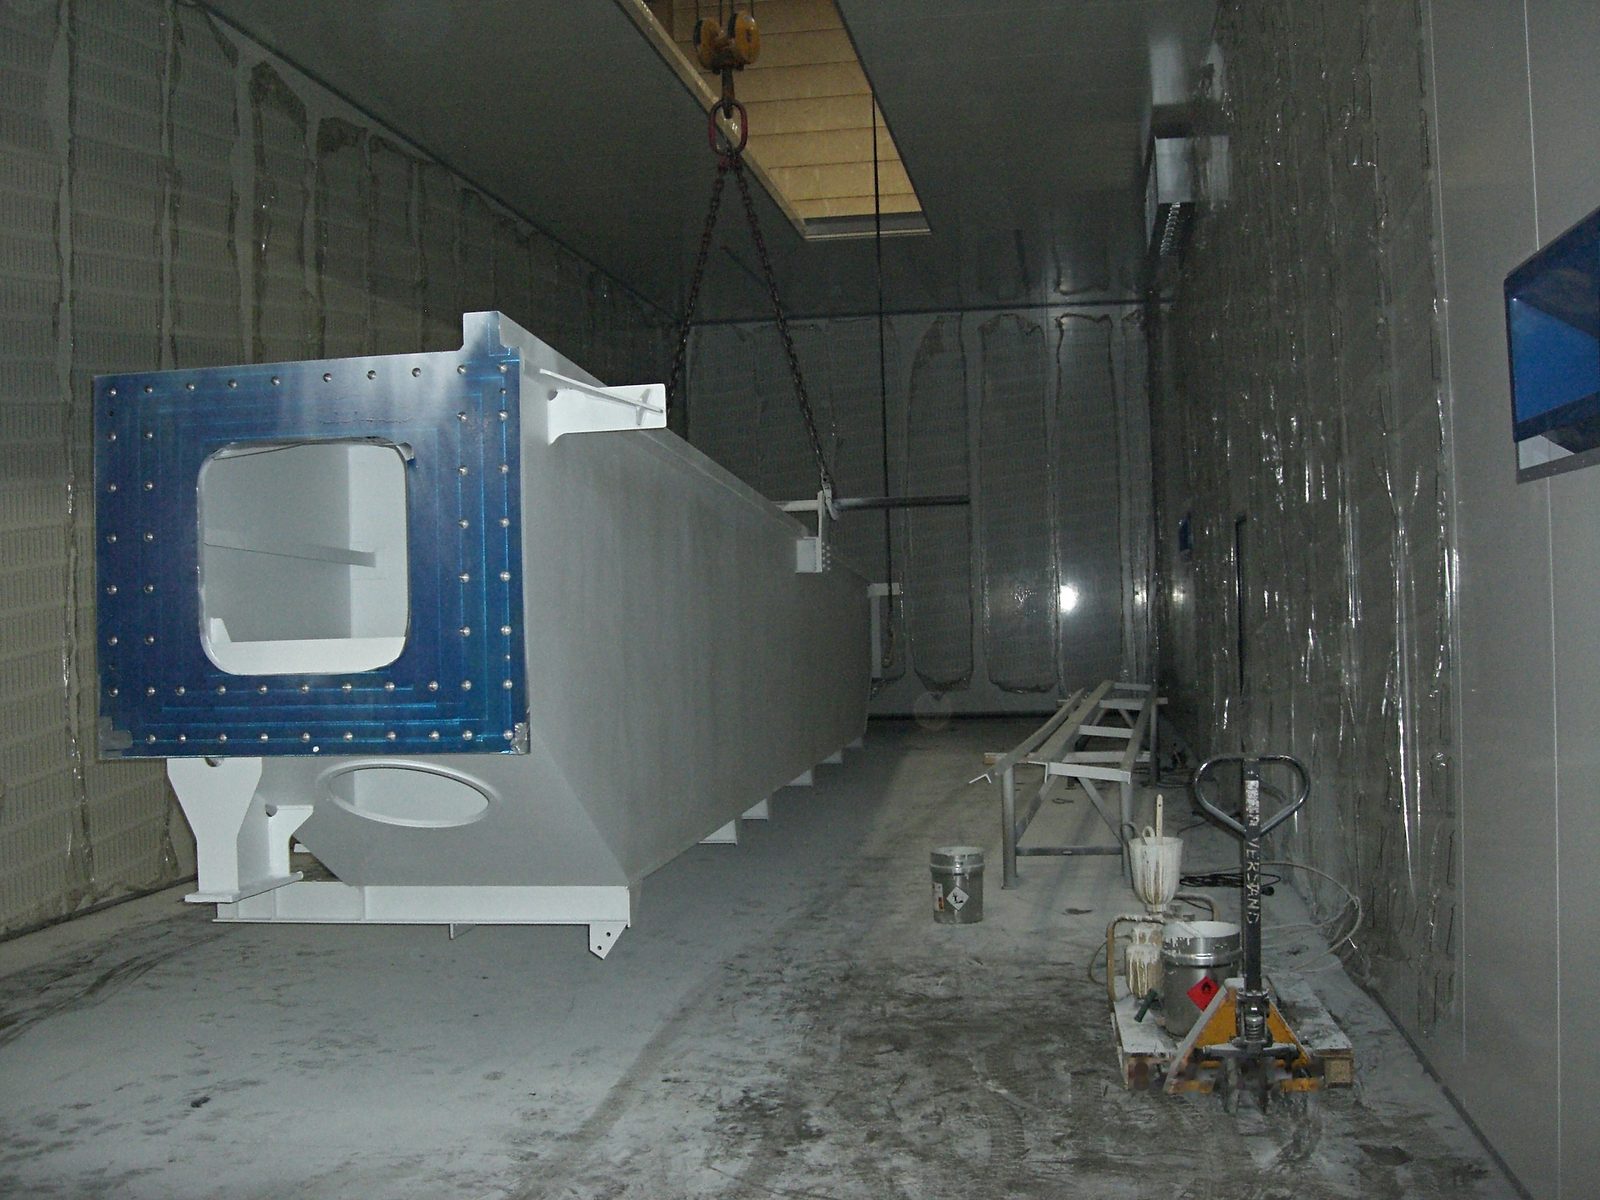
The spray booth at Bock has a usable interior of 25 × 7 × 6 m. These dimensions enable large components, long welded structures and large-format machine elements to be accommodated – for which standard spray booths are not designed.
Via the 2×25 t crane system in the production facility, heavy components up to 50 t can be safely positioned and transferred into the booth. This eliminates separate transport operations and shortens the throughput time between welding, blasting and painting.
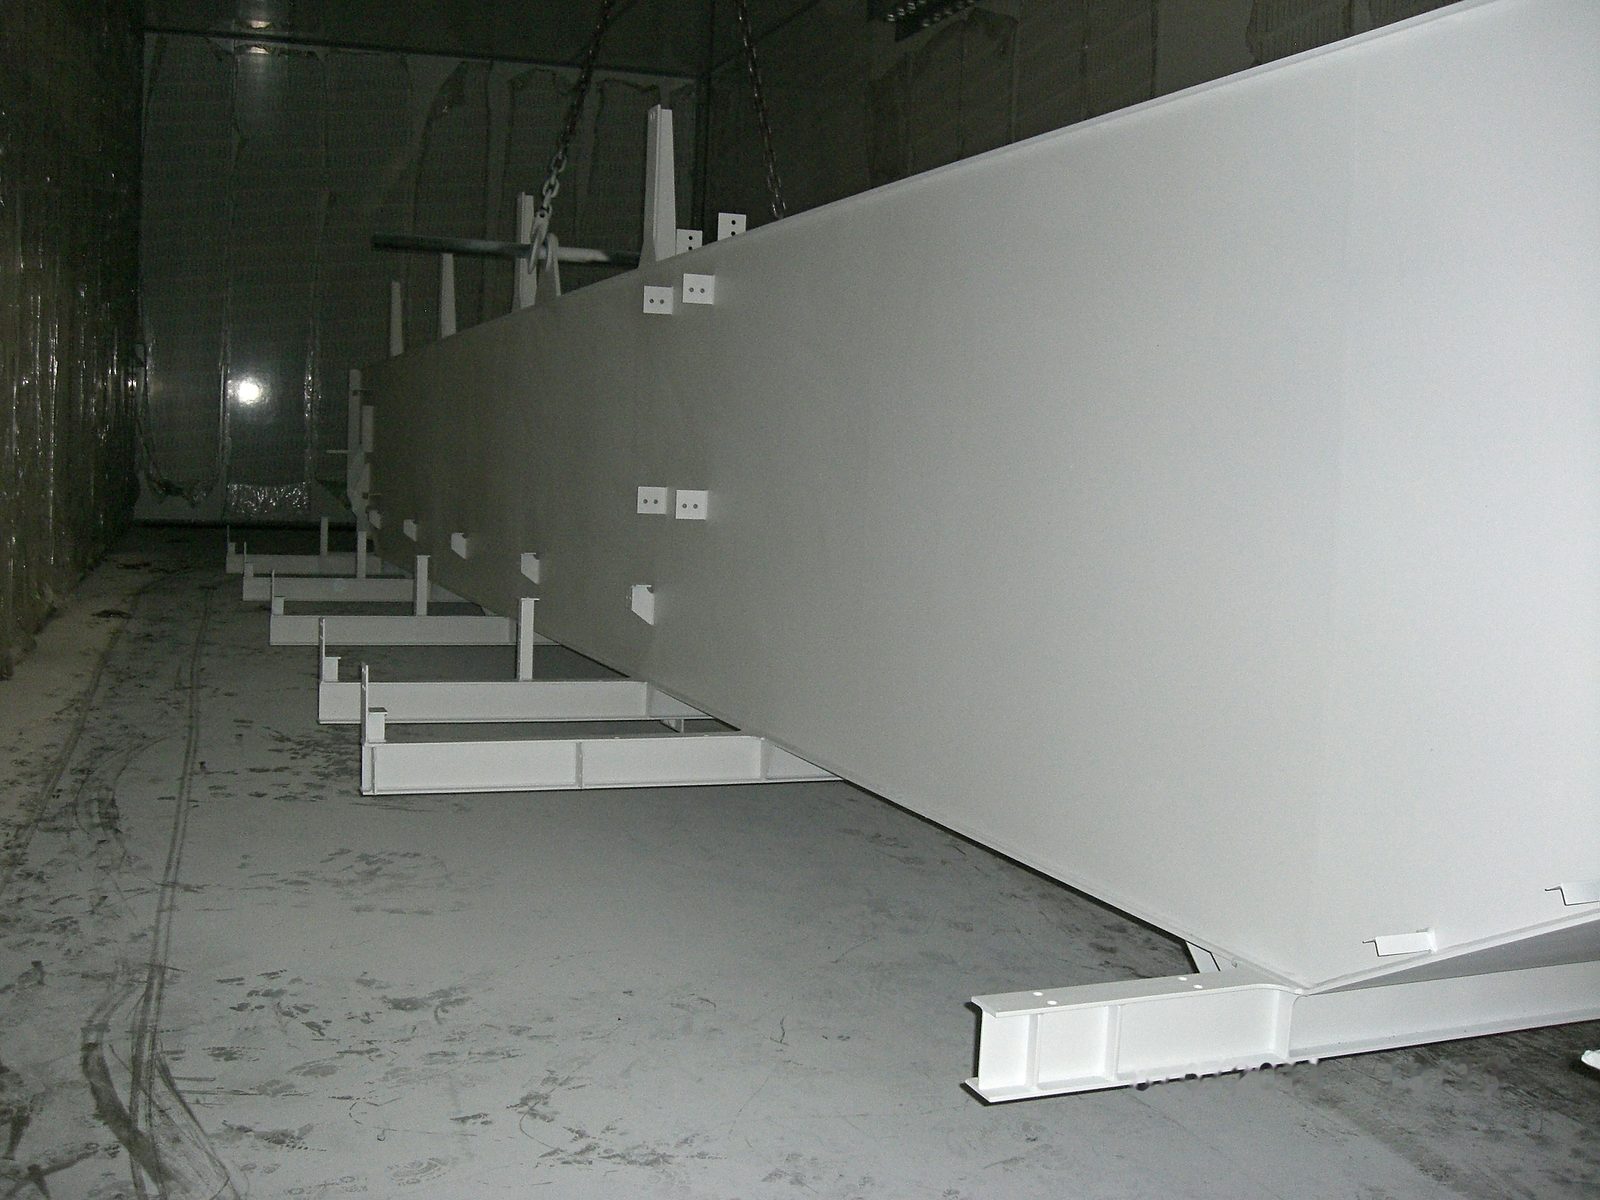
| Parameter | — |
|---|---|
| Cabin length | 25 m |
| Cabin width | 7 m |
| Cabin height | 6 m |
Durable adhesion of a coating requires a defined surface preparation. At Bock, shot blasting to Sa 2.5 is available in-house in a large-format blast chamber.
Sa 2.5 is the cleanliness grade required by EN ISO 12944 as the basis for most corrosion protection coating systems. Through the spatial integration of blast chamber and spray booth within the same facility, no intermediate transport is required – components are painted immediately after blasting.
The blast chamber has the same large-format dimensions as the spray booth and is designed for heavy components up to 50 t.
In flame-spray galvanizing, zinc is melted in a flame and sprayed onto the blasted steel surface. The zinc layer protects the steel cathodically – like hot-dip galvanizing, but without a zinc bath.
The component is heated only slightly in the process. The method is therefore suited to welded structures that would distort in a zinc bath, to components that are too large for a zinc bath and to touching up galvanized surfaces after welding.
The surface is prepared in our own blast chamber; there is no transport to an external galvanizing plant.
On request, the zinc layer is primed and top-coated in the same plant. This duplex system of spray galvanizing and coating is produced without transport between galvanizer and paint shop.
Industrial painting at Bock is suited to a broad range of steel components and materials:
Coating system, build-up and requirements for adhesion primer and corrosion protection category are defined on a project basis to EN ISO 12944 and customer specifications.
We take the colour scheme and coating build-up from the drawing and the coating specification. Painting covers, among other things:
If no paint manufacturer is specified, we select the coating system to suit the corrosivity category and operating conditions.
Painting production at Bock is embedded within the certified quality management system to DIN EN ISO 9001:2015. Coating build-up, preparation grade and coating requirements are defined and documented to drawing, normative requirements and customer specifications.
EN ISO 12944 sets out requirements for corrosion protection of steel structures by coating systems – including corrosivity categories, film thicknesses, preparation grades and expected durability. The specific corrosion protection category and coating system are agreed according to project requirements.
For components manufactured as part of certified welded assemblies to DIN EN 1090-2 EXC3, painting can be embedded within the overarching quality framework of the welding operation. Inspection and documentation requirements are agreed on a project basis.
Painting at Bock is not an isolated step but part of an integrated production workflow. The following upstream processes can be combined within the same facility:
Components can therefore not only be painted but also welded, formed, machined and blasted within the same facility – subject to project requirements.
Industrial painting at Bock is applied where durable corrosion protection is required on large-format or heavy steel components:
Industrial painting is available as the final production step for complete assemblies – including counterweights and other heavy construction machinery components, as well as parts that have been welded, CNC-machined and shot-blasted within the same facility.
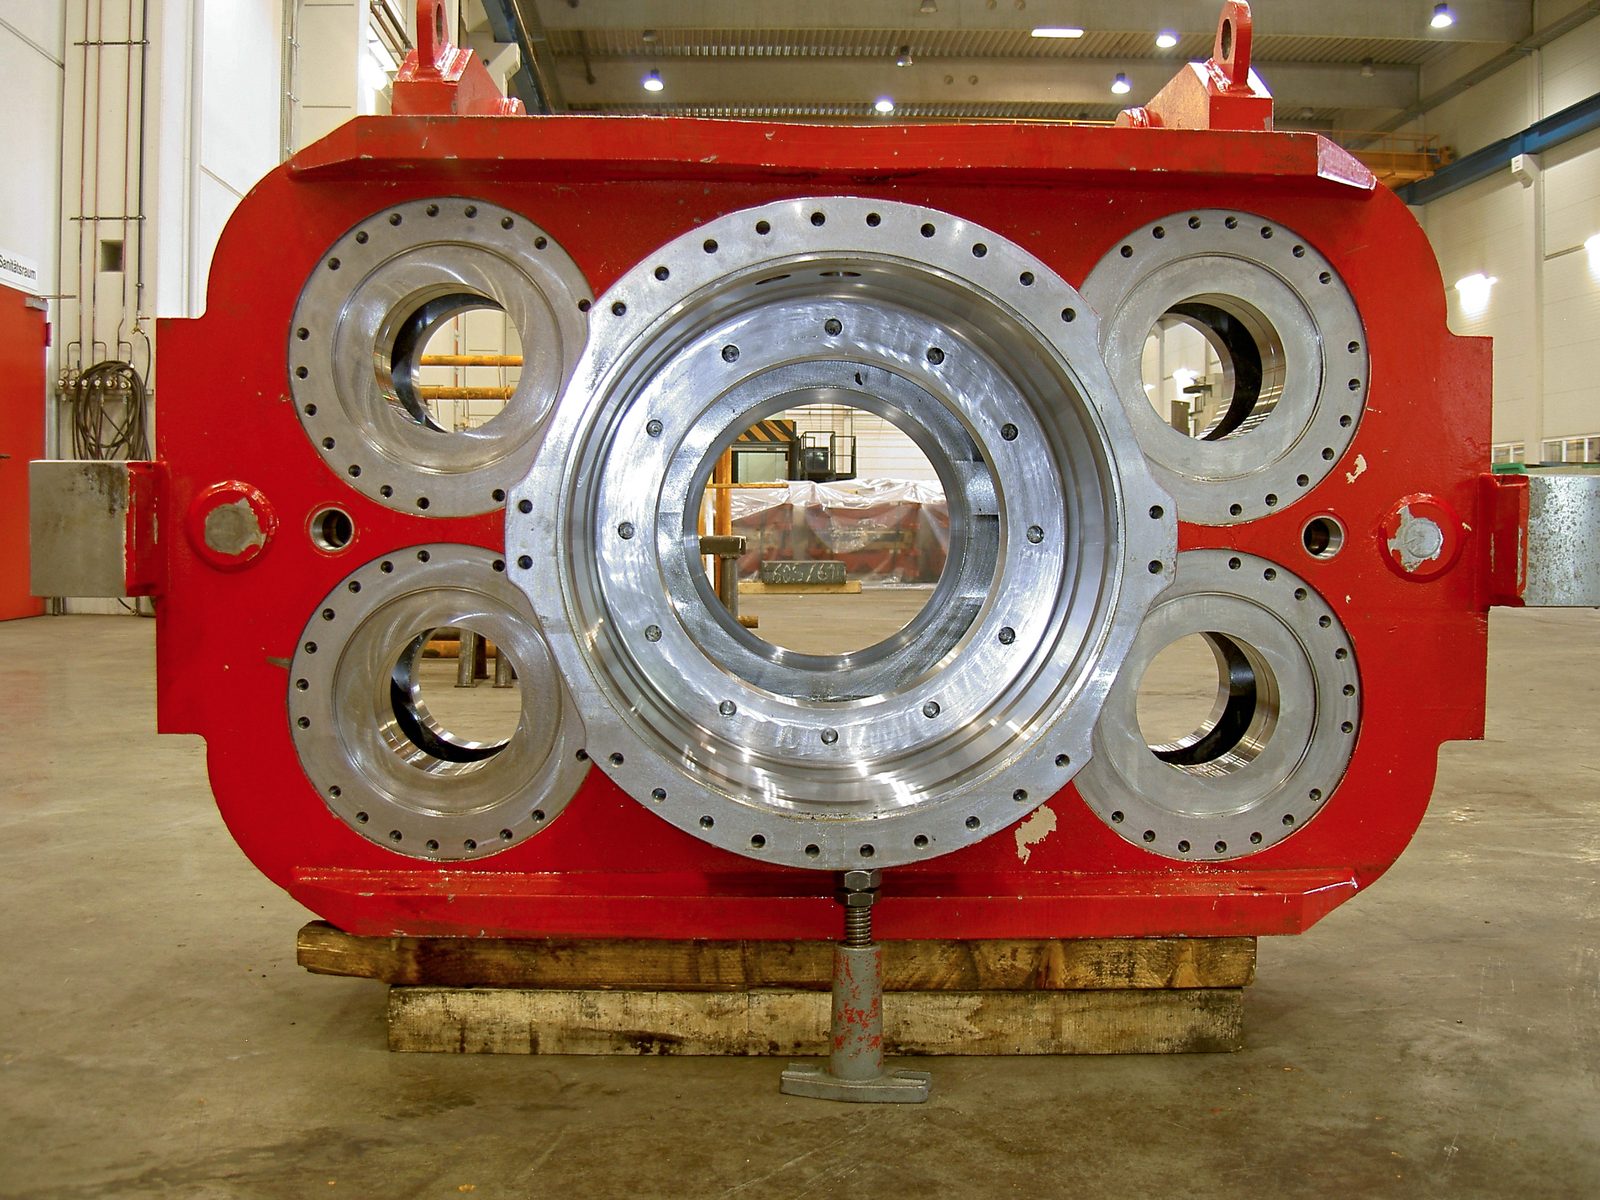
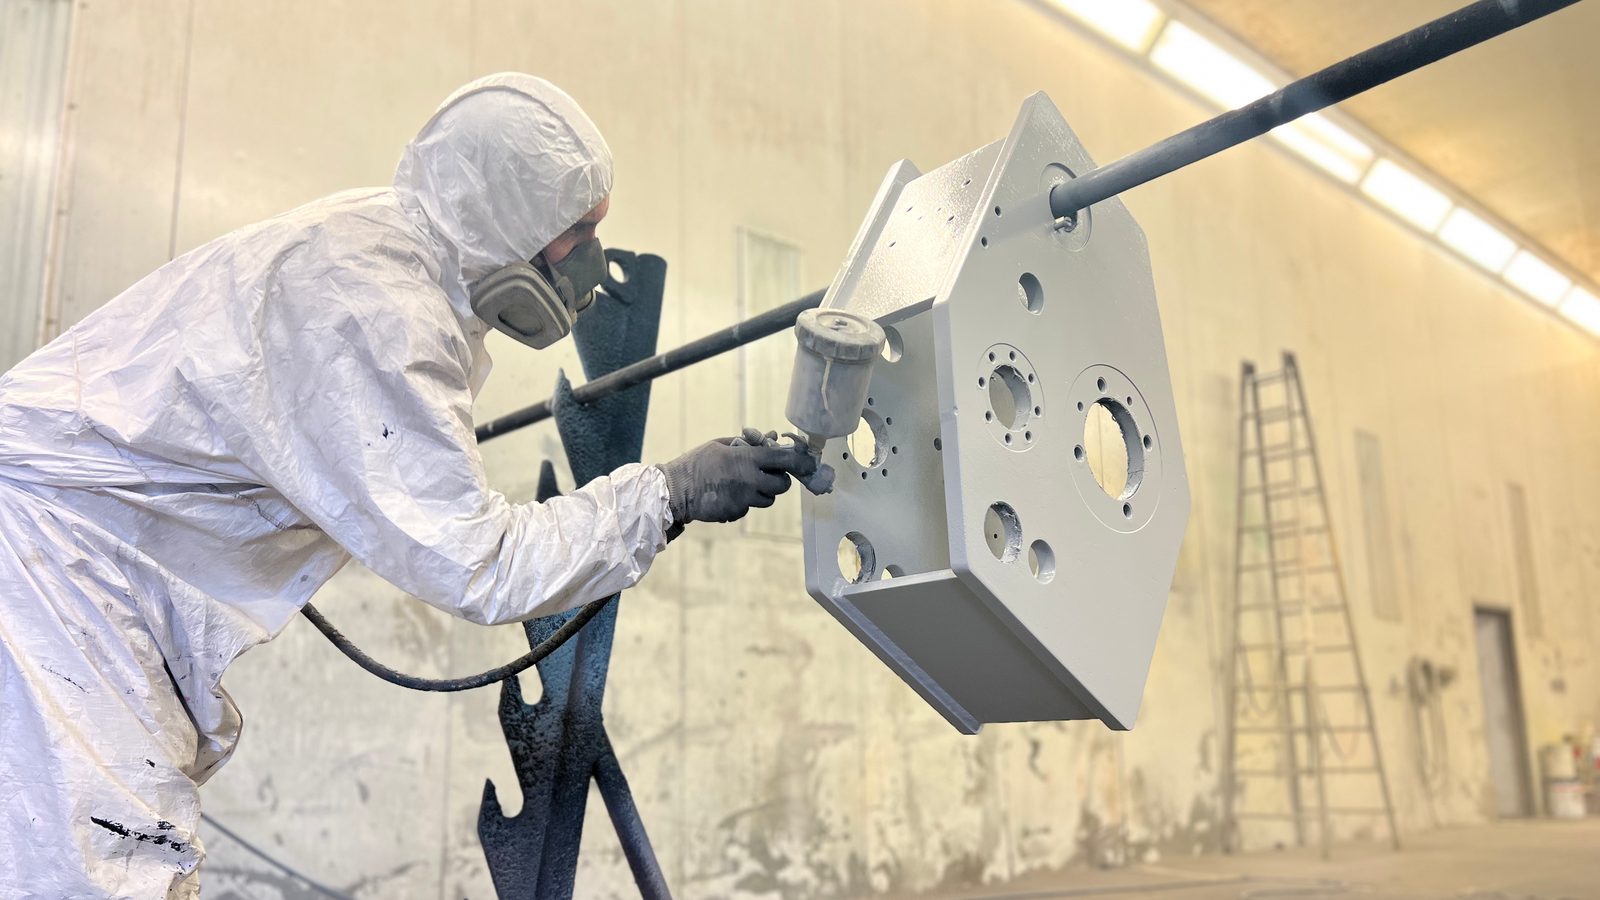
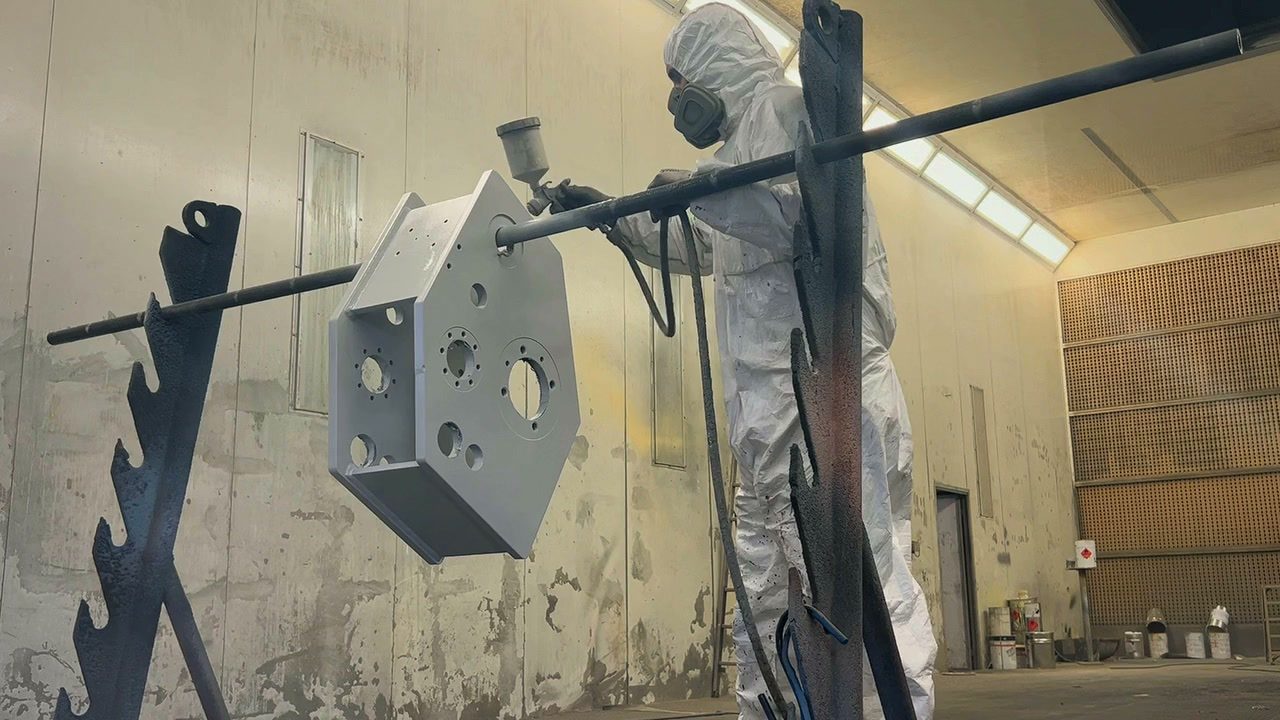
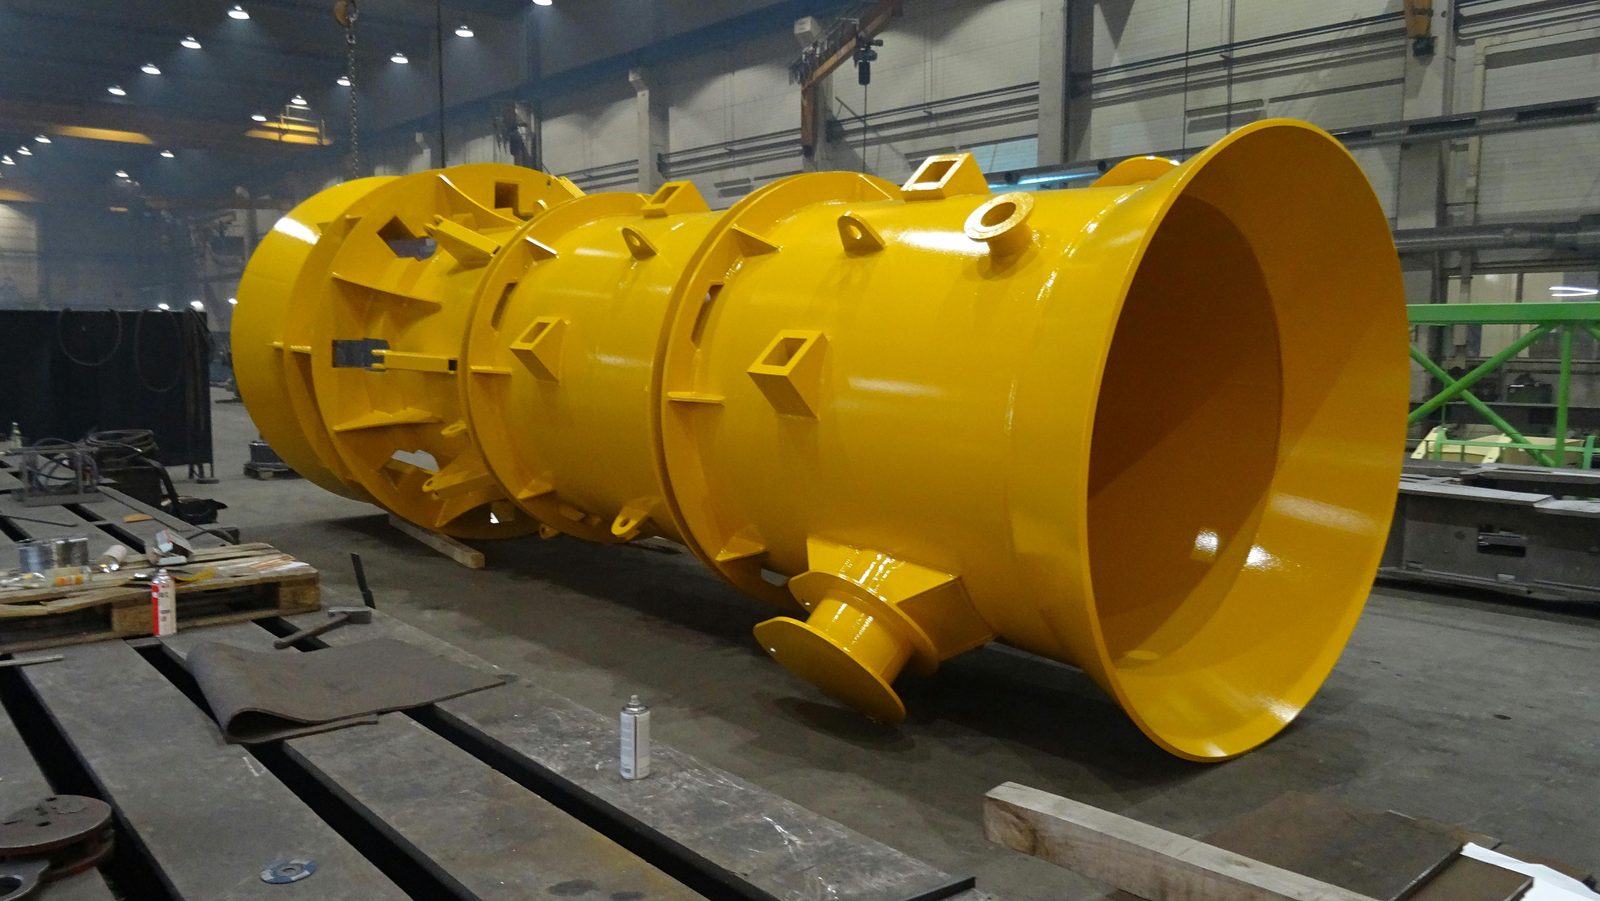
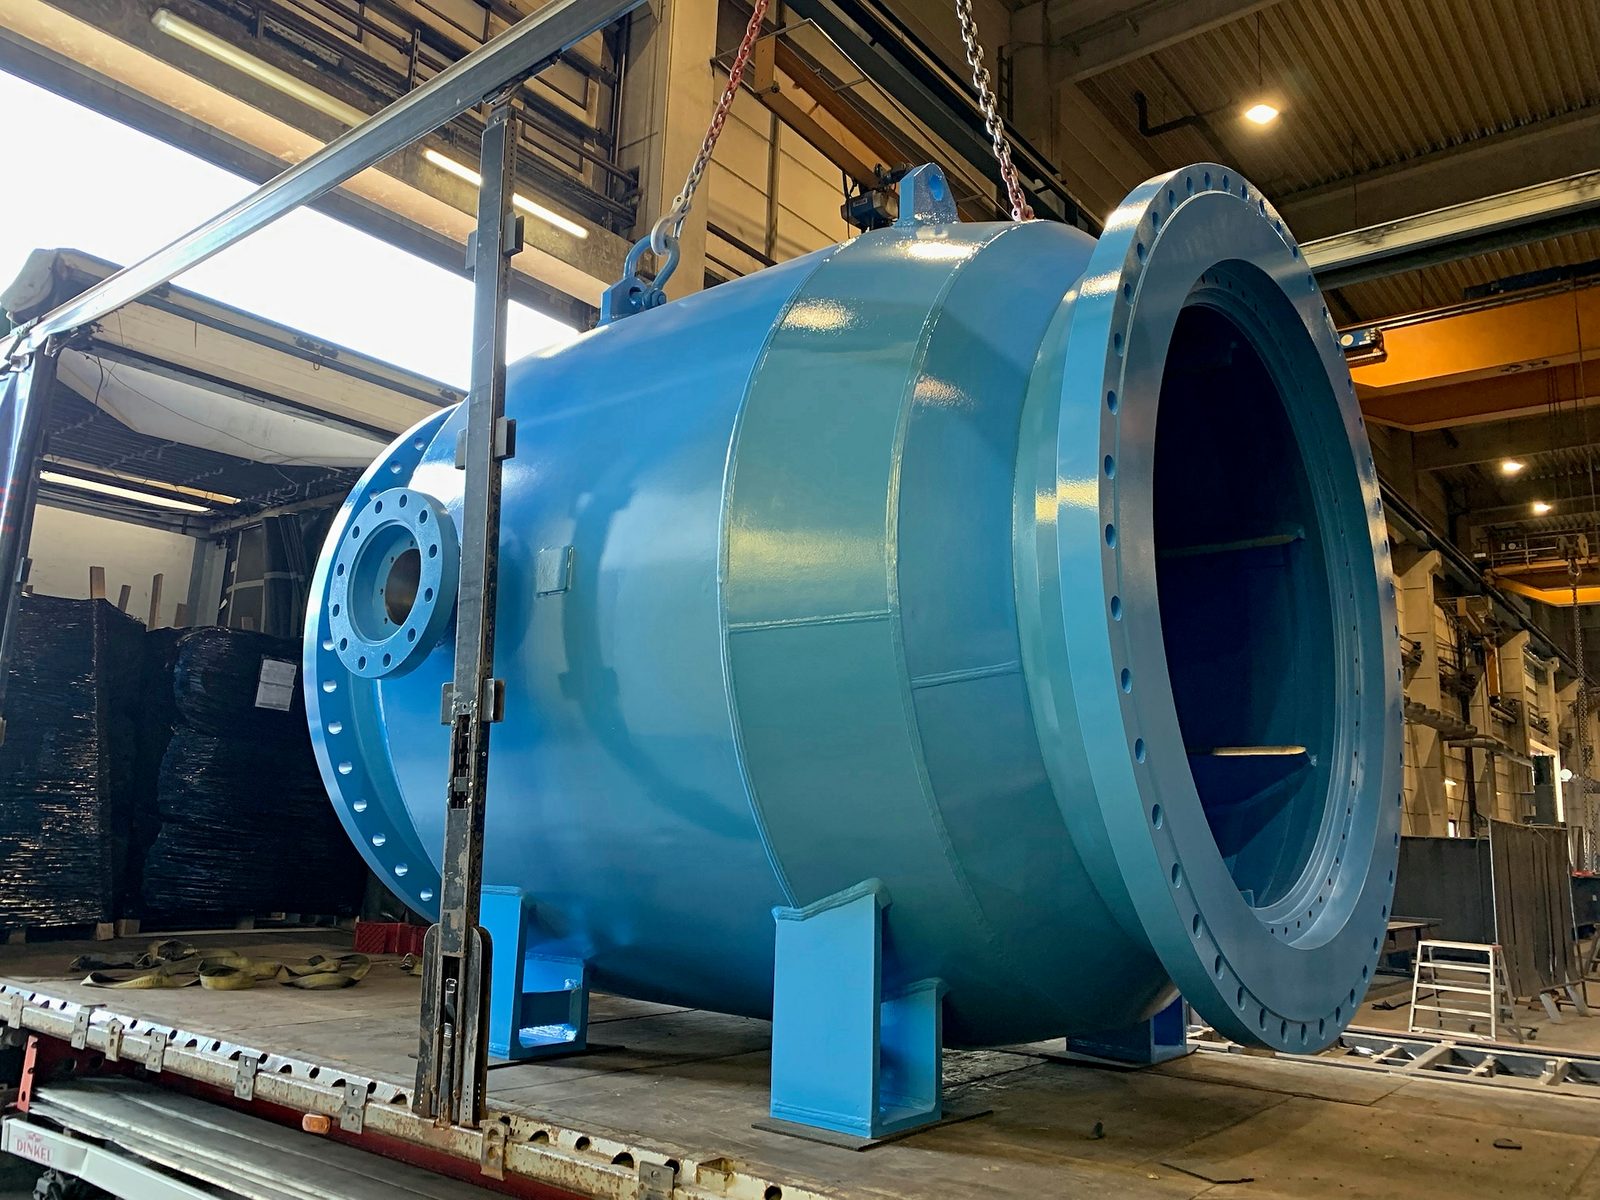
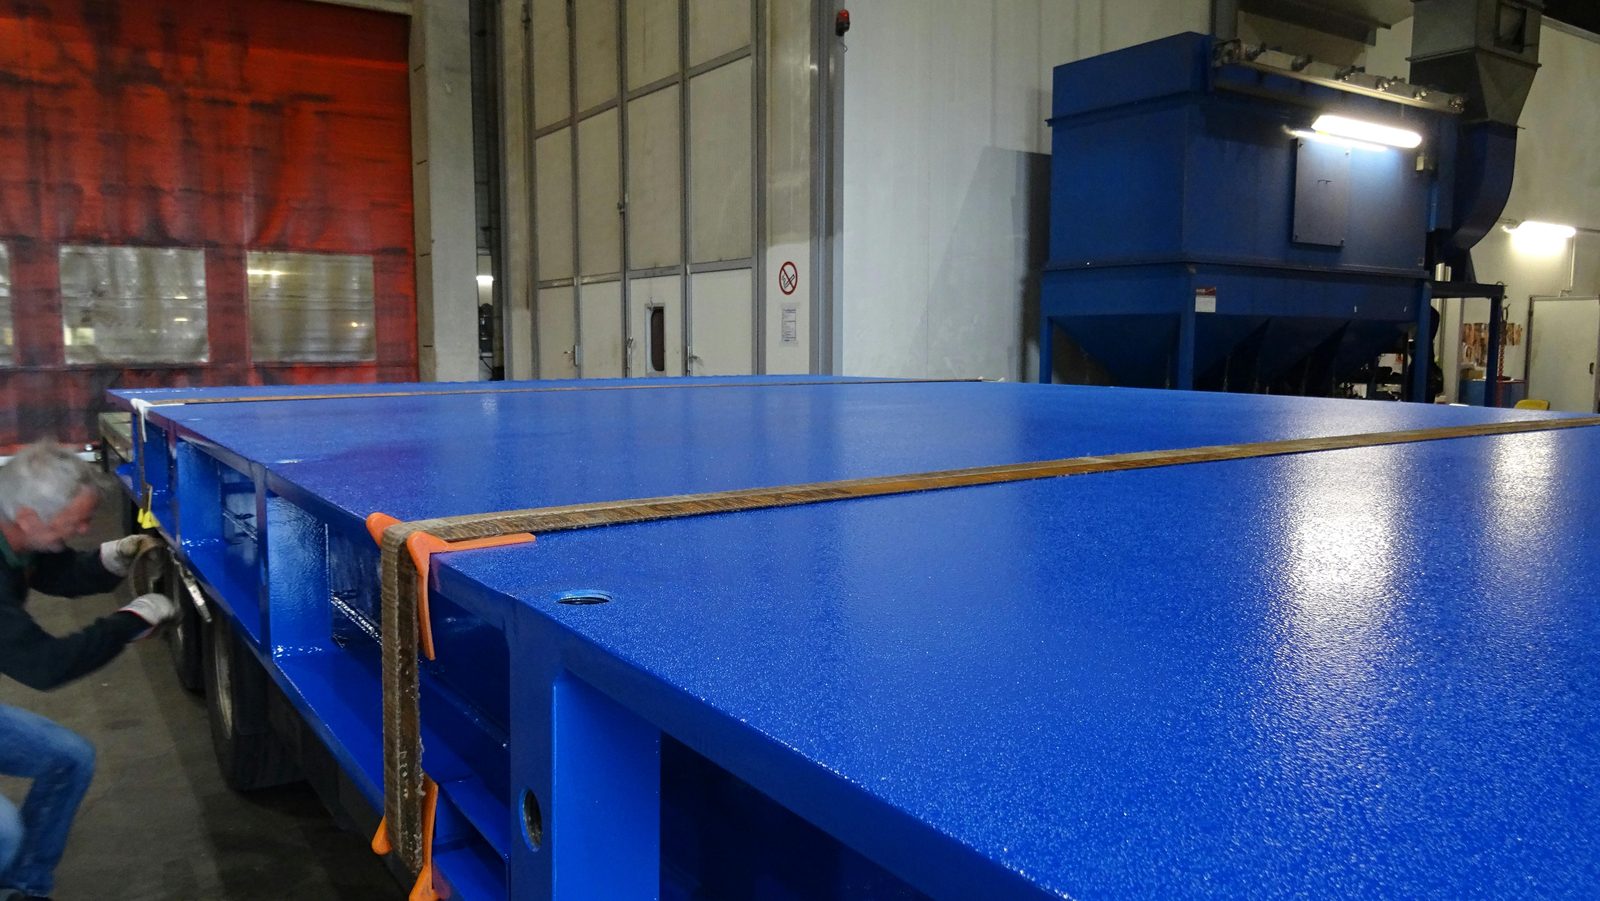
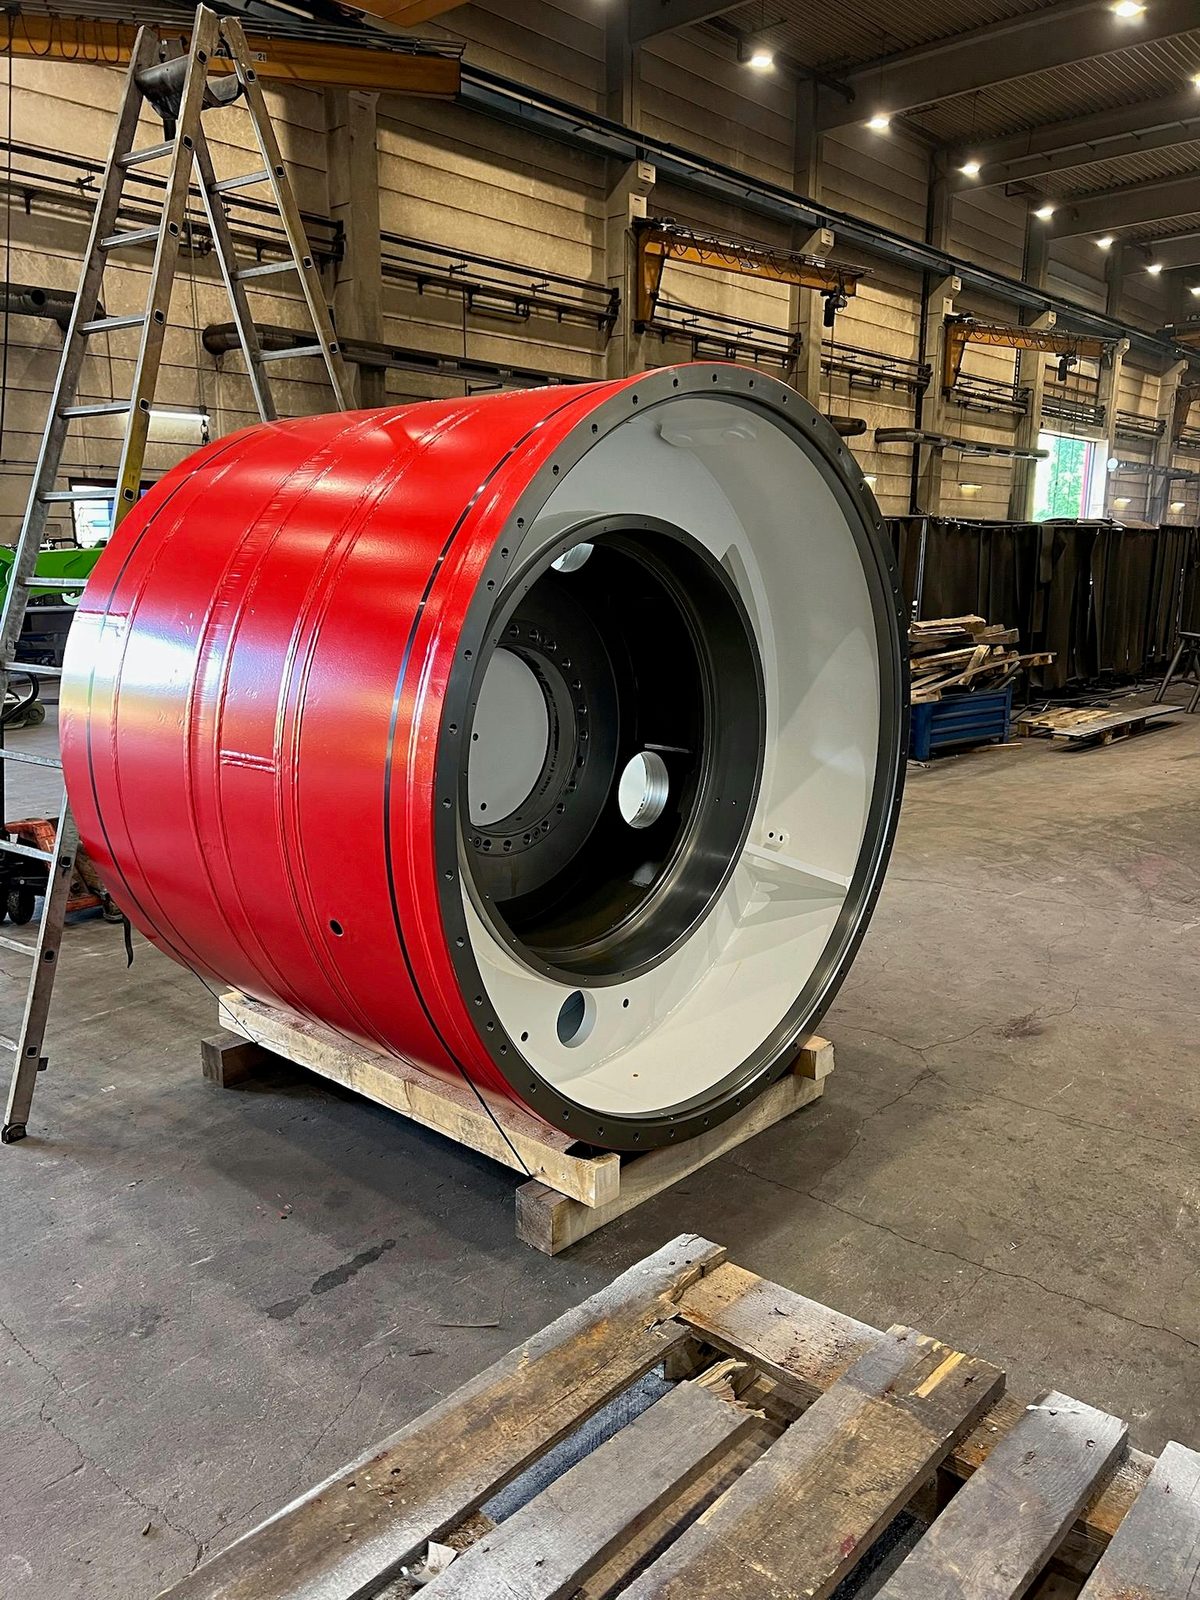
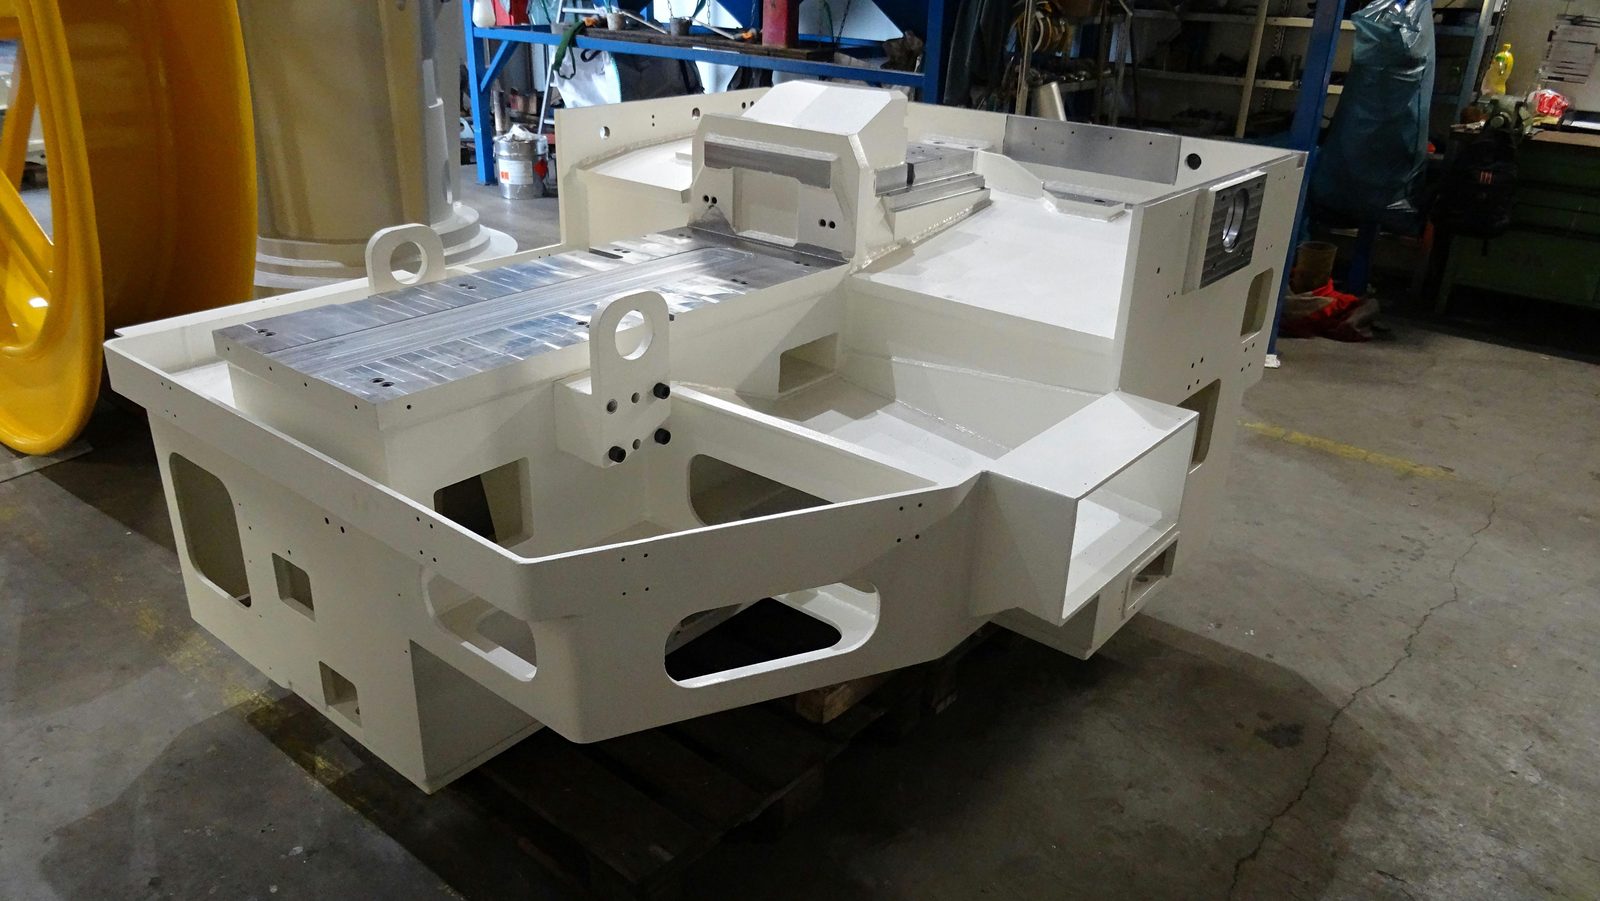
Our industrial painters at work in the paint booth. Real components from our paint shop in Lorch – from the heavy-plate welded structure in the large booth, through long machine frames and machined steel rings, to the fully assembled drum unit.
More from our production: Shot Blasting & Painting · 23 images
Bock Maschinenbau provides industrial painting in Lorch as part of an integrated production and corrosion protection process:
Plant, machine and vehicle builders from the Stuttgart area and the entire DACH region get blasting and painting to EN ISO 12944 from a single source in Lorch.
The spray booth for industrial painting at Bock has a usable interior of 25 × 7 × 6 m and accommodates heavy parts up to 50 t. Components are positioned via the 2×25 t crane system in the production hall and moved into the booth.
Industrial painting is carried out to EN ISO 12944 up to corrosivity category C5 with high durability (H). Coating system and corrosion protection class are agreed on a project basis according to drawing, normative requirements and customer specifications.
In the colour shade to RAL or customer specification and in the required gloss level, from matt and low-reflection to glossy. If the customer specifies a paint manufacturer, we paint with that manufacturer's coating materials. Anti-slip coatings with a rough surface are also possible for tread surfaces and loading areas.
Yes, in-house. The zinc is sprayed onto the previously blasted surface, and the component heats up only slightly in the process. The method is an option for components that would distort in a zinc bath or are too large for one.
By shot blasting to Sa 2.5 to ISO 8501-1 in a large-format blast chamber in the same plant; this is the usual surface preparation for corrosion protection coating systems to EN ISO 12944. Painting takes place immediately after blasting.
Painting covers structural steel (S235, S355), fine-grain and high-strength structural steel, Hardox after shot blasting and priming, as well as machine components, housings and cast components, vessels and large-format special structures. Further materials and component types are painted by agreement.
Coating build-up, preparation grade and coating requirements are defined according to drawing, normative requirements and customer specifications and documented in the quality management system to DIN EN ISO 9001:2015. For components from welded assemblies to DIN EN 1090-2 EXC3, painting can be embedded within the quality framework of welding production; inspection and documentation requirements are defined on a project basis.
At the Lorch site, in the same plant as shot blasting, welding, press brake bending and CNC machining. Blasting and painting to EN ISO 12944 therefore take place without transport between two companies.
For an initial assessment, please provide component dimensions, material, weight, required corrosion protection category to EN ISO 12944, colour shade and any requirements for coating build-up or documentation. We will prepare a project-specific quotation.