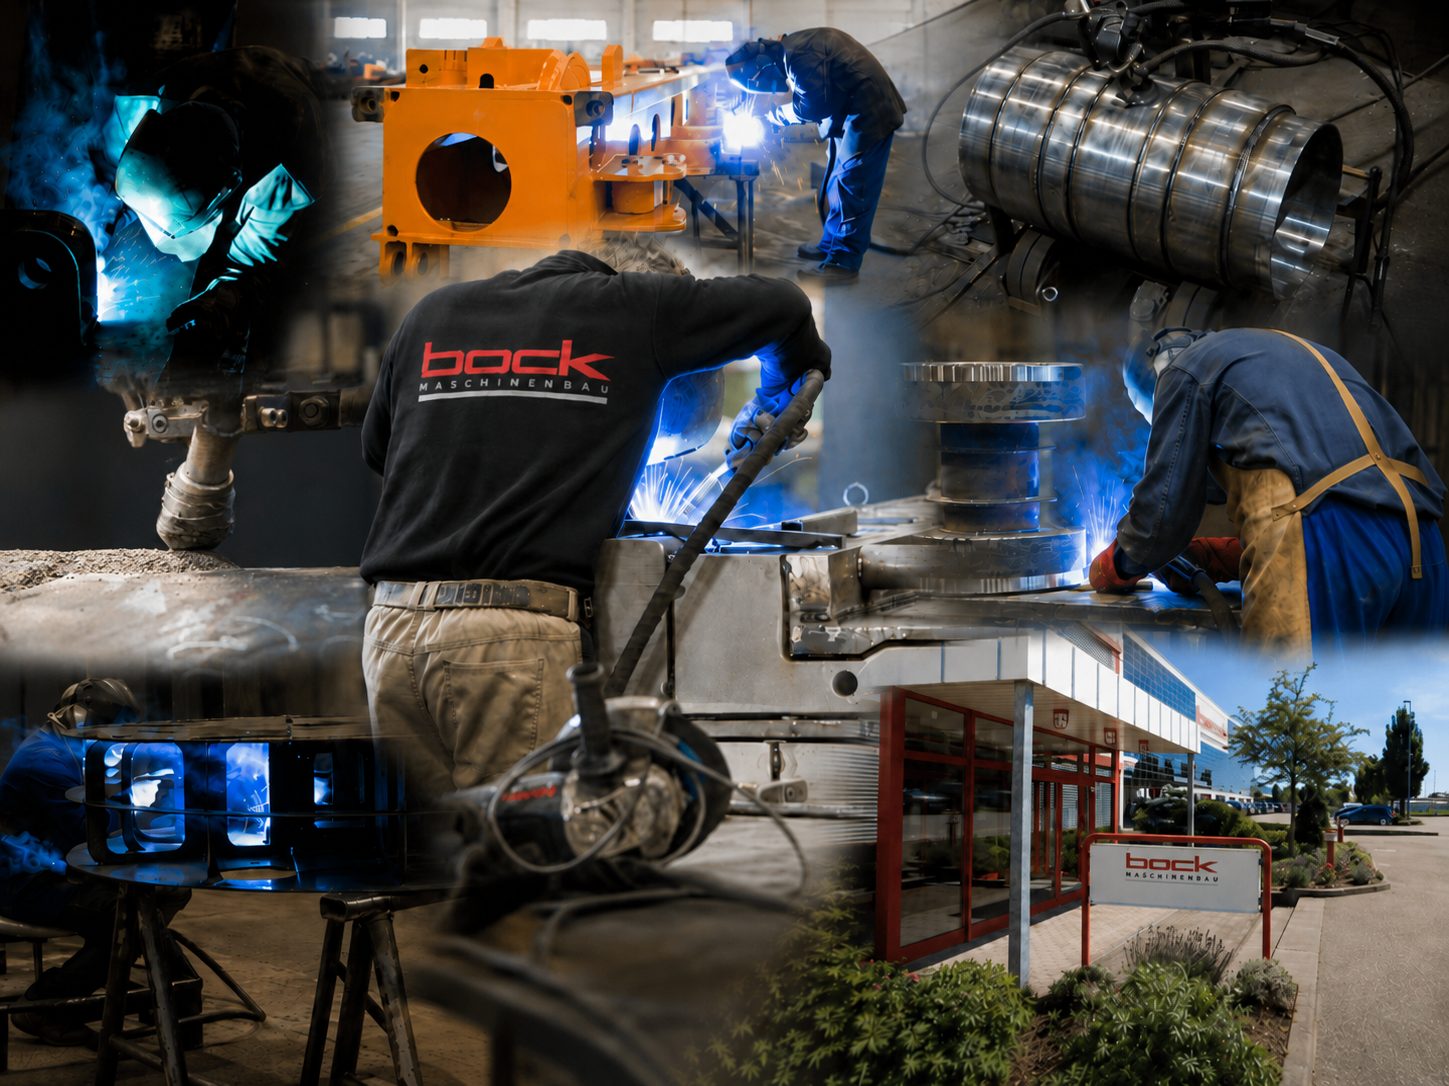
Production Gallery – Machinery & Manufacturing
Images from our operations: CNC machining, welding, heavy parts and more.
Manufacturing on approx. 14,000 m²
Across approx. 14,000 m² of production space we manufacture steel assemblies, special-purpose machinery and heavy parts up to 50 t. The following images give an overview of our machinery, manufacturing processes and typical workpieces from projects in crane engineering, vehicle construction, plant engineering and specialist civil engineering. All work shown was carried out at our plant in Lorch, Baden-Württemberg, Germany.
Facilities & Operations
The Lorch plant: production halls, material storage and workstations on 14,000 m². Cutting, welding, machining and surface treatment are under one roof; between production steps, a component never leaves the plant.
Milling & Boring
Gantry milling machines with up to 26 m of travel, a boring mill and a travelling-column machining centre at work on welded assemblies, machine beds and castings. The pictures show large parts in their setups.
Turning
Vertical turning up to Ø 4,800 mm and 25 t table load: rings, flanges, hubs, housings and rolled pipe sections. The pictures show the vertical lathe and large parts in their setups, plus a conventional lathe.
Welding
MAG, TIG and submerged arc welding on machine frames, cylindrical components and large assemblies. For long, heavy seams, the submerged arc system welds with up to 1,250 A.
Cutting
Oxy-fuel cutting up to 200 mm plate thickness on 20 × 3.5 m, plus plasma cutting above and under water with bevel cuts. In the plant, almost every assembly starts with cutting.
Forming
Press braking with up to 1,000 t of pressing force and shearing of heavy plate. Plate rolling turns sheets up to 3,050 mm wide and 120 mm thick into pipes, cones and rings up to Ø 8,000 mm.
Heavy Parts & Projects
Welded structures, machine frames and assembled units up to 50 t unit weight — manufactured, inspected and coated in Lorch, some shown on the low-loader before delivery.
Shot Blasting & Painting
Blasting to Sa 2.5 and industrial painting to EN ISO 12944 in a 25 × 7 × 6 m booth. The pictures show large parts before, during and after coating.
Quality & Inspection
Non-destructive testing of welds in the plant, above all dye penetrant testing (PT) on welded assemblies and large components.
Vibration Stress Relief
Vibration stress relief on welded structures and machine frames: unbalance motor, sensors and measuring device in place. The process reduces residual stresses without putting the component into an annealing furnace — important for parts that are machined to tolerance afterwards.
Interested in working together?
Our machinery and manufacturing capacity are available for demanding contract manufacturing orders.