DIN EN 1090-2 EXC3
Certified welding contractor for load-bearing steel structures – qualified up to Execution Class EXC3.
DVS ZERT · Zertifizierungsstelle des DVS download as PDFCutting, welding, machining, surface finishing — the complete production under one roof in Lorch. Steel structures and large parts up to 50 t, CNC large-part machining up to 26 m part length, certified to EN 1090-2 EXC3.
Cutting, forming, certified welding, stress relief, large-part CNC machining, surface finishing and assembly — every step at one location, for single parts and series up to 50 tonnes. We process several thousand tonnes of steel a year. Follow your component's path through our plant below.
Structural steel, high-strength fine-grain steel up to S1100, Hardox & wear-resistant steels, austenitic stainless steel, duplex and pressure-vessel steel — predominantly European quality steels, with a 3.1 inspection certificate to EN 10204, from our own stock and cut to size.
View all processed materials
One plant · every production step in-house


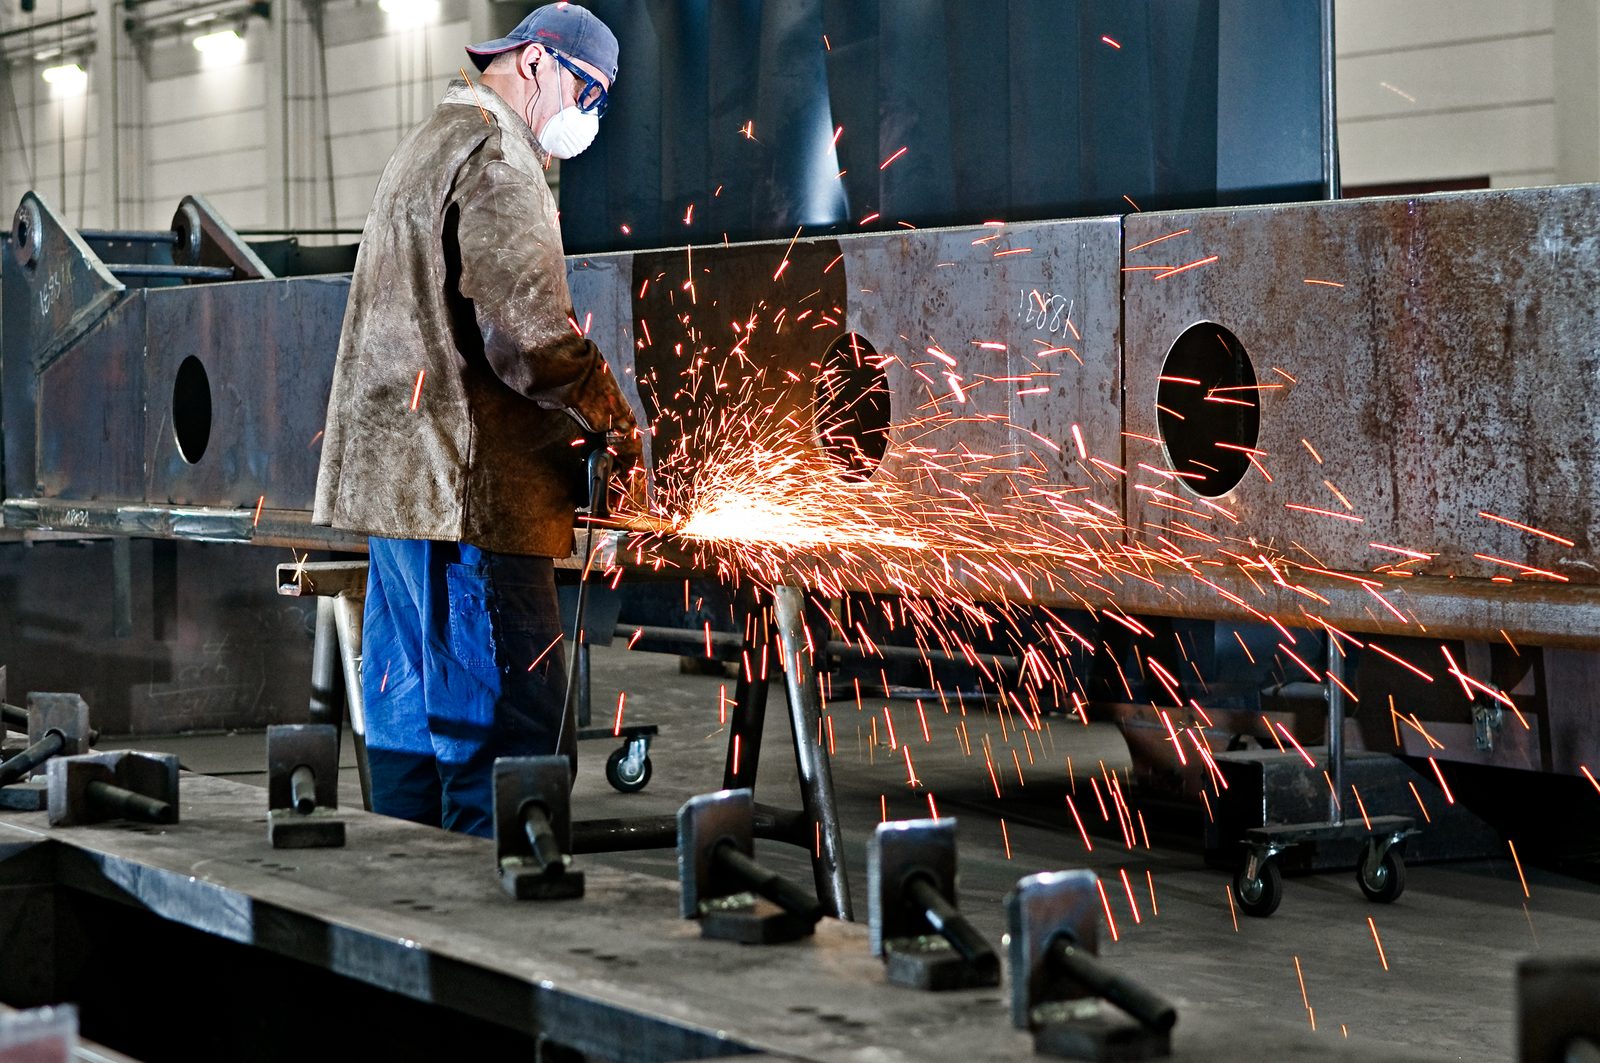
From raw steel to the exact contour — oxy-fuel flame cutting and CNC plasma on a 20-metre format, saw cutting from our own material stock, and for tubes & hollow sections 3D plasma and oxy-fuel tube cutting reaching where the tube laser gives up. Plate and tube alike — all on site.
Plate up to 200 mm · tube up to 50 mm · 20,000 × 3,500 mm · bevels ±45°

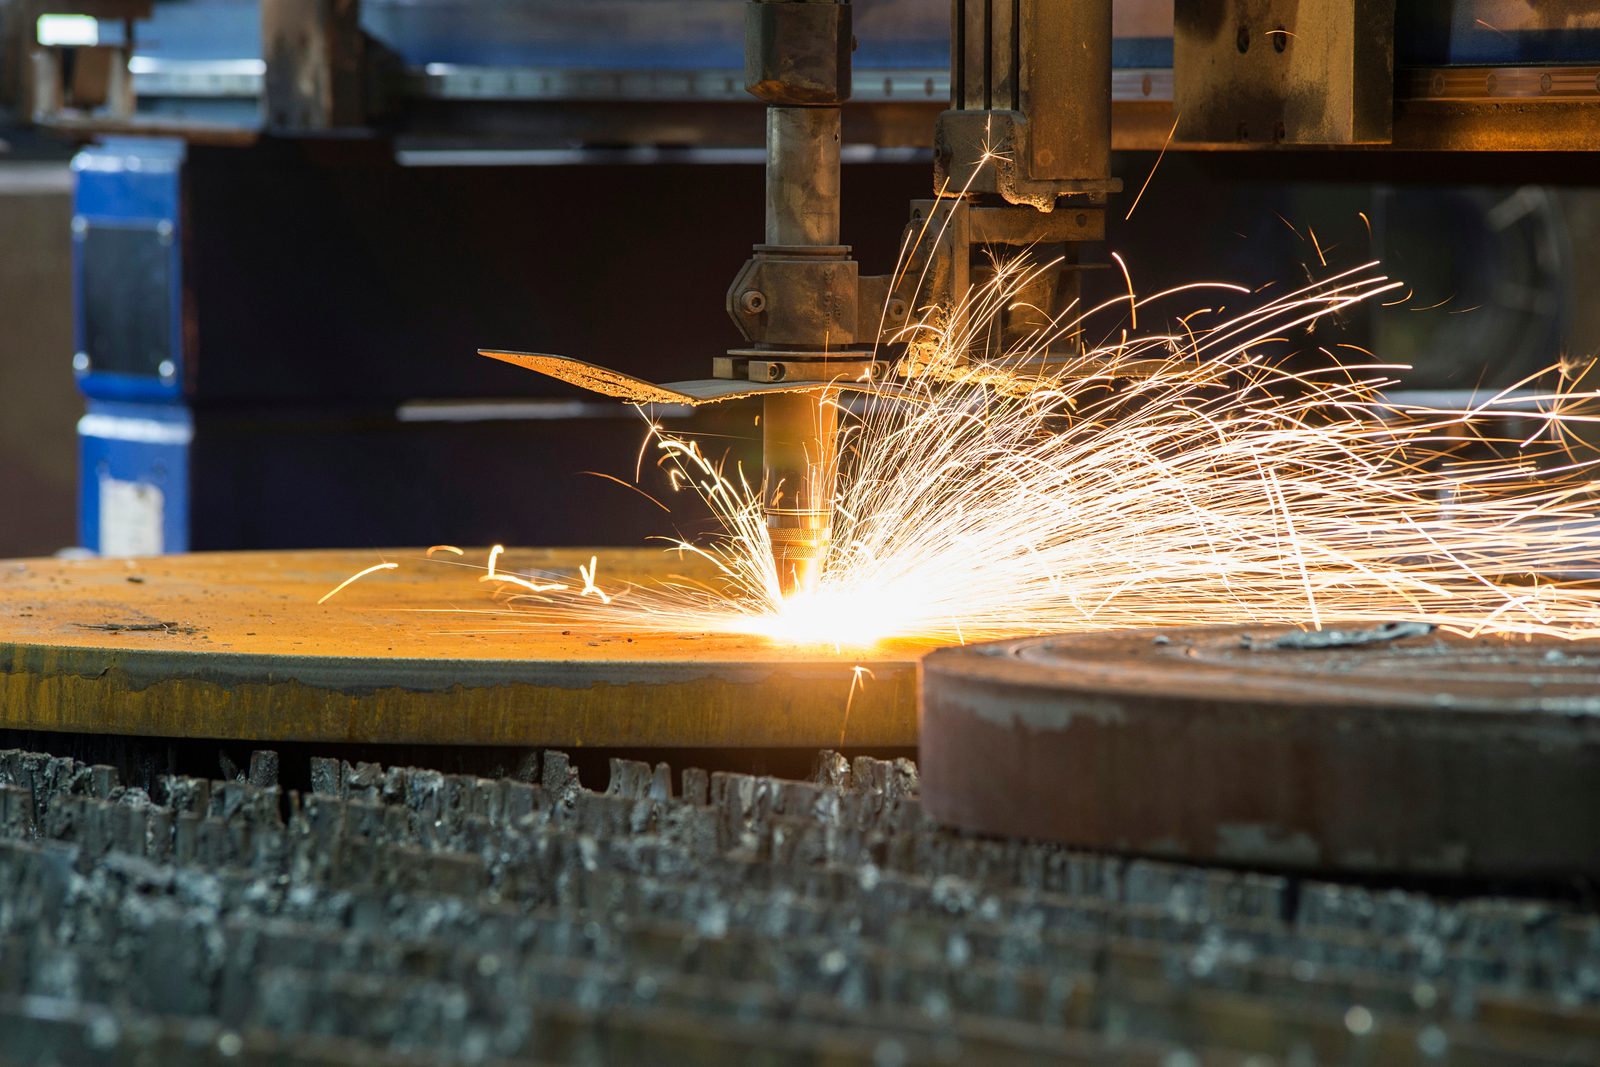
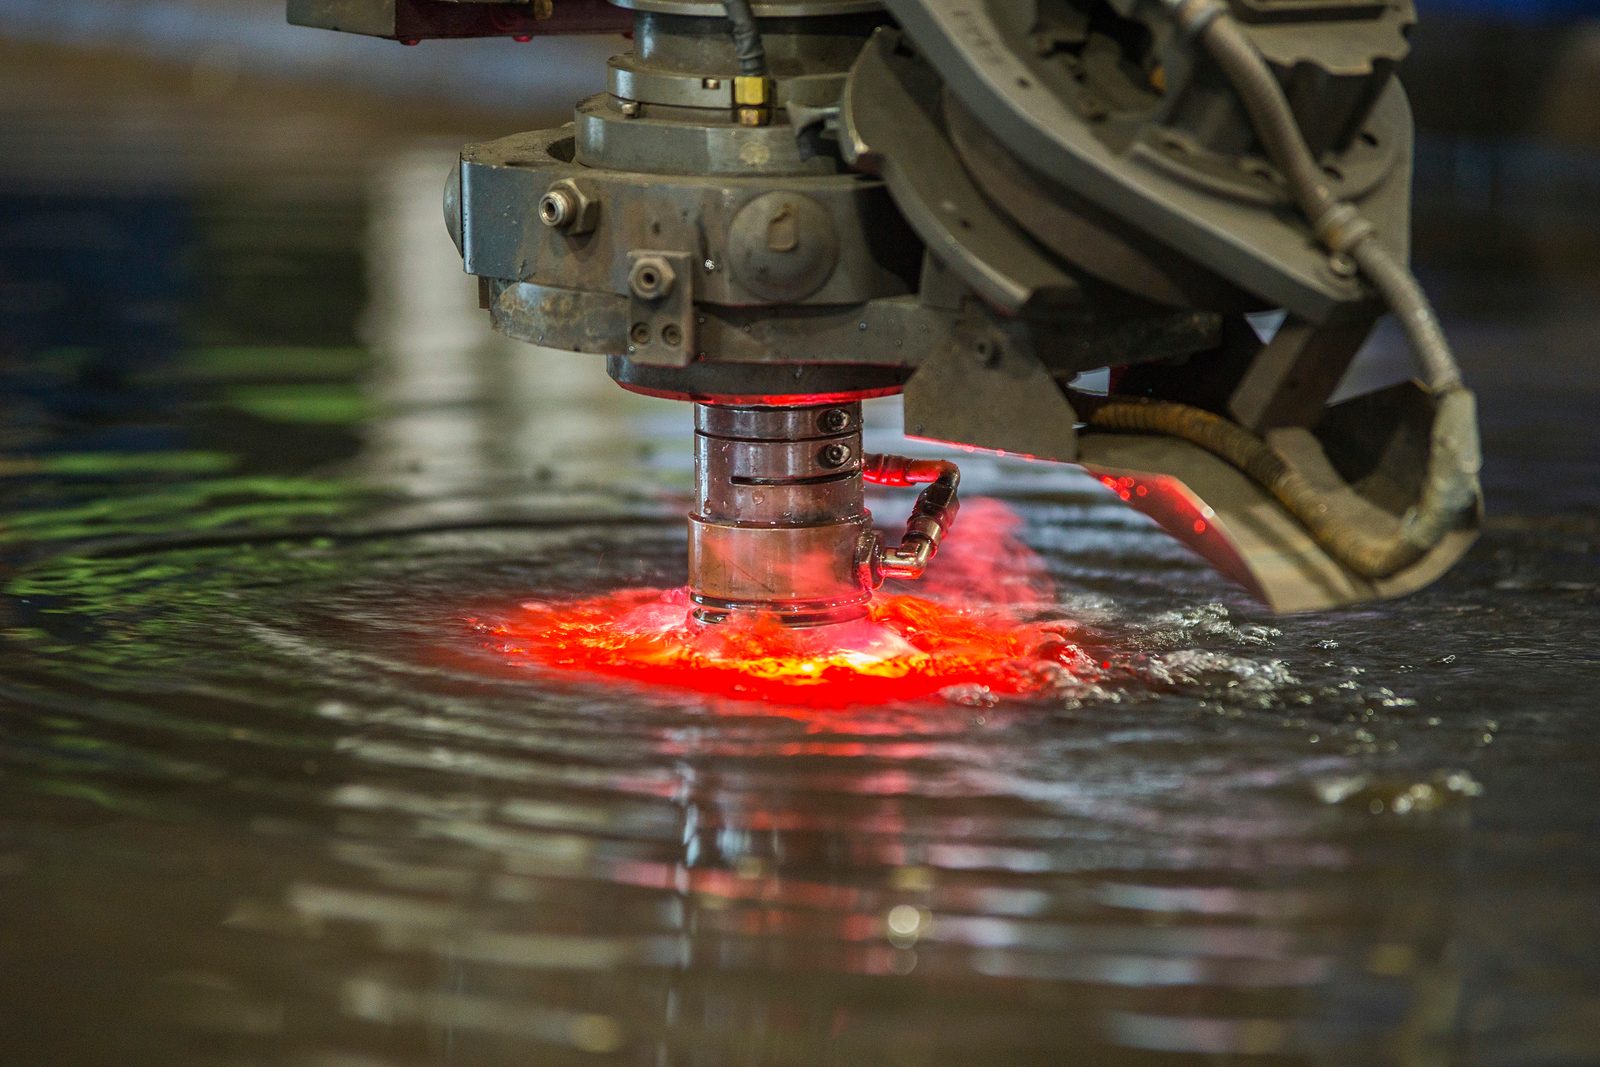
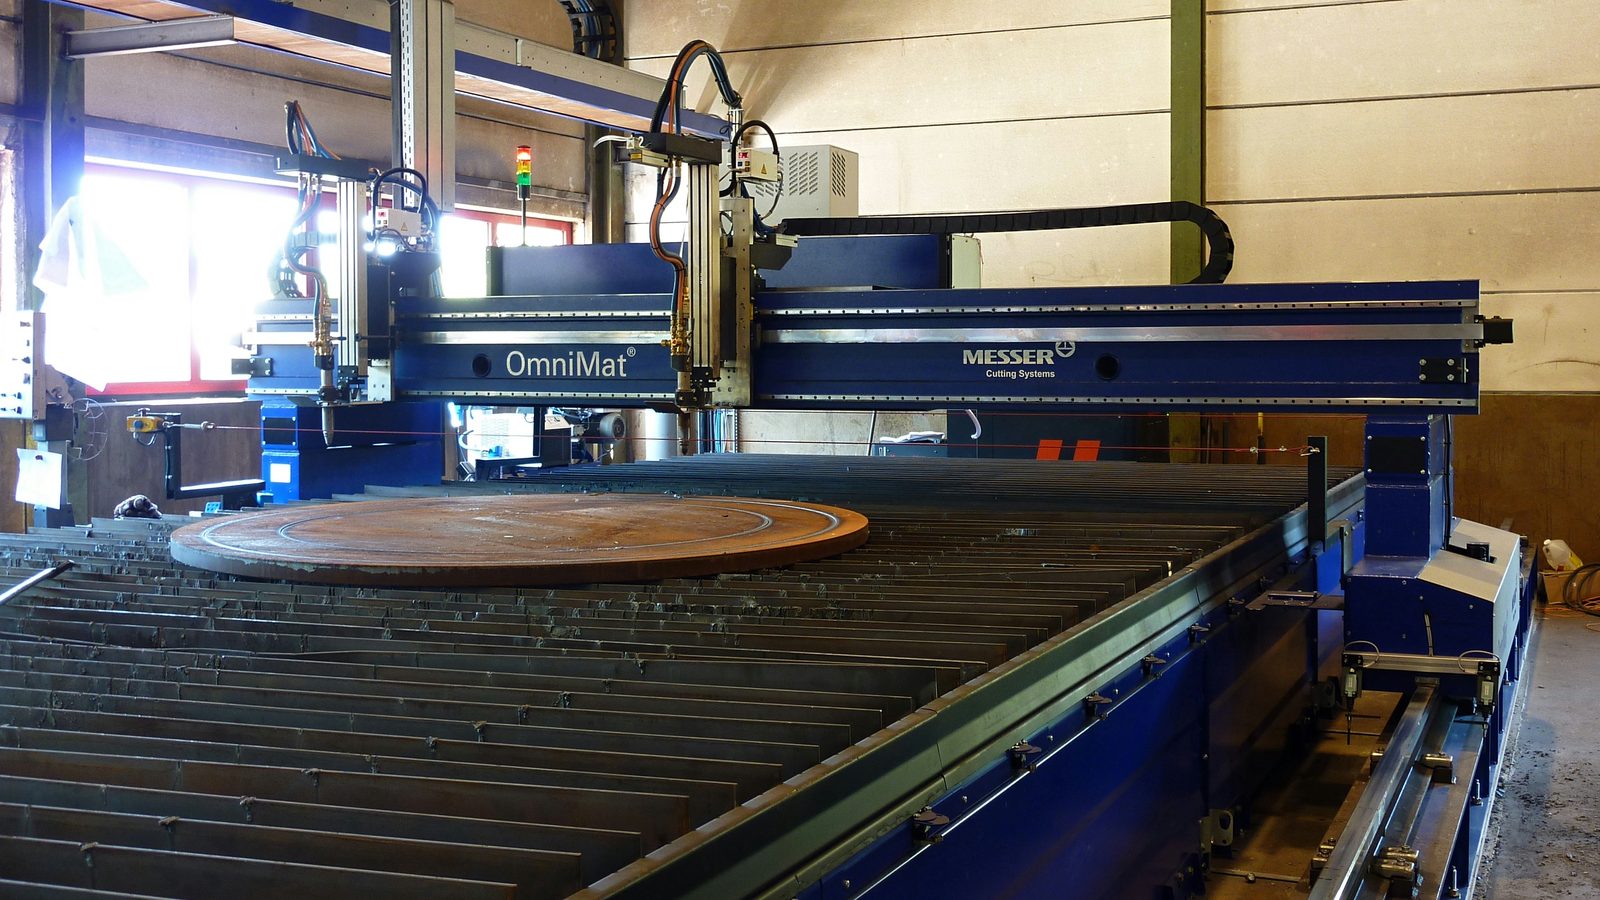
CNC oxy-fuel flame cutting on a 20 × 3.5 m format — steel and Hardox up to extreme wall thicknesses, with automatic bevel cutting.

High-precision plasma cutting on a large format — including automatic bevel tilt ±45°, steel, stainless steel and Hardox.

Automatic saw cutting of tubes, profiles, girders and round stock to size — straight from our own material stock, fast and economical.

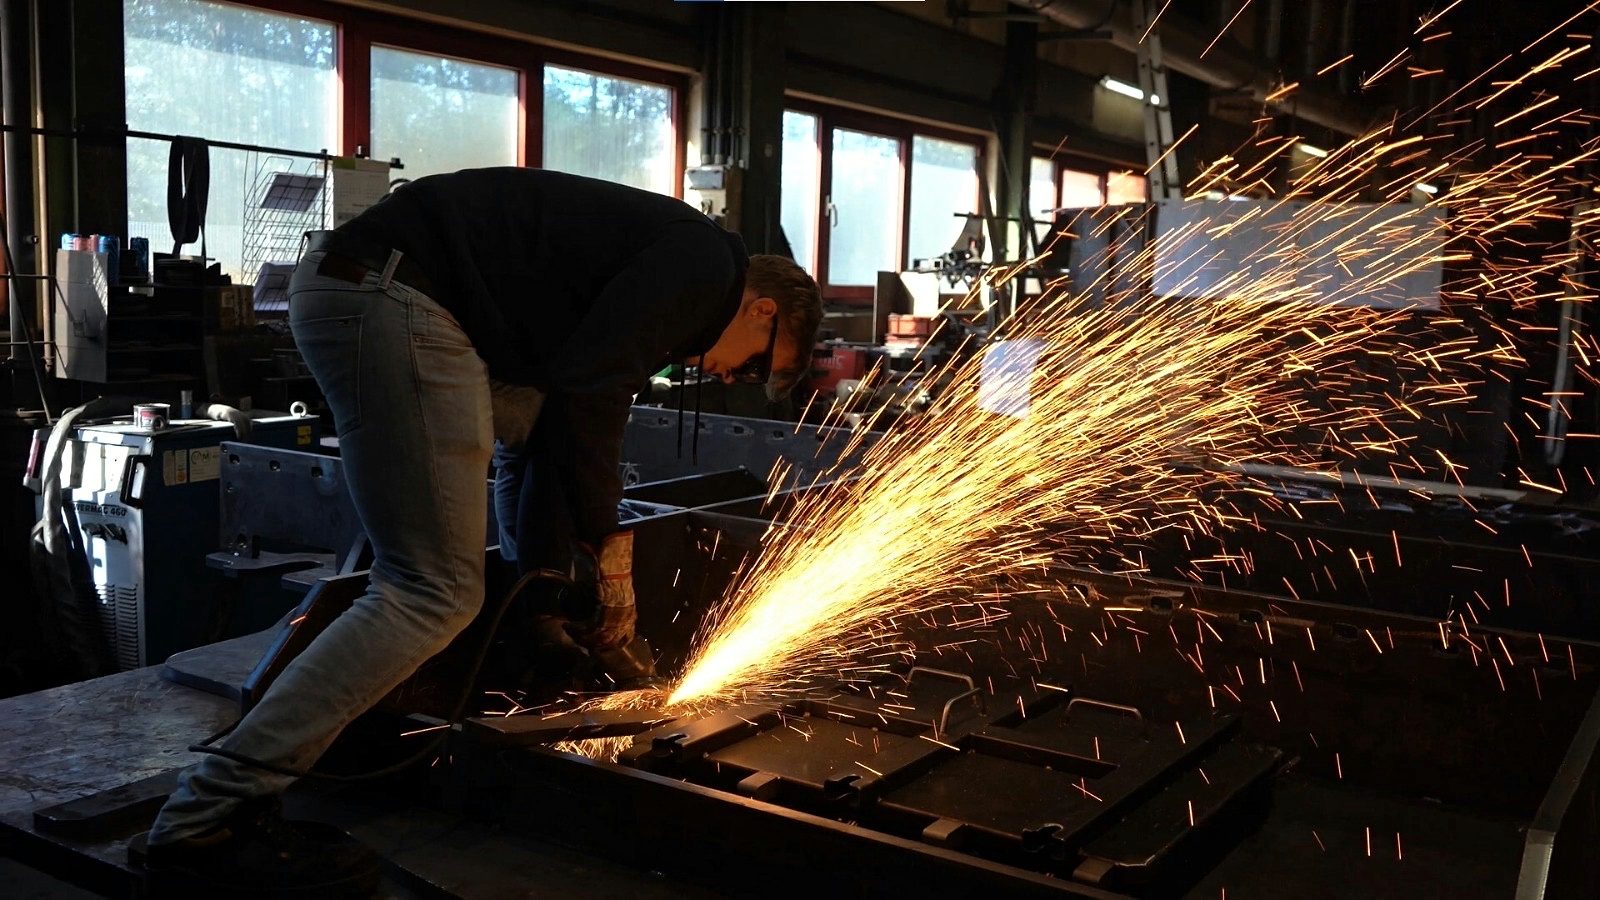
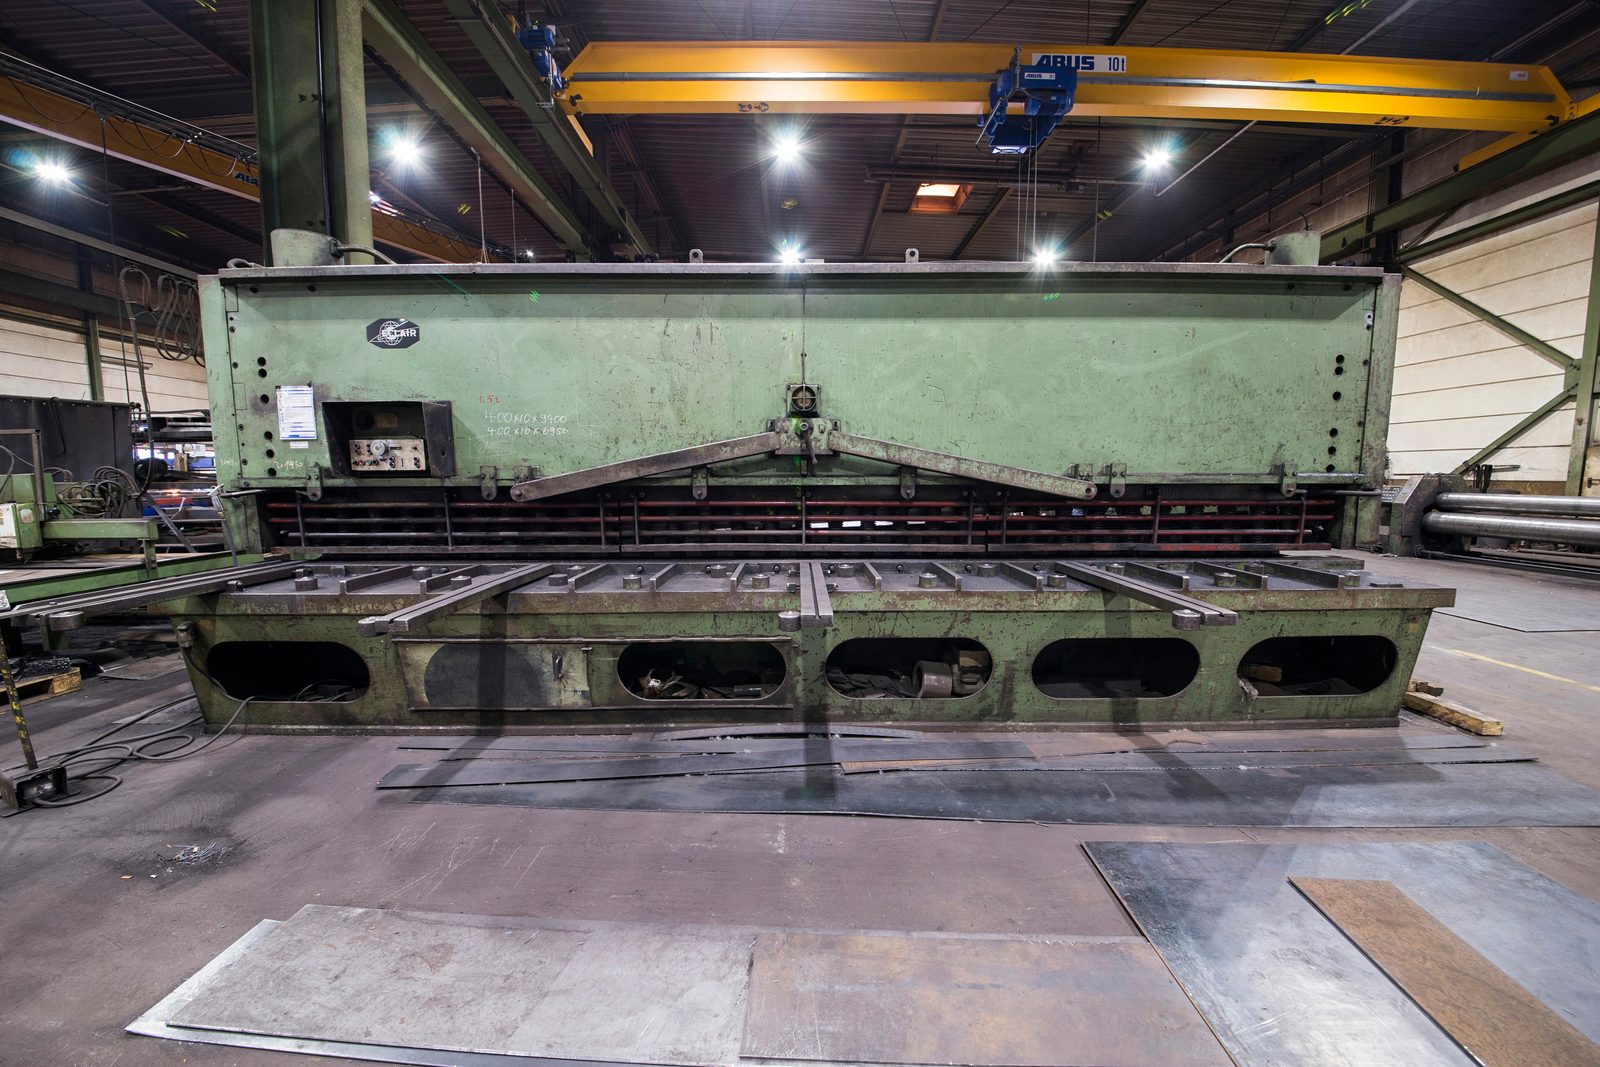
Mechanical plate cutting on the guillotine shear — heat-free and distortion-free, a clean edge on plate up to 15 mm on lengths up to 6,100 mm.
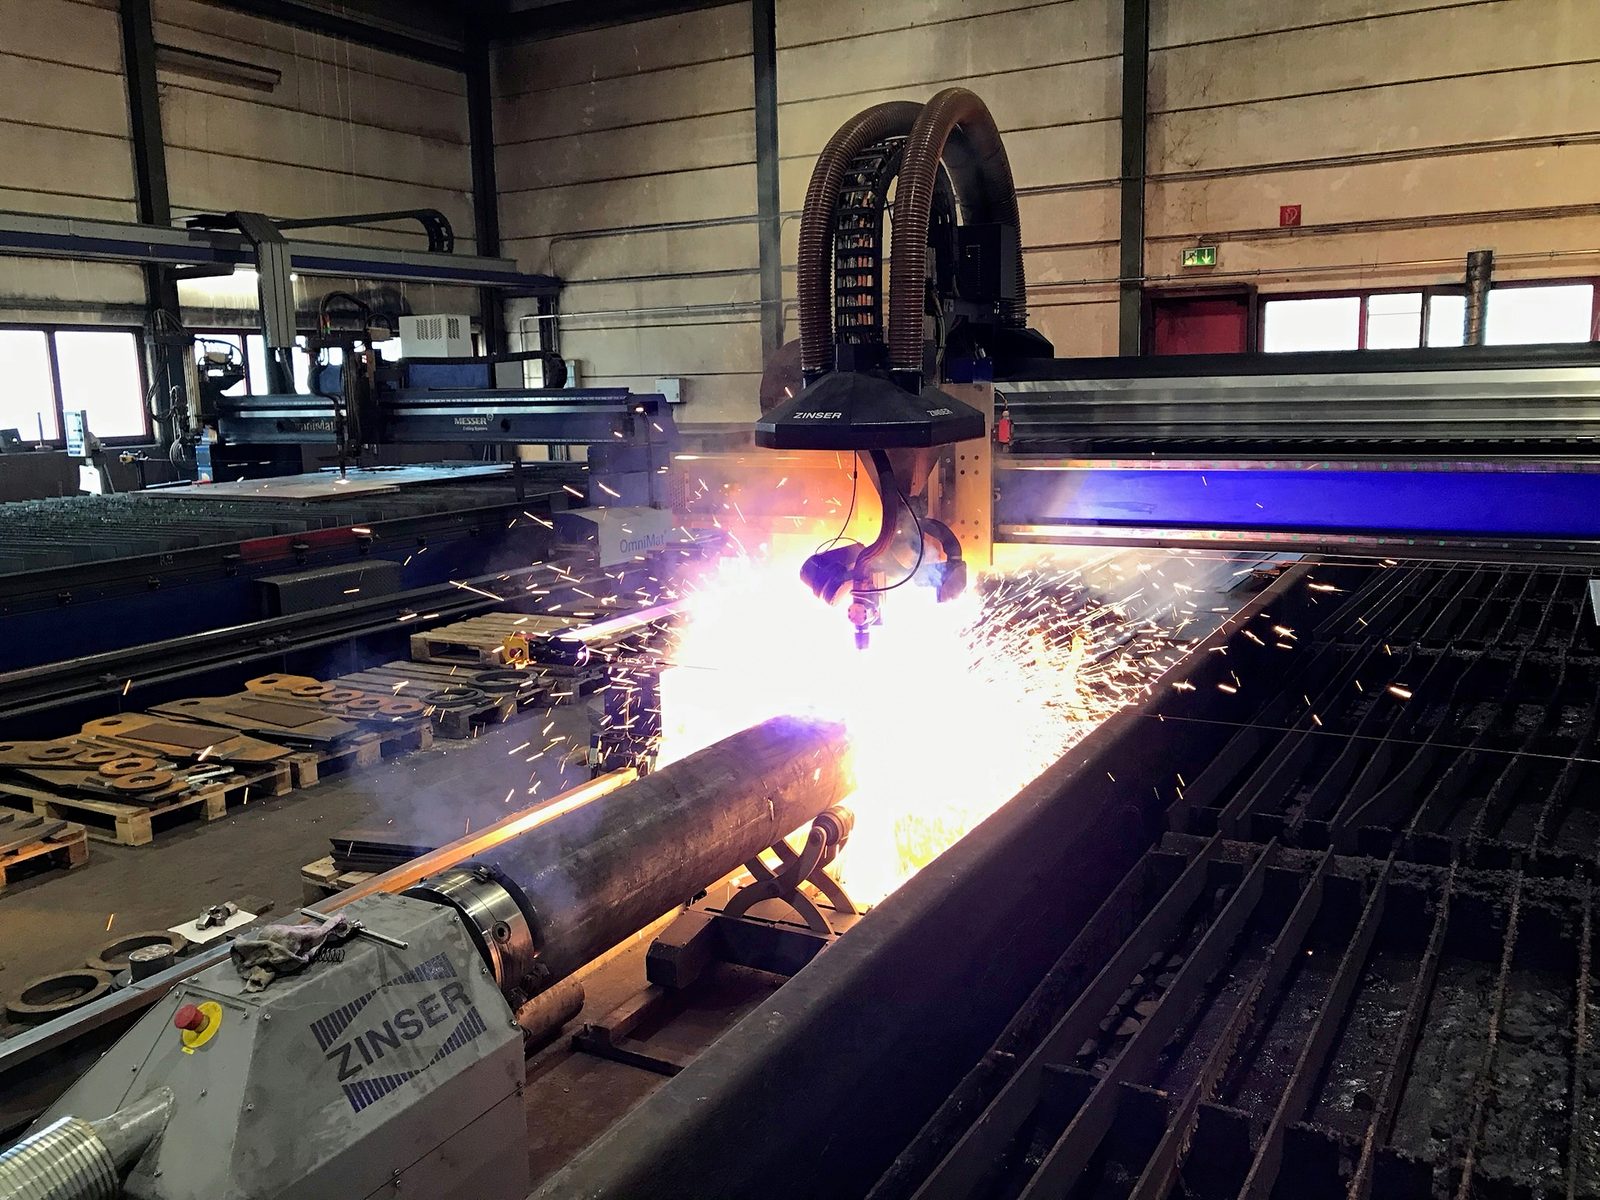
CNC tube machining for tubes, hollow sections and round stock — both cutting processes under one roof: 3D plasma tube cutting for contours, cope cuts and mitre cuts up to 30 mm wall thickness in structural steel, stainless steel, fine-grain steel and wear-resistant steel (Hardox); oxy-fuel tube cutting for solid steel up to 50 mm — structural steel, high-strength fine-grain steel (S460–S1100) and wear-resistant steel. Exactly where tube lasers reach their limits: no outsourcing, all at the Lorch location.

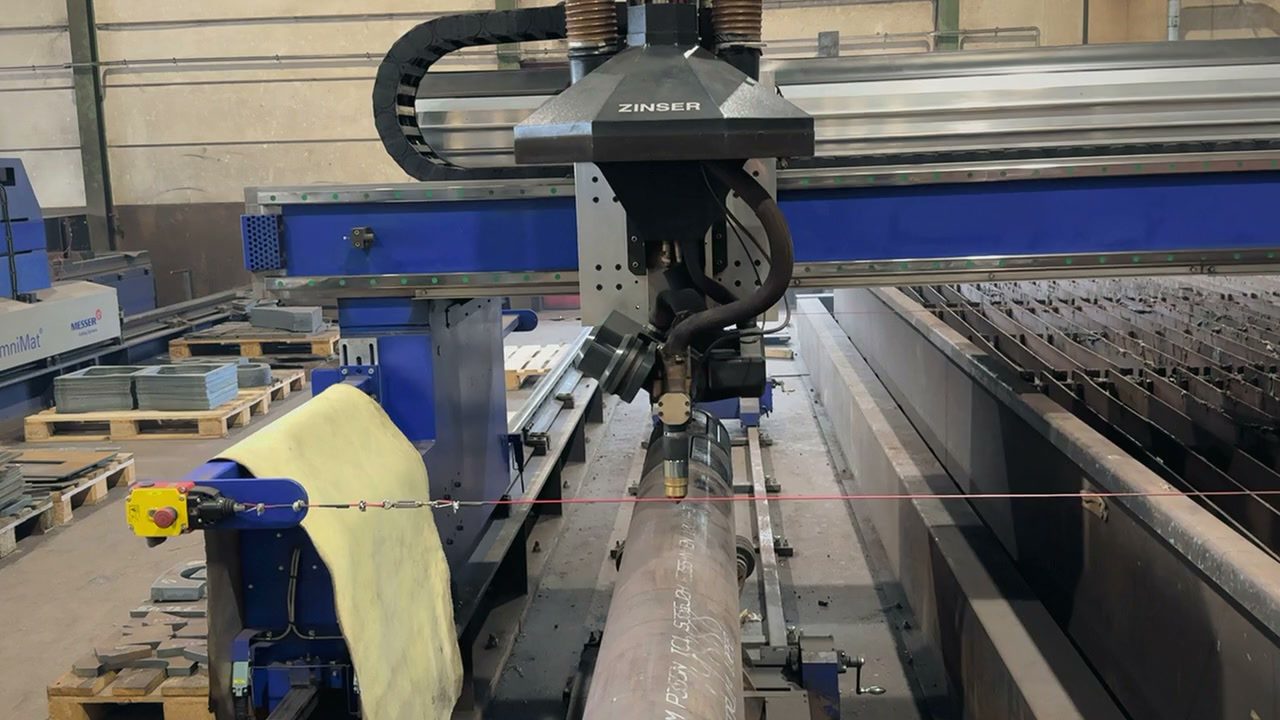
CNC-controlled 3-axis plasma system for tubes and hollow sections — 3D cut-outs, cope cuts and mitre cuts in a single operation, with no intermediate steps. Where tube lasers reach their limits.

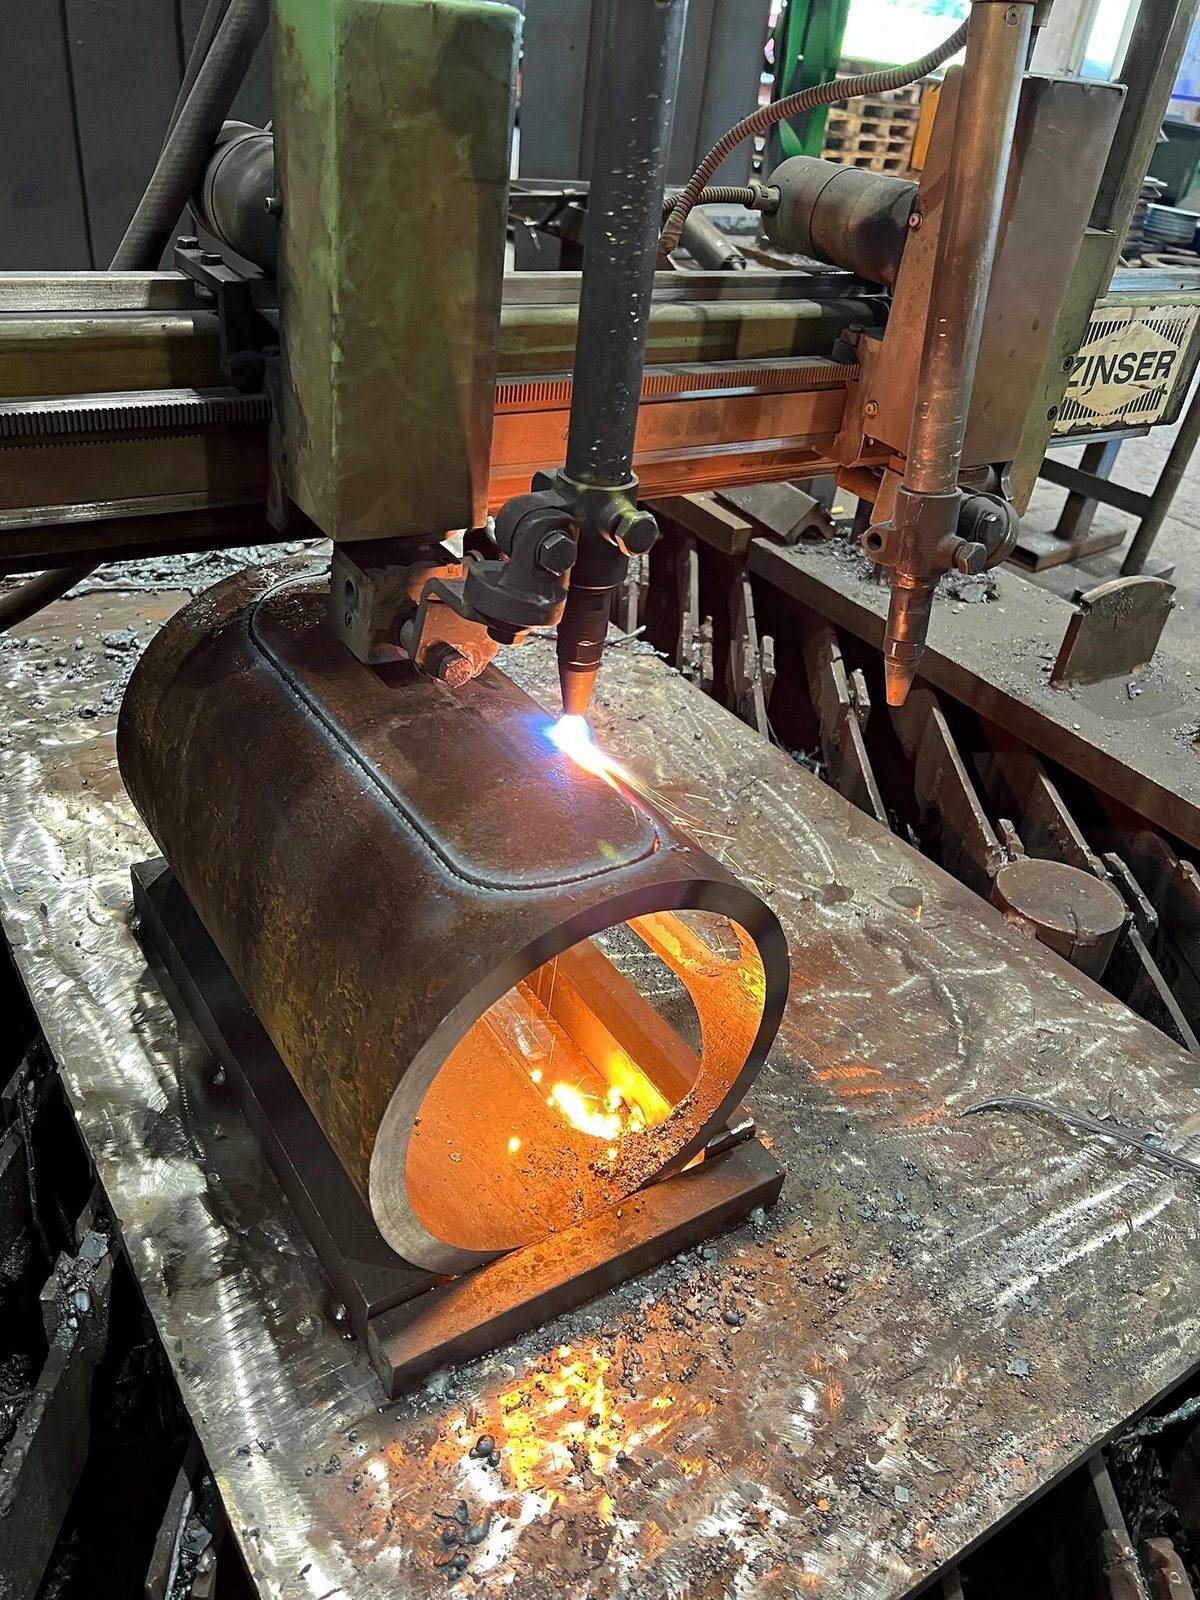
CNC copy flame-cutting machine (Zinser) for thick-walled tubes, profiles and hollow girders in solid steel and high-strength materials — where no tube laser and no plasma can cope any longer.
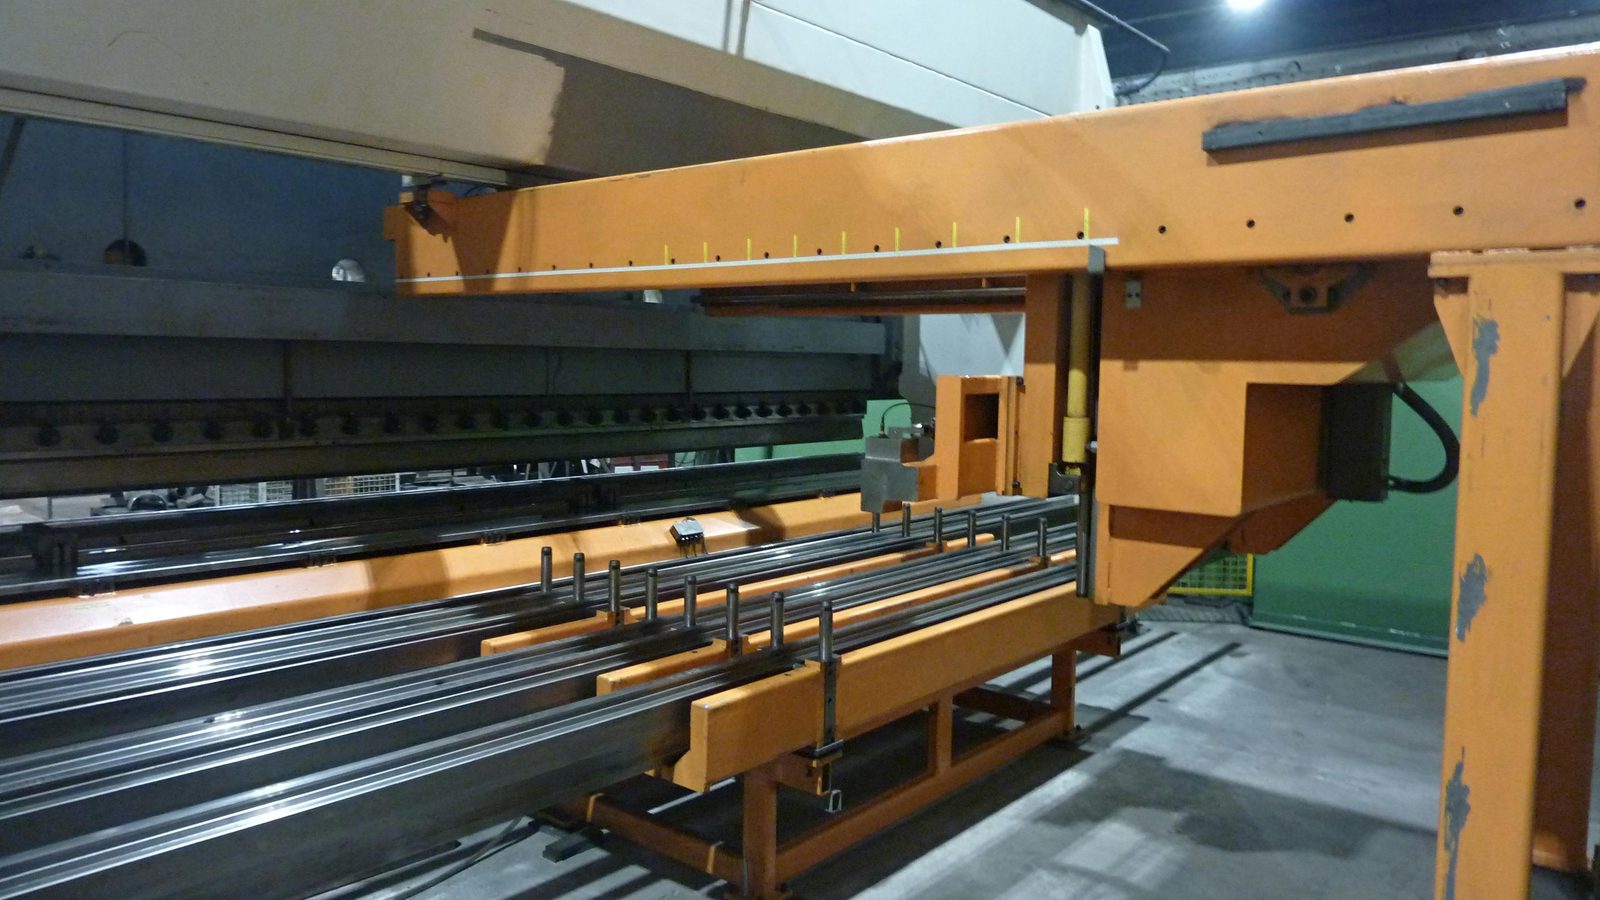
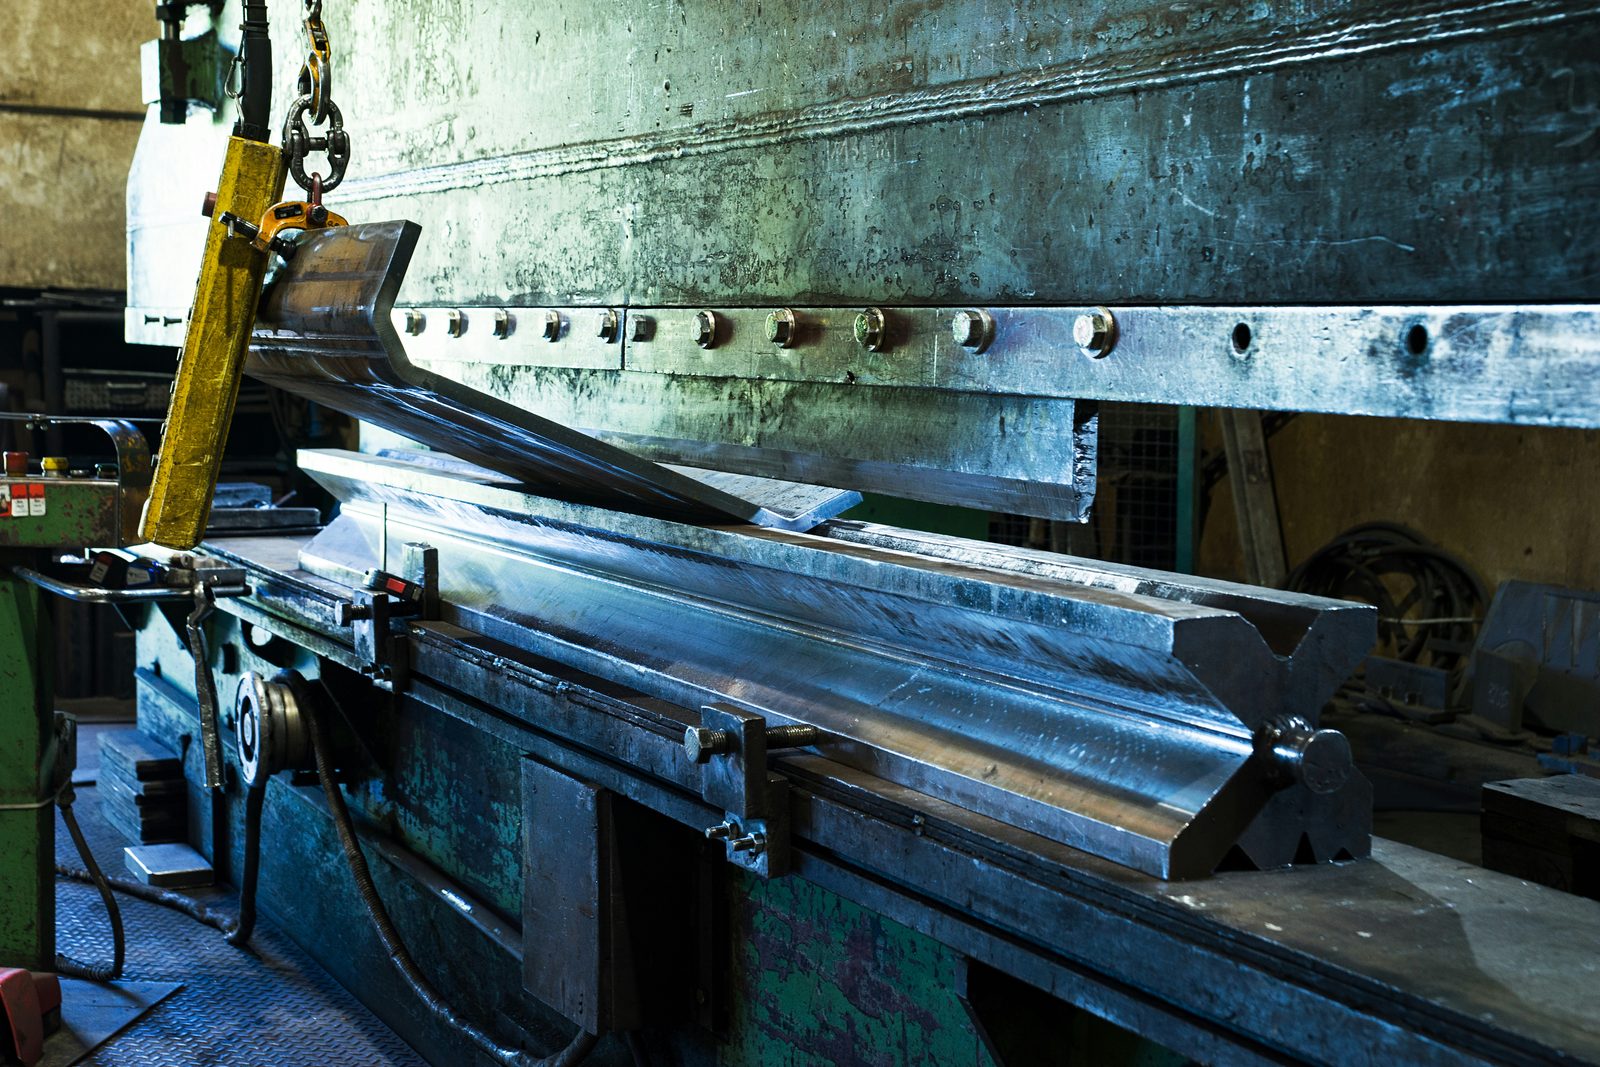
Flat plate becomes shape: die bending on press brakes up to 1,000 t and heavy plate rolling for cylinders, cones and special shapes.
1,000 t press force · Ø up to 8,000 mm · up to 120 mm plate thickness

Die bending of large plates on press brakes up to 1,000 t press force — dimensionally accurate and reproducible for every material.

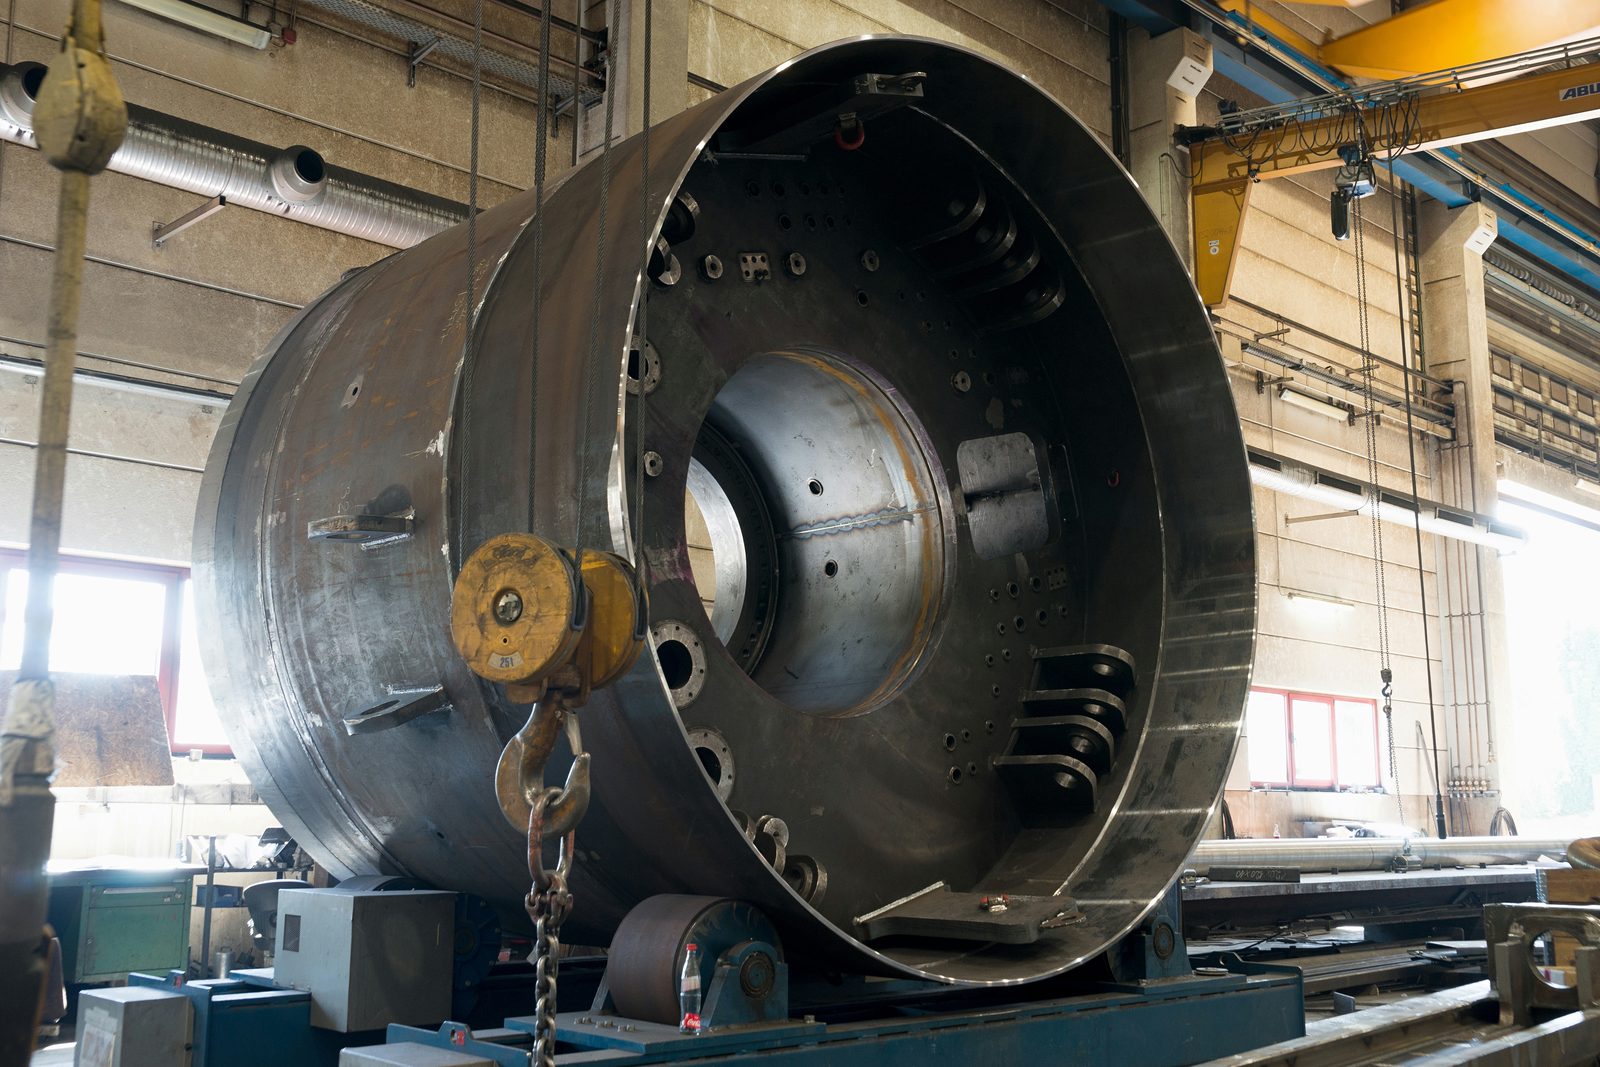
Heavy plate rolling and rounding for cylinders, cones and special shapes — steel, Hardox and stainless steel up to extreme diameters.
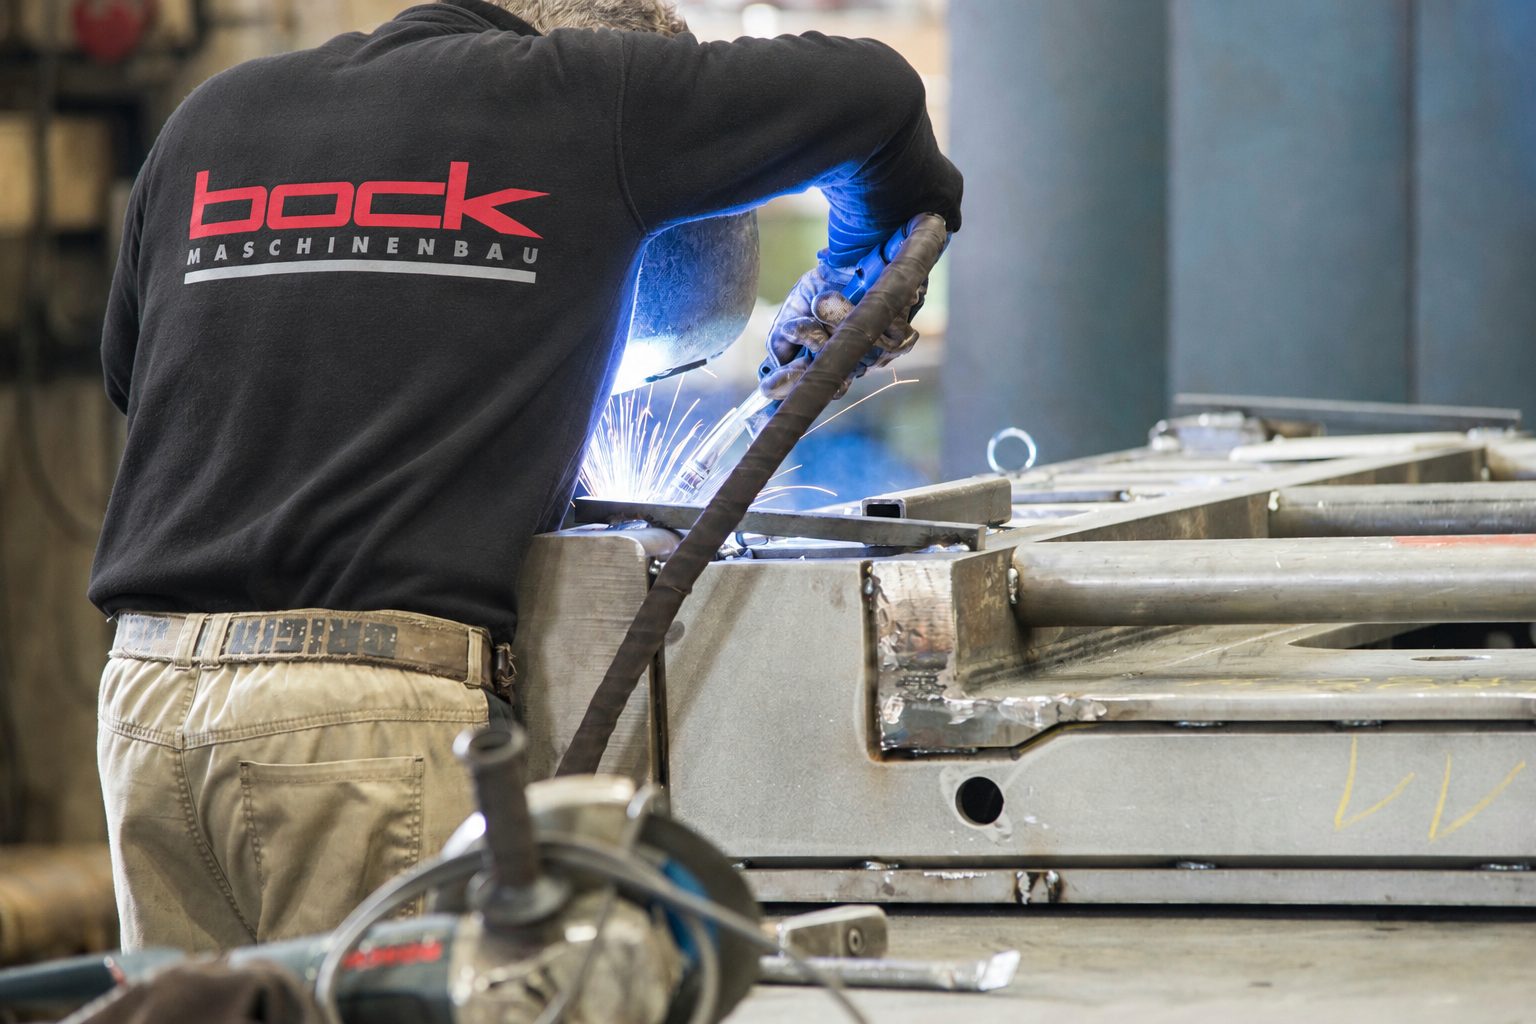
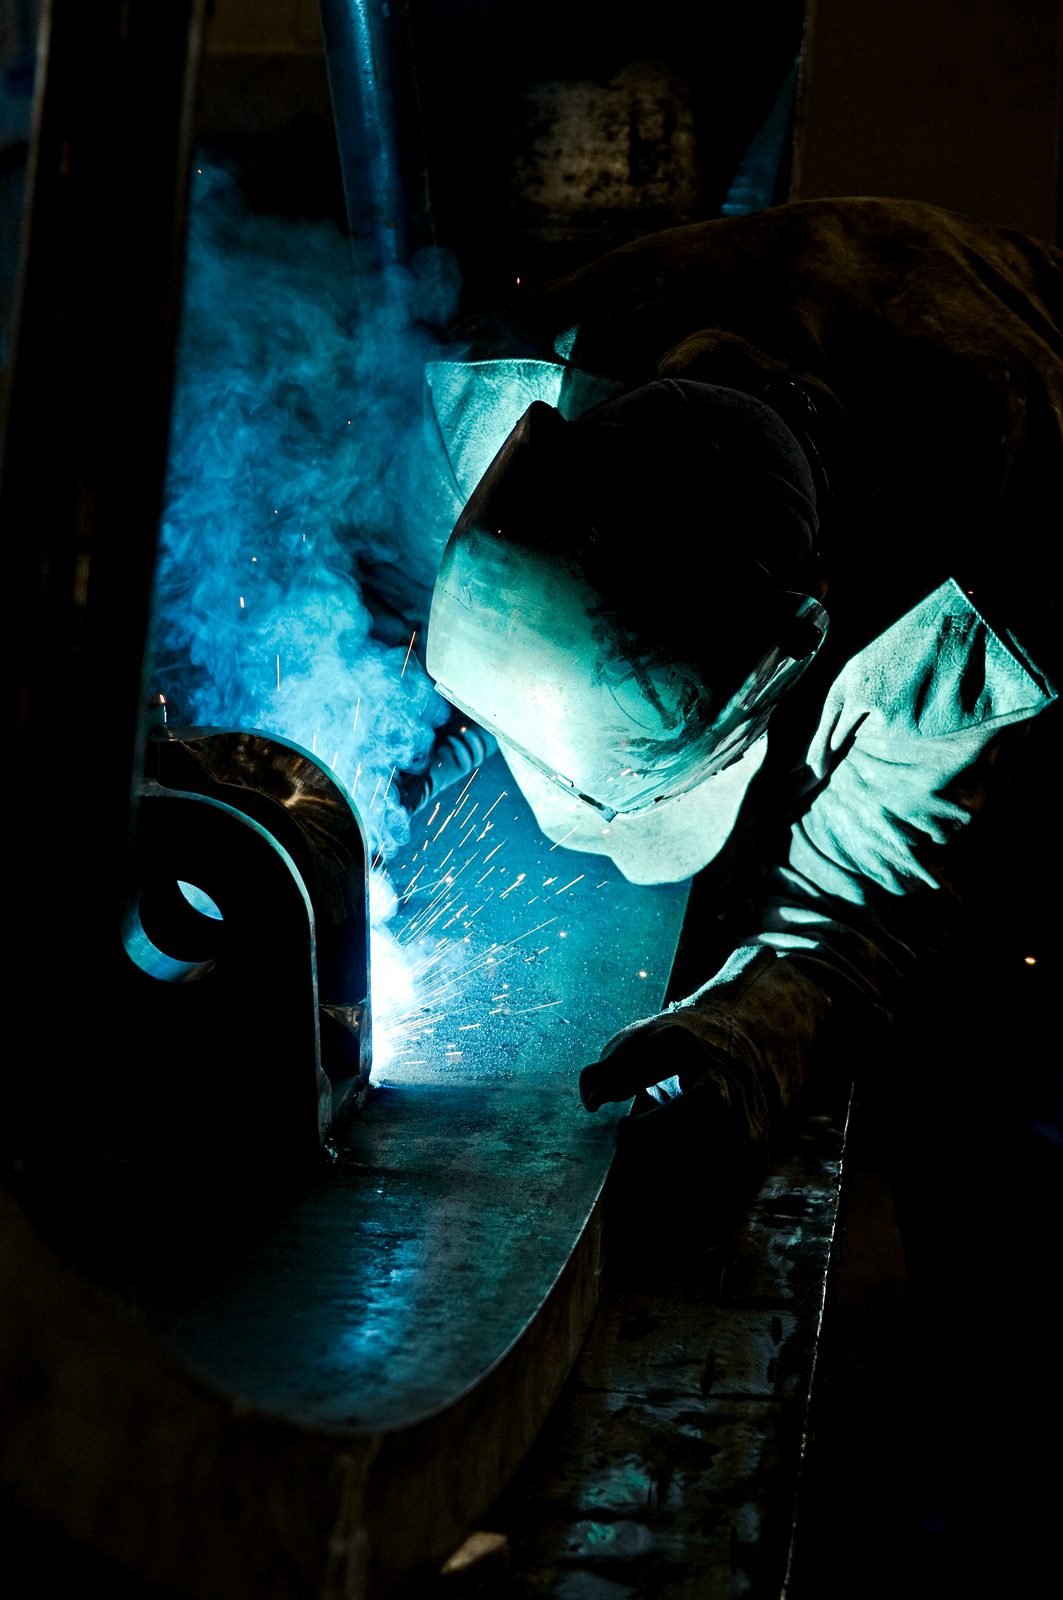
DIN EN 1090-2 EXC3 certified. MAG, TIG and submerged-arc for components up to 50 t — from the multi-part welded assembly to the large-format heavy component.
EXC3 · EN ISO 3834-2 · up to 50 t

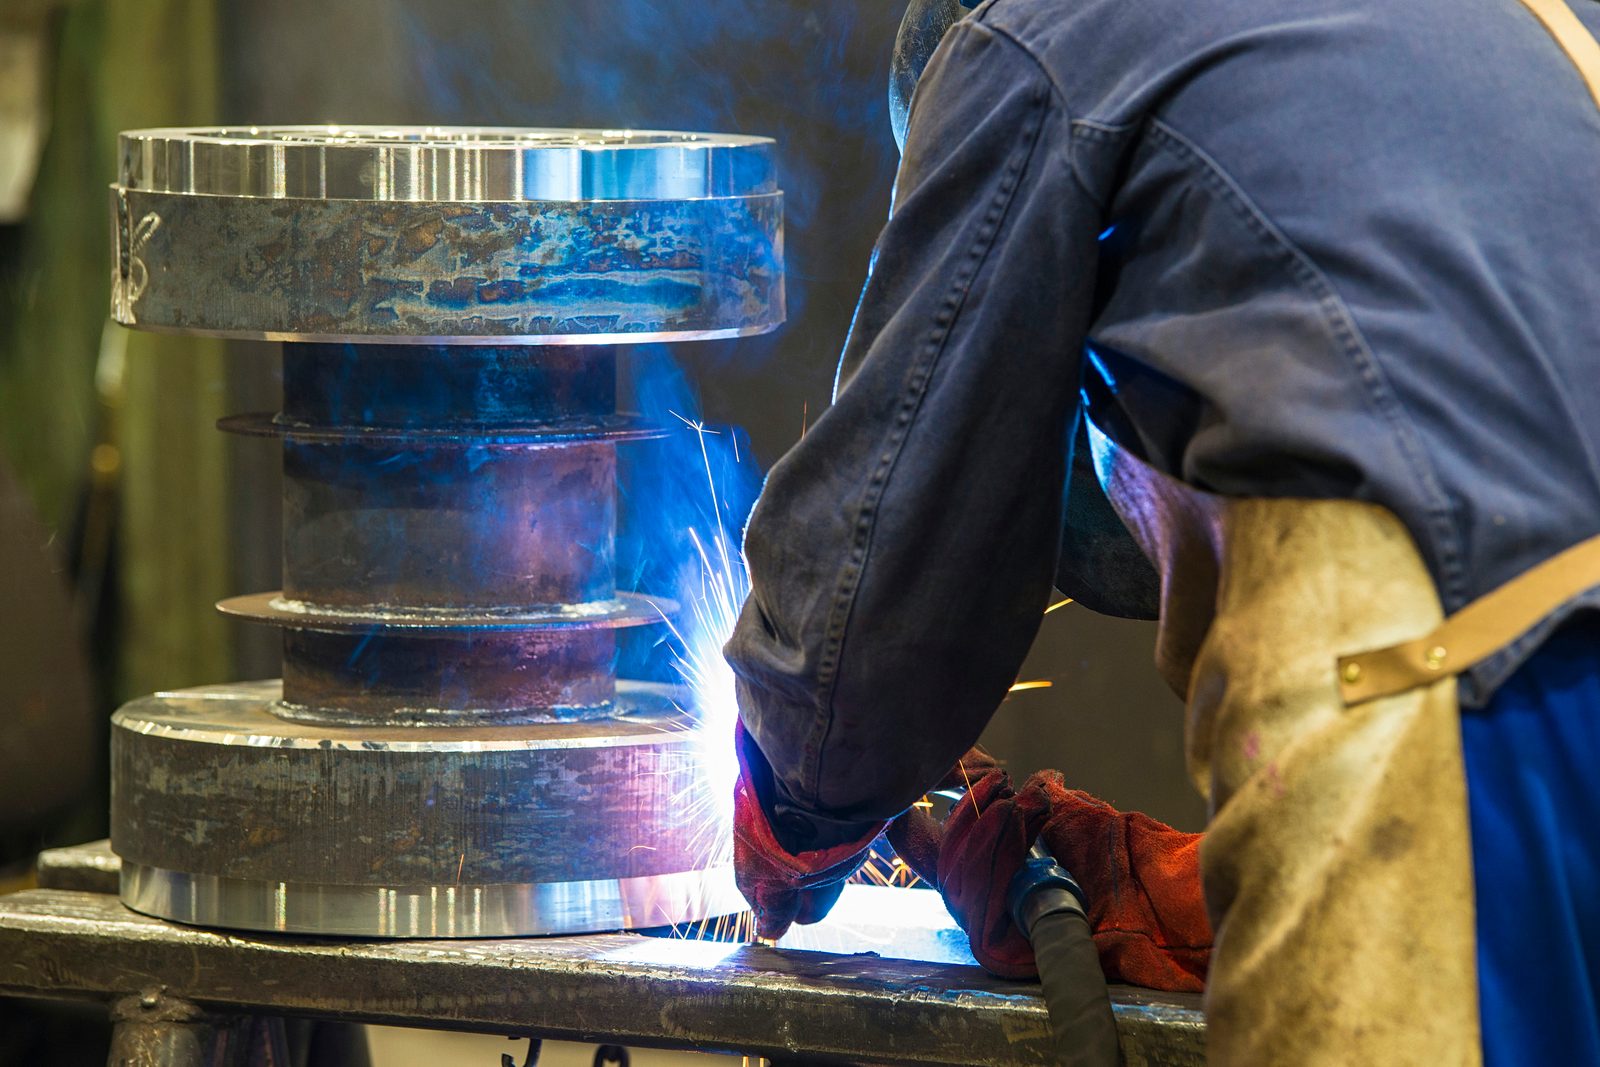
Contract welding to DIN EN 1090-2 EXC3 — MAG, TIG, for steel, Hardox, stainless steel and fine-grain steel up to S1100, multi-part assemblies with many joints.

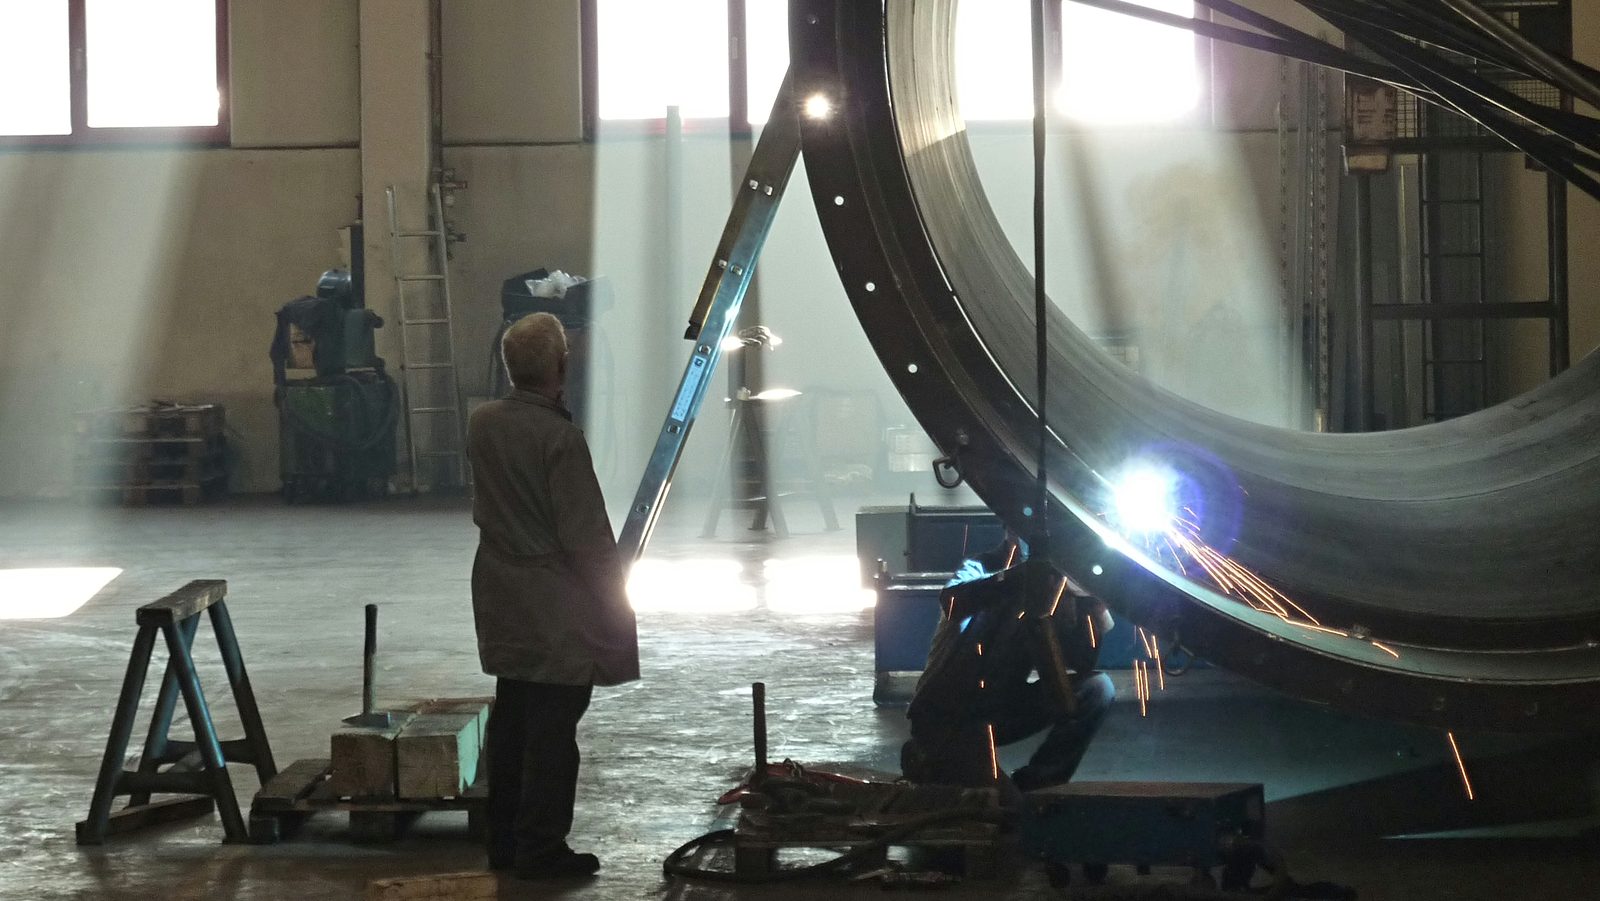
Automated submerged-arc welding with ESAB masts up to 7 m reach and 1,250 A — deep, high-strength welds on heavy parts.

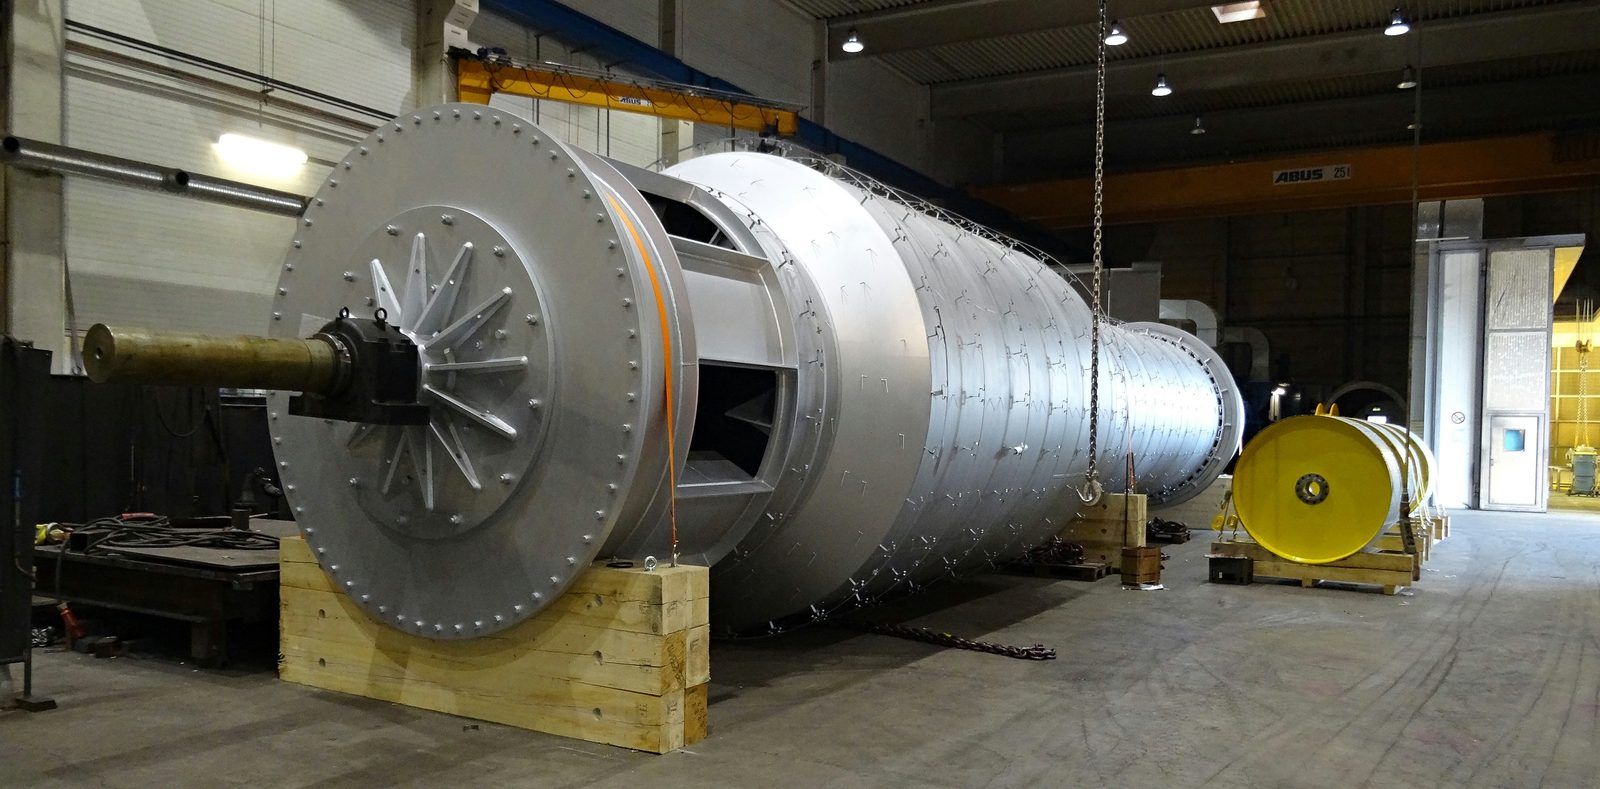
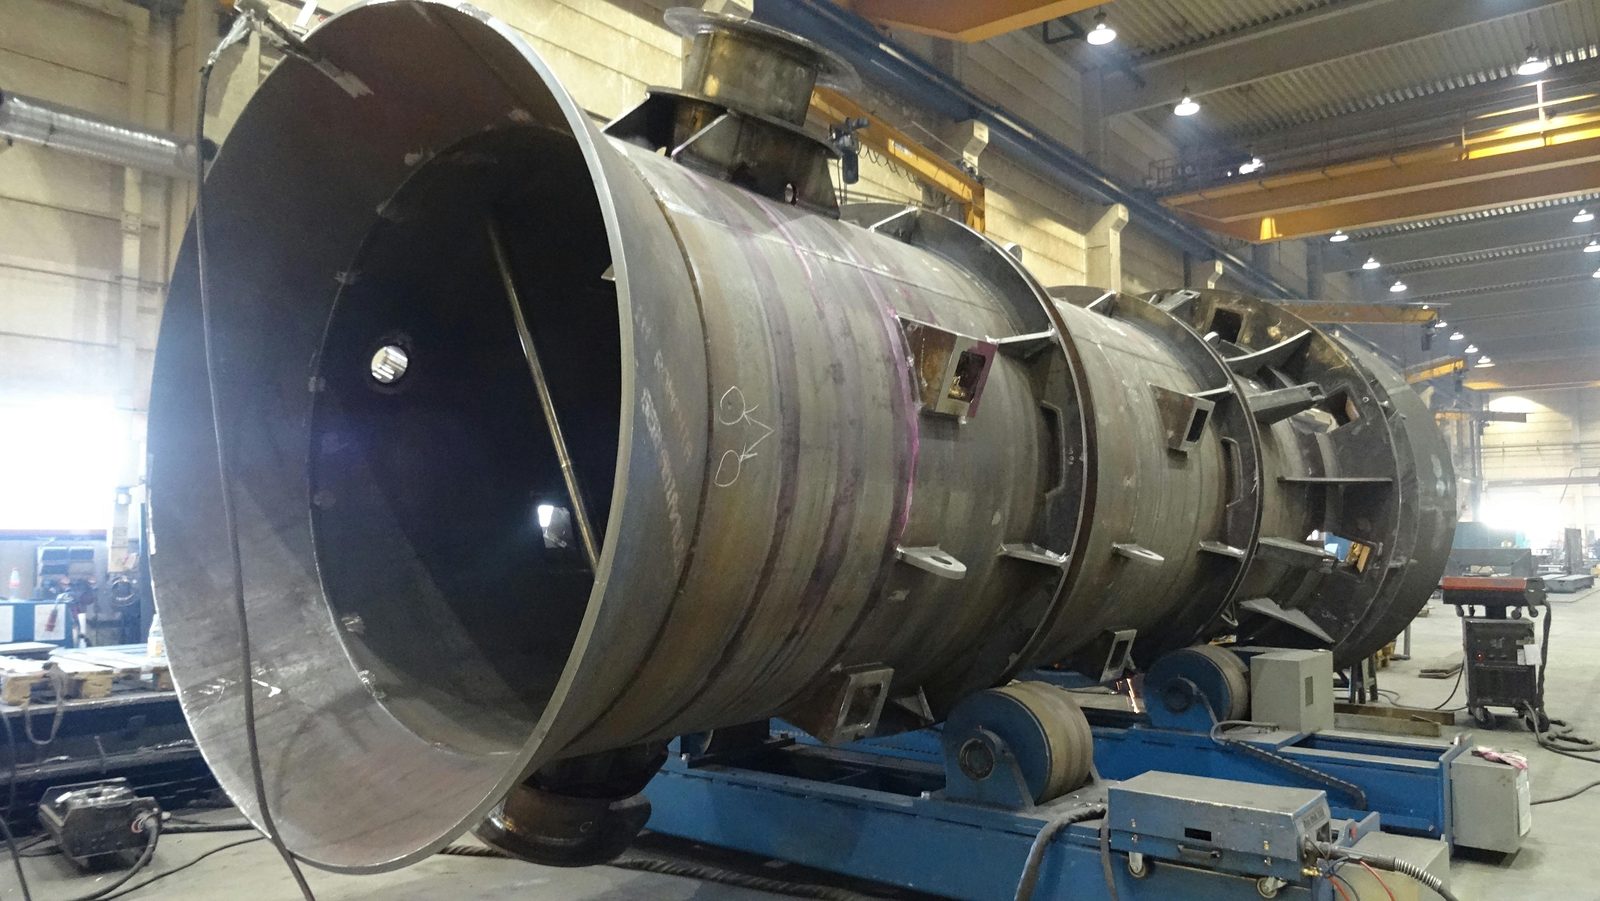
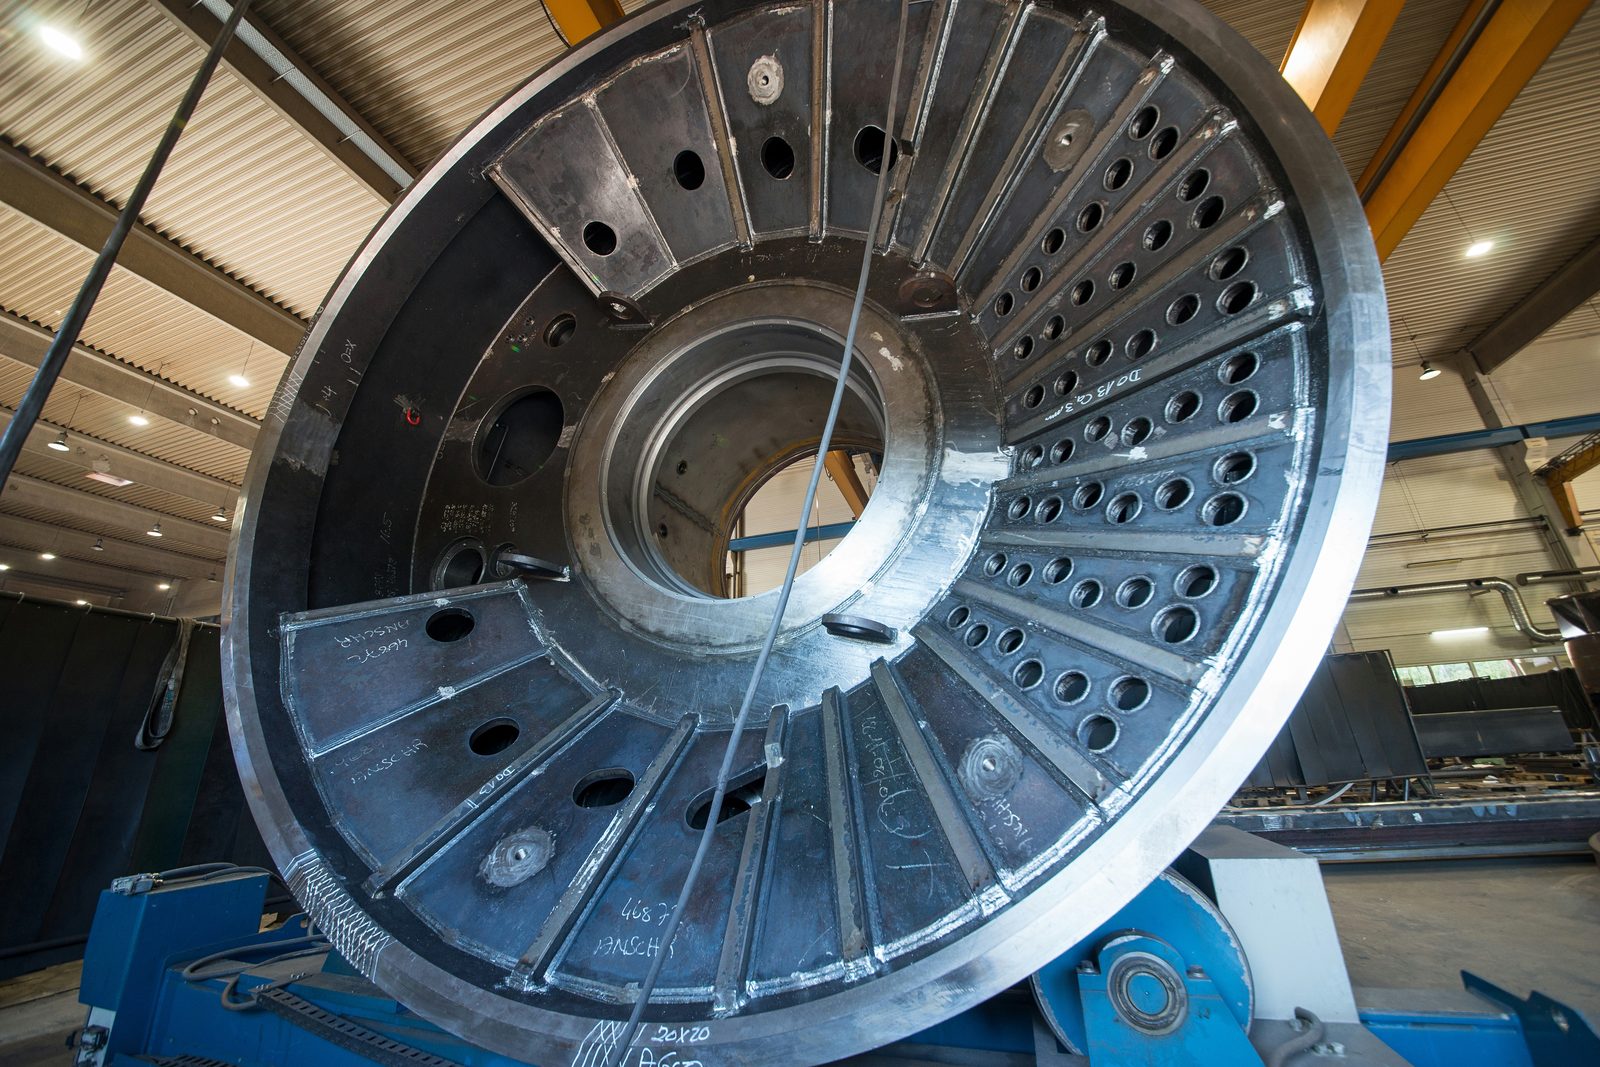
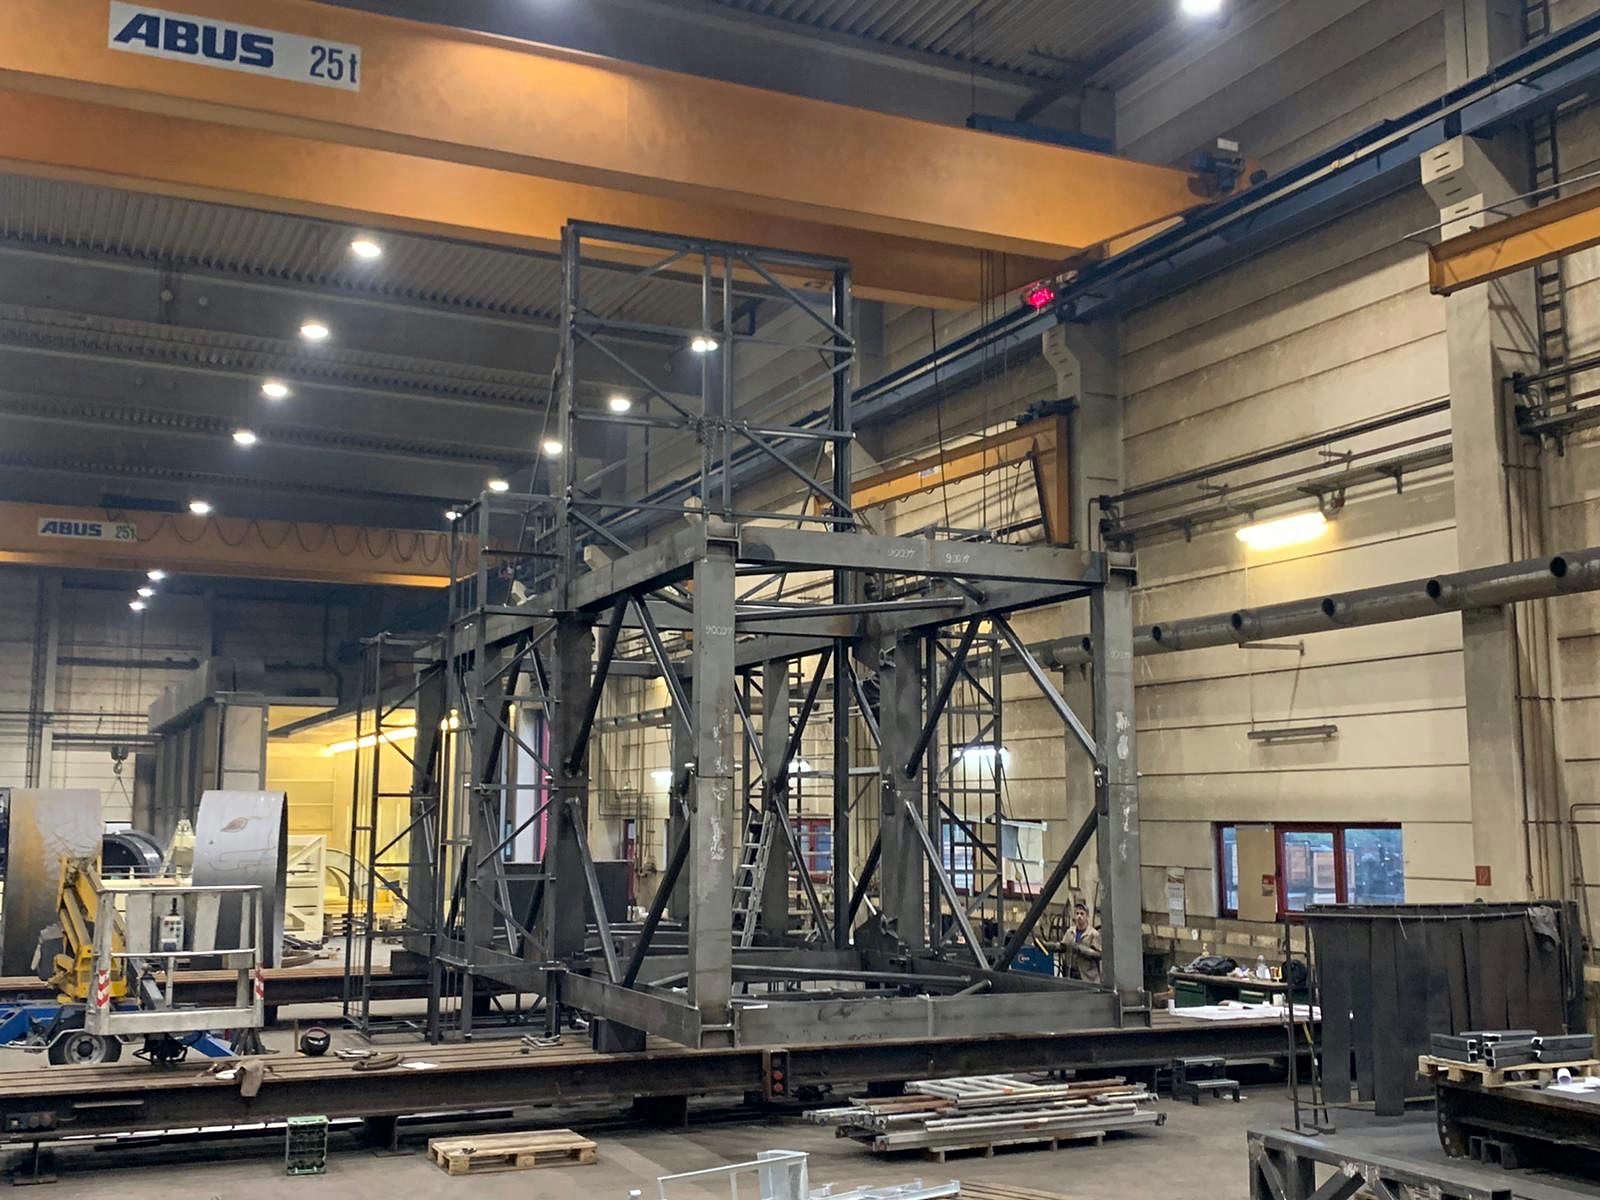
Large-format individual components and structures up to 50 t on the 2×25-t crane system — DIN EN 1090-2 EXC3, steel, Hardox and fine-grain steel up to S1100.
Welding brings heat — and heat brings residual stresses and distortion. We remove both from the components before machining: vibration stress relief releases stresses without a furnace, flame straightening corrects distortion. This keeps the part dimensionally stable for the long term.
Vibration stress relief (VSR) · flame straightening · without stress-relief annealing

VSR treatment to reduce residual stresses — fast, economical, without heat. Ideal for welded structures as an alternative to stress-relief annealing.

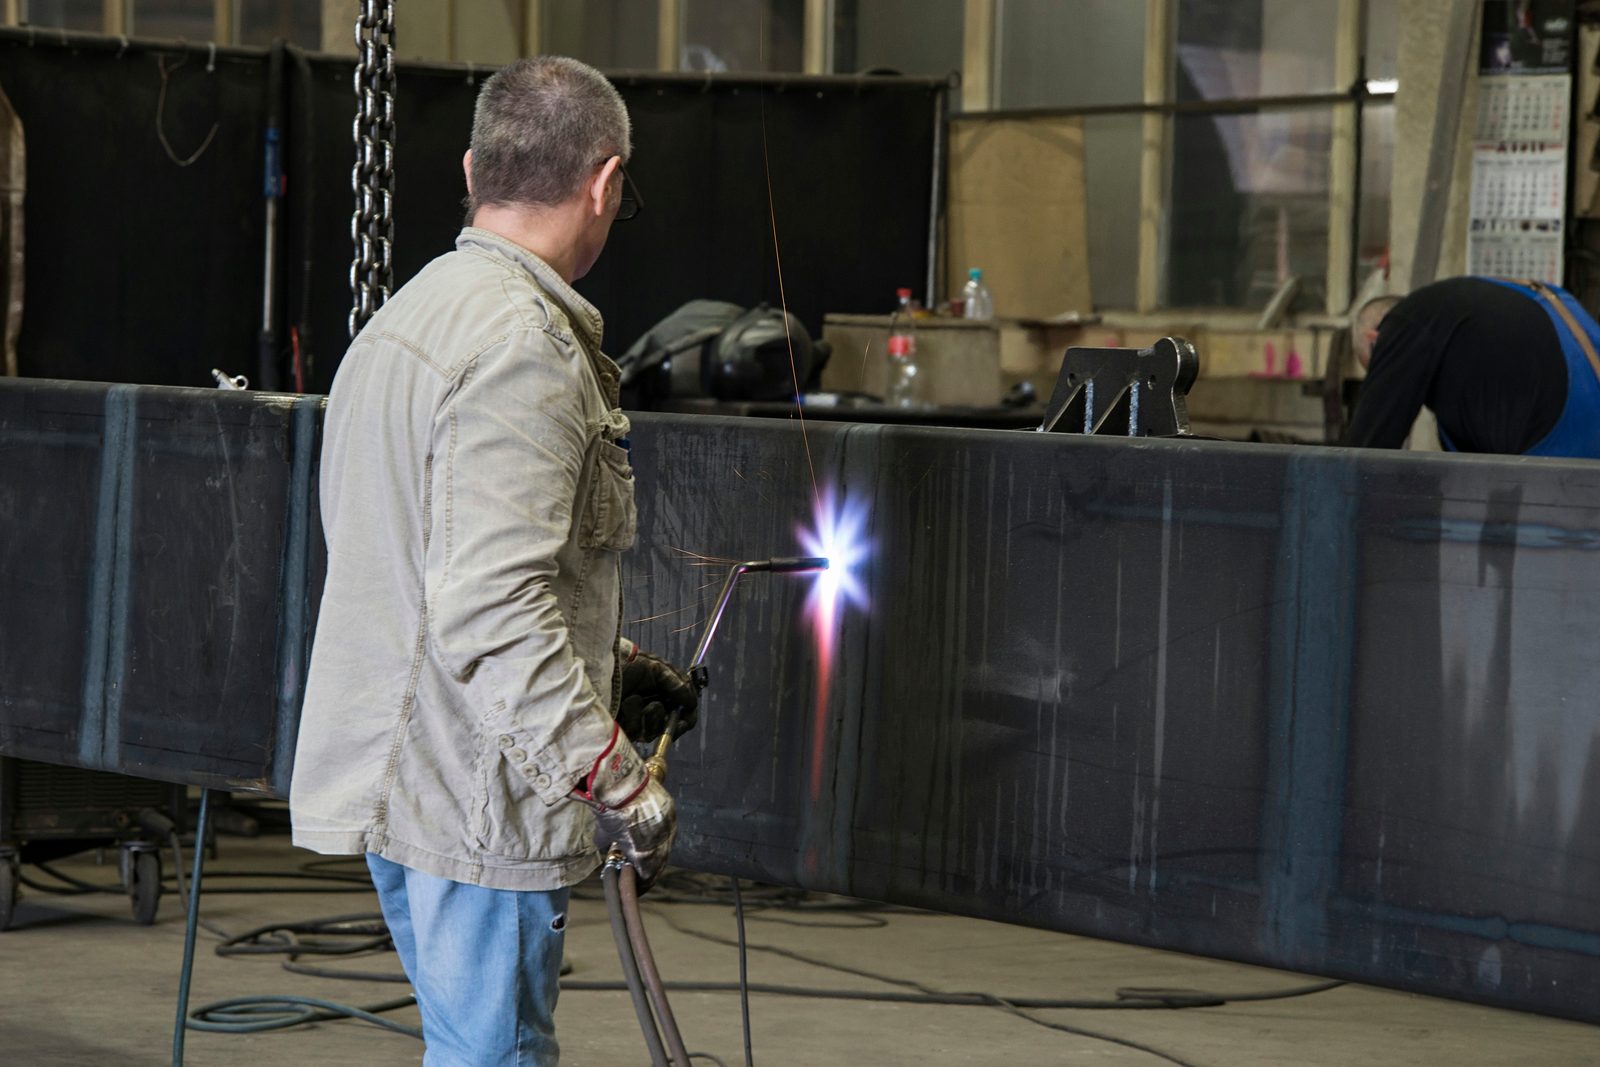
Thermal straightening of welded structures and large components — targeted heating corrects welding distortion and secures dimensional accuracy, even on heavy parts up to 50 t.

Between cutting and assembly, no part ever leaves our plant.
Large-part CNC machining for heavy parts: vertical turning up to Ø 4,800 mm, gantry milling up to 26 metres of travel and three CNC horizontal boring mills with rotary table — dimensionally accurate and reproducible.
Ø up to 4,800 mm · gantry milling 26 m · 3 × boring mill · up to 50 t

Contract turning of heavy parts on vertical lathes — large flanges, slewing rings and rotationally symmetric components up to large diameters.

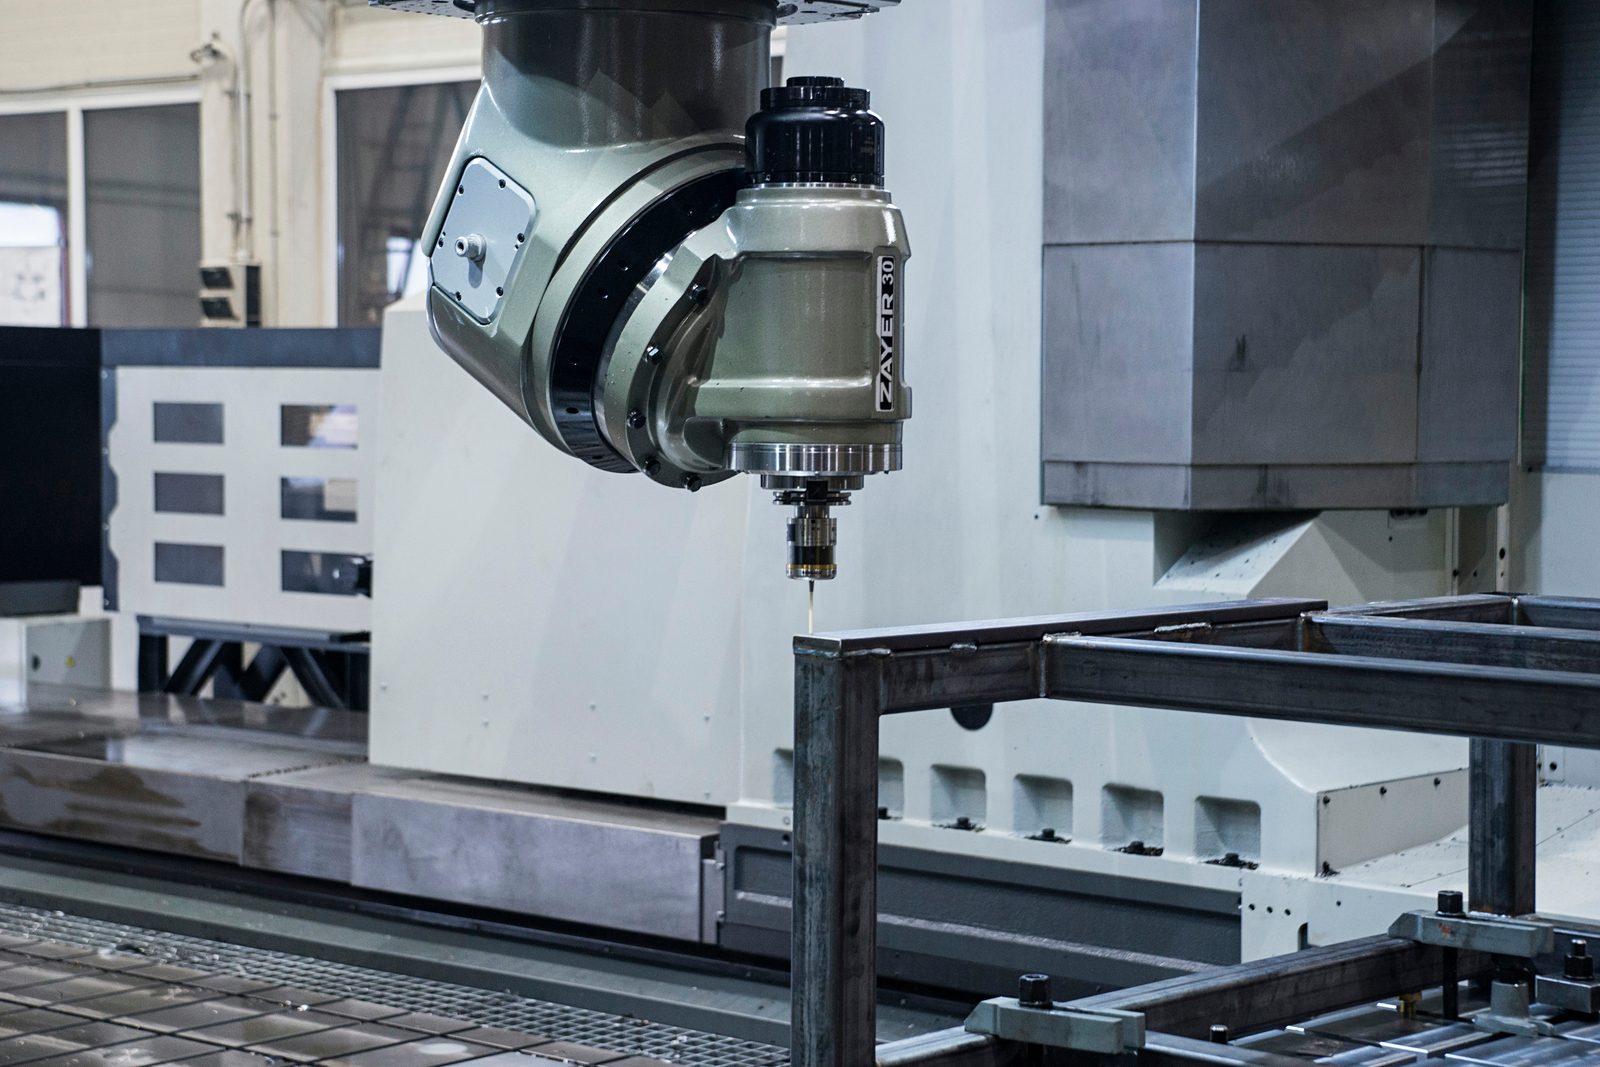
Two gantry milling machines with a 30° swivel milling head and a portal supported on both sides — maximum rigidity for long, large-format components.

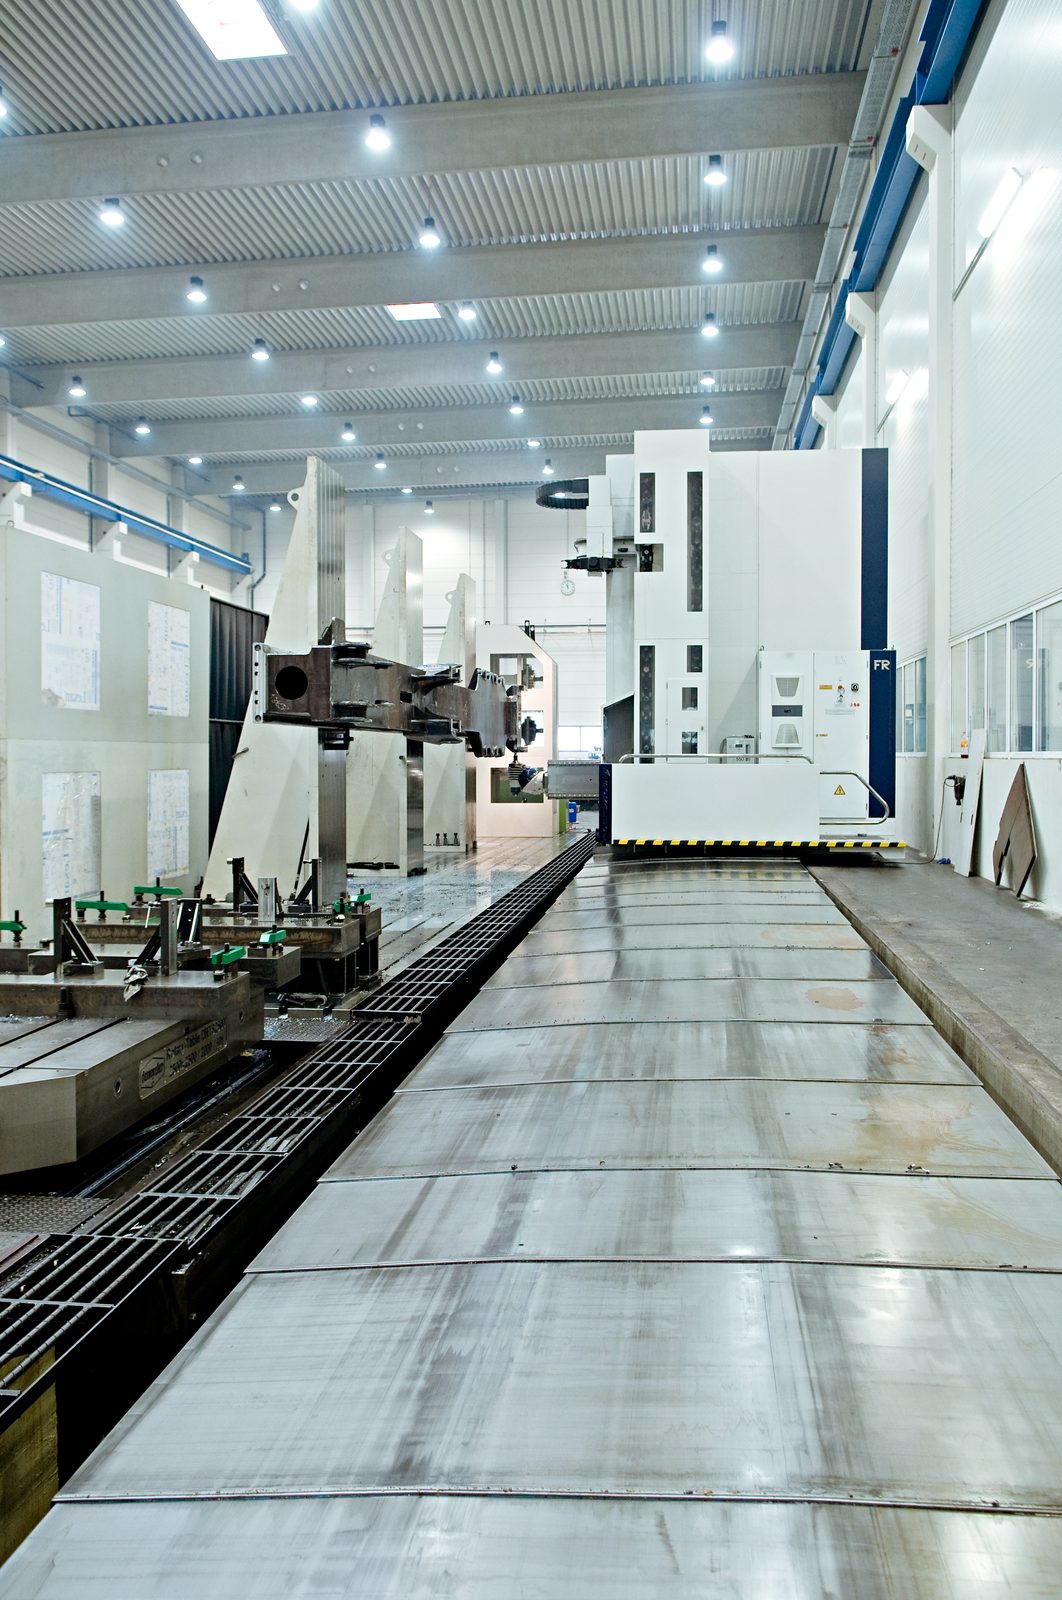
Soraluce FR 20,000 with a swivelling milling head and rotary table — a work area open at the top for bulky, tall heavy parts: milling, boring, line boring.

Three TOS-Varnsdorf WHN 13 CNC with rotary table — precise boring, line boring and milling on heavy components, produced in parallel and on schedule.

The overview: gantry milling, travelling-column milling, horizontal boring mills and vertical turning for heavy parts up to 50 t — all processes under one roof.

Radial drilling, countersinking and reaming up to Ø 90 mm — thread cutting up to M60 on large parts in steel, stainless steel and Hardox.
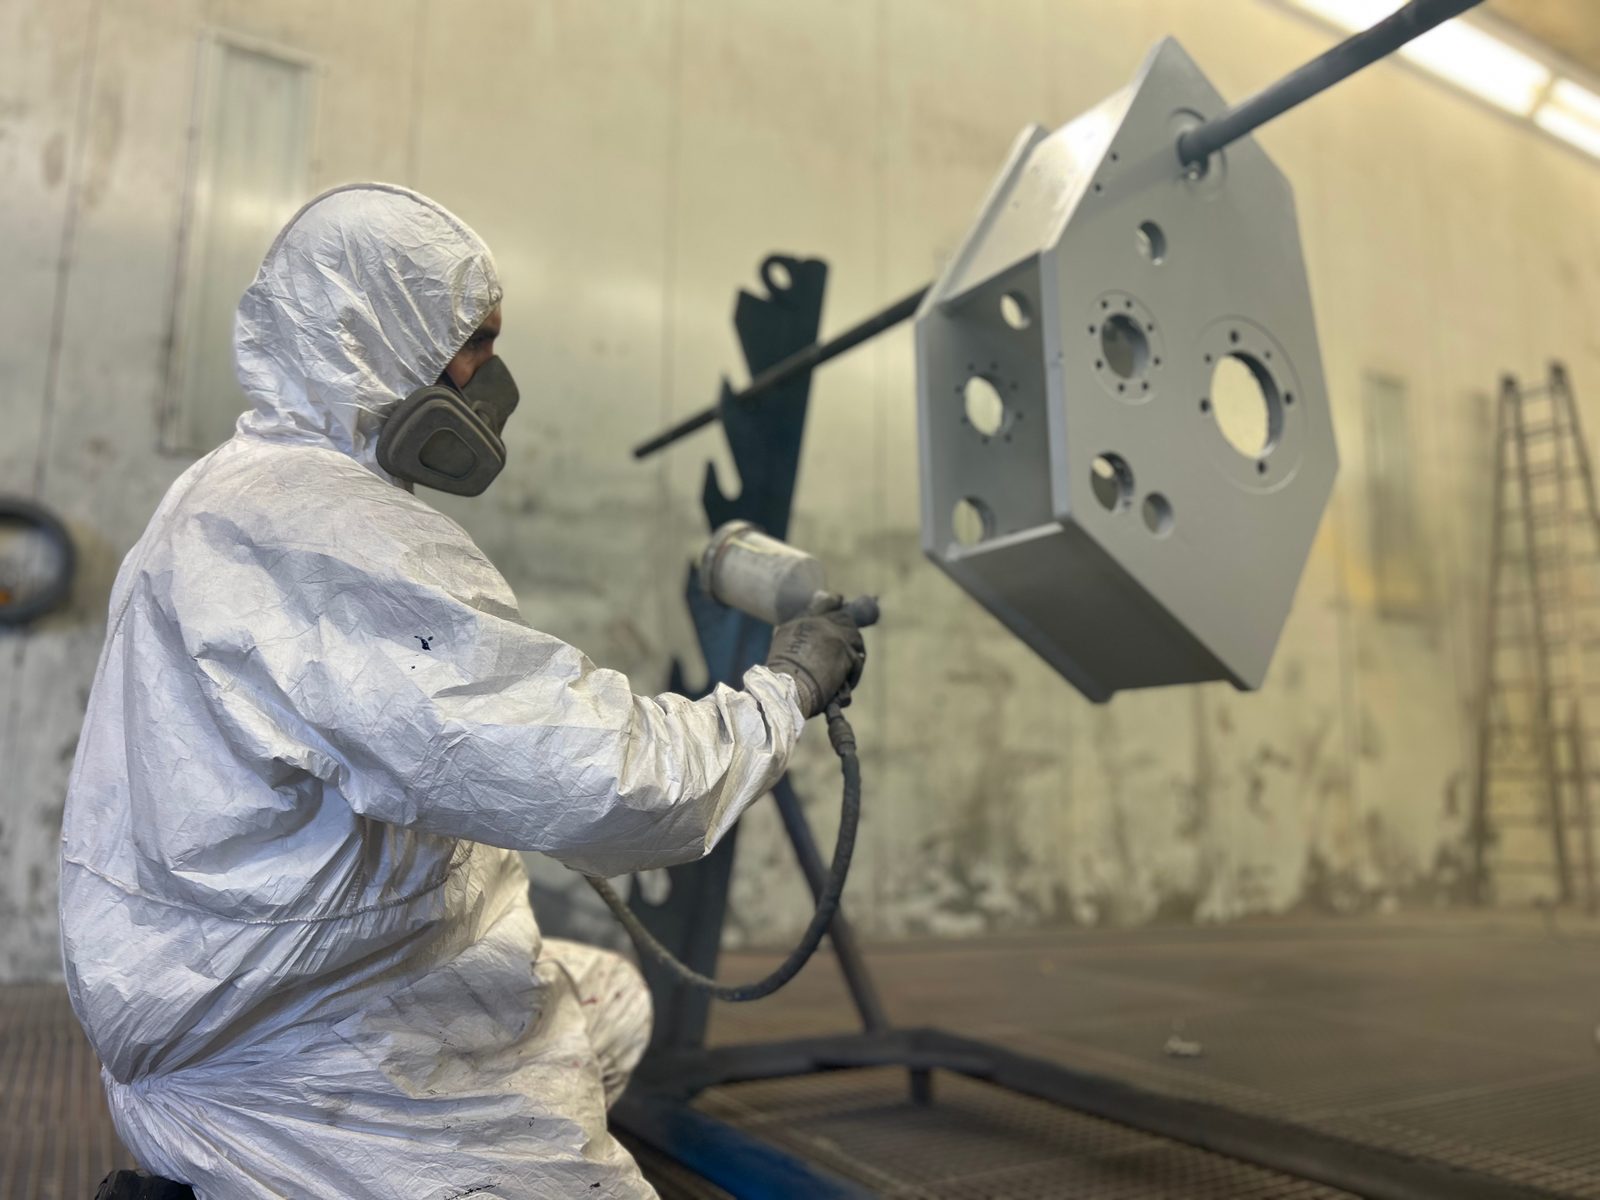
We add the final touch in-house: blasting up to Sa 2,5 and industrial painting to EN ISO 12944 in the 25-metre large-volume booth — corrosion protection from a single source.
Sa 2,5 · EN ISO 12944 · booth 25 × 7 × 6 m

Sandblasting up to Sa 2,5 in our 25 × 7 × 6 m large-volume booth — optimal adhesion conditions before industrial painting to EN ISO 12944.

Industrial painting to EN ISO 12944 in a 25 × 7 × 6 m large-volume booth — steel, Hardox, stainless steel up to 50 t, sandblasting from a single source.
Single parts become the finished assembly: locksmithing and assembly work, jig building and final assembly — certified joining quality meets craftsmanship precision, all under one roof.
Assembly of subassemblies · locksmithing · jig building

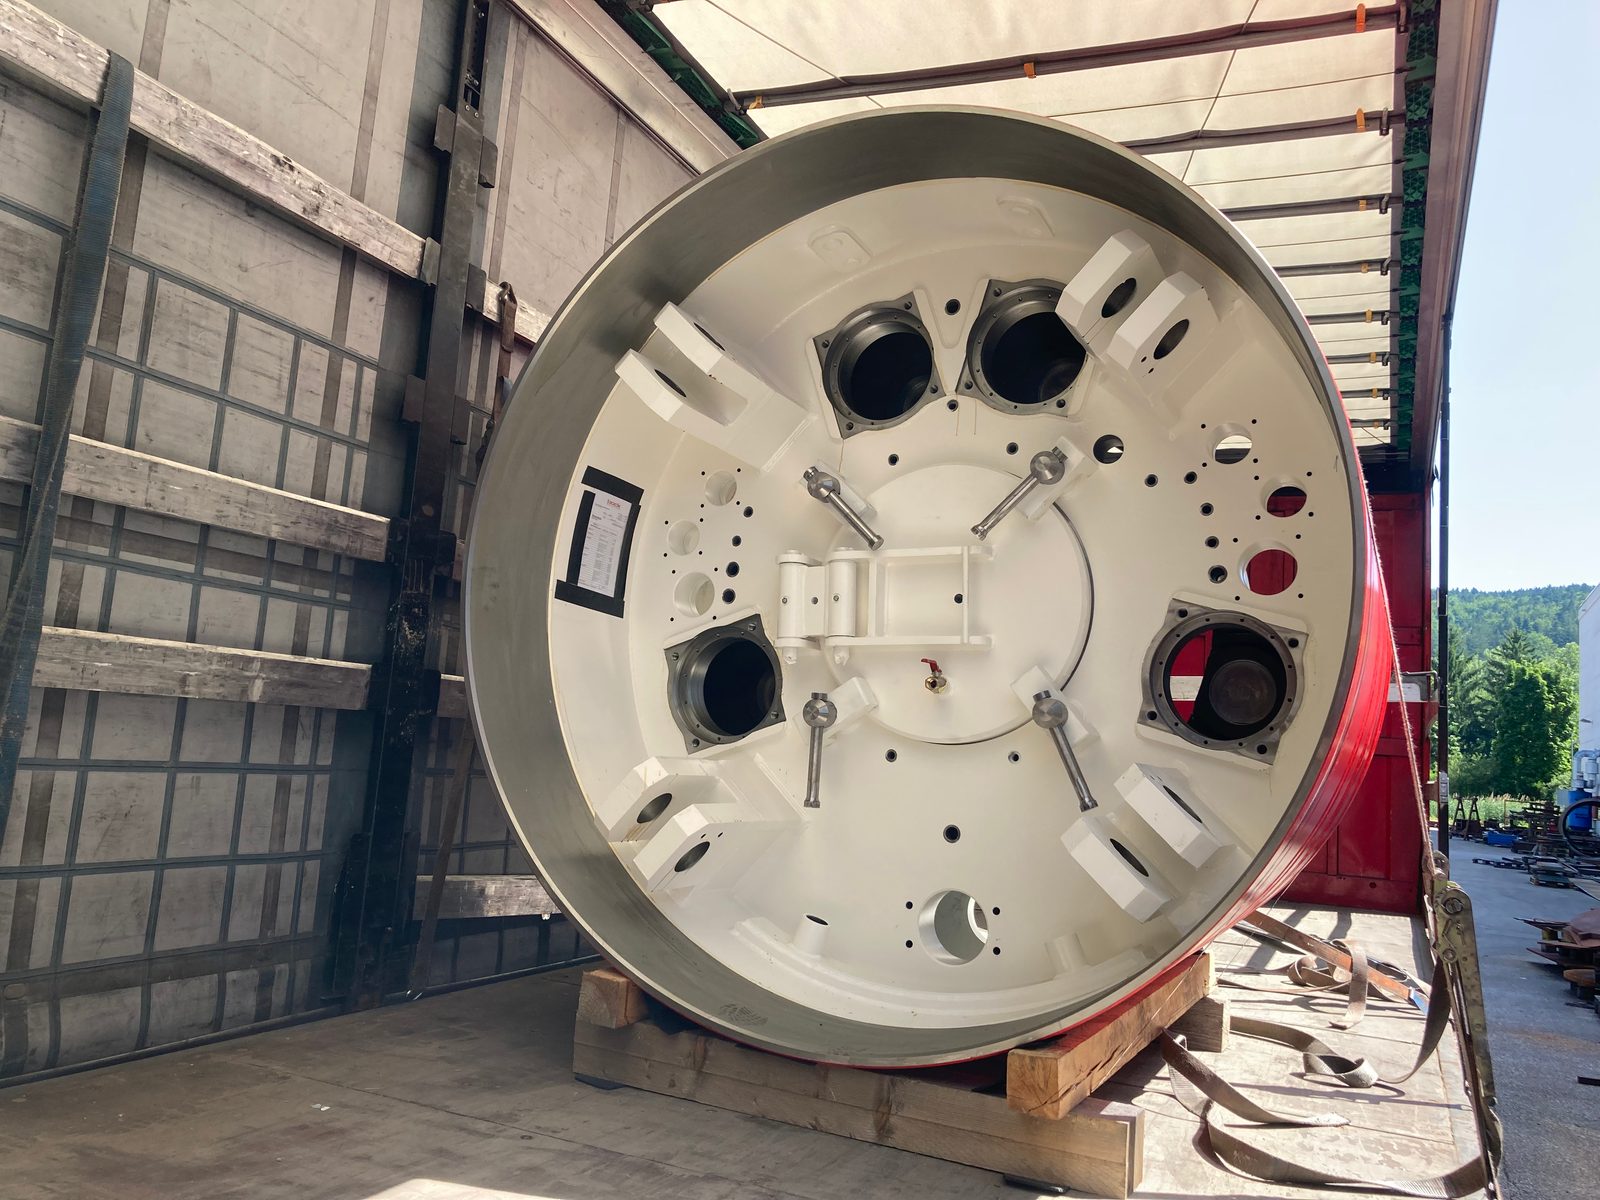
Assembly of welded and machined components into complete assemblies — heavy-duty structures to DIN EN 1090-2 EXC3, up to 50 t.

Professional locksmithing, fitting and assembly services for steel assemblies and single parts — craftsmanship precision meets industrial manufacturing.
Quality runs through the entire production — and at the end there is documented proof: certified welding supervision, non-destructive testing of the welds, geometric measurement and a measurement & inspection report. No component subject to acceptance leaves the plant without the required documentation.
DIN EN ISO 9001 · EXC3 · EN ISO 3834-2 · NDT to DIN EN ISO 9712

We inspect welds and components with the appropriate NDT methods and document the result on a project basis according to drawing, standard and customer specification — without damaging the component.

Authorised by GSI SLV München, we transfer the material marking to EN 10204 from the 3.1 inspection certificate onto flame-cut and cut parts — cleanly documented down to the individual component.
DIN EN 1090-2 EXC3 & EN ISO 3834-2 — verified joining quality, supervised by IWE/EWE welding supervision.
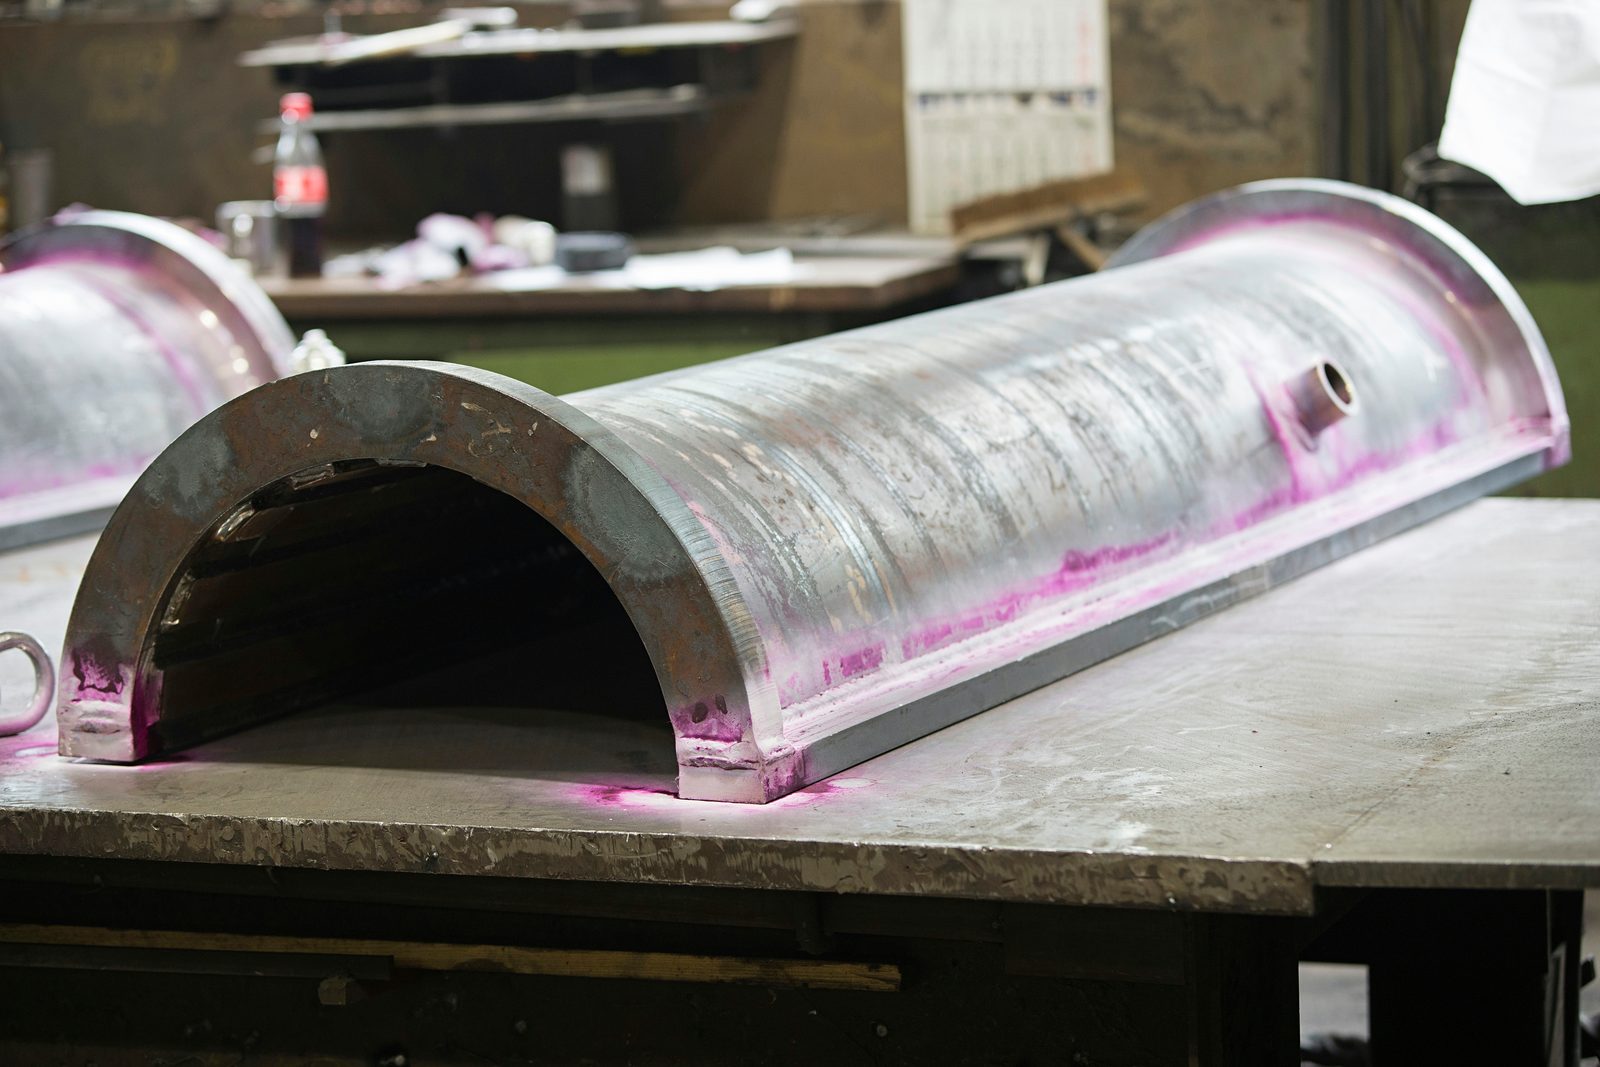
VT, PT and MT in-house (Level 2, DIN EN ISO 9712), UT via our cooperation partner — weld quality proven without damaging the component.
Re-stamping to EN 10204 — authorised by GSI SLV München: batch and sample from the 3.1 inspection certificate onto every flame-cut part.
Geometric measurement of the components — also before CNC machining — plus a documented inspection report of the dimensions and tolerances to DIN EN ISO 9001.
All eight steps interlock — and do not end at the single part: special container construction for offshore applications and special machinery to customer specification, manufacturing and final assembly entirely in-house, without a single external supplier.
Single piece to small series · Manufacturing + assembly · Entirely in-house

Manufacture of special containers for offshore and industrial applications — built to customer specification, certified to DIN EN 1090-2 EXC3.

Complete manufacturing for special machinery and plant engineering — crane construction, vehicle construction, water treatment and special foundation engineering from a single source, single piece to small series.
Worn, cracked or damaged steel assemblies do not have to be replaced: weld repair, build-up and hardfacing welding, machining refurbishment, blasting and painting interlock within the same operation — including makes from other manufacturers.
Weld repair EXC3 · build-up & hardfacing welding · up to 50 t · third-party makes too

Weld cracks and fractures, build up worn surfaces by build-up and hardfacing welding and machine them back to size — heavy assemblies up to 50 t.

Disassemble assemblies, blast them, renew wear liners, paint and reassemble — handed over like new, more economical than a new build.
DIN EN 1090-2 & EN ISO 3834-2 — verified weld quality for load-bearing structures.
A 2 × 25-t crane and machines for component dimensions where others have to pass.
From cutting to painting without an external supplier — one responsibility, one point of contact.
Manufacturing centrally in Baden-Württemberg — short distances, plannable deadlines, personal contact.
Send us your drawing or a short enquiry. You receive a non-binding quote — and a point of contact who knows your parts.